

Principle and Working Scene Characteristics of Vacuum Suction Type Powder Conveying Lines
Understanding the vacuum suction type powder conveying line is crucial for industries dealing with bulk solid materials. This technology offers an efficient and safe method for transporting powders over varying distances and in diverse operational environments. The following sections delve into the fundamental principles of this system and highlight key characteristics that define its application scenarios.
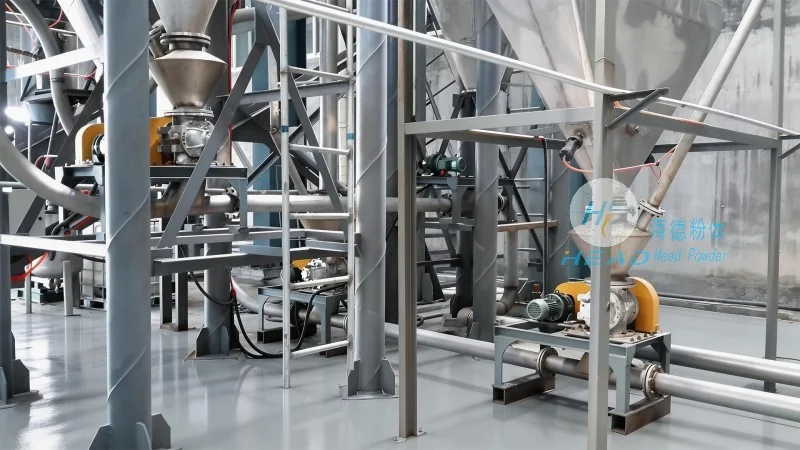
Principle of Vacuum Suction Type Powder Conveying Lines
The core mechanism of a vacuum suction type powder conveying line revolves around the creation of a negative pressure environment within the conveying pipeline. This is achieved by using a vacuum pump, which draws air from the system, thereby reducing pressure inside the pipeline. As a result, the atmospheric pressure outside the pipeline exerts a force on the powder particles, causing them to be drawn into the pipeline and transported to the discharge point. The process typically involves several key components: a vacuum pump, conveying pipes, a dust filter, and a control system. The vacuum pump generates the necessary suction force, while the pipes guide the powder flow. The dust filter ensures that any airborne particles are captured, maintaining air quality and preventing contamination. The control system manages the operation of the pump and other components, ensuring smooth and efficient operation.
Key Working Scene Characteristics
The vacuum suction type powder conveying line is particularly well-suited for a range of industrial applications due to its unique operational characteristics. One of the primary advantages is its ability to handle powders in a dust-free manner, which is critical in industries such as pharmaceuticals, food processing, and electronics manufacturing where product purity is paramount. The system operates by drawing powders into the pipeline without the need for mechanical contact, reducing the risk of contamination and ensuring product integrity. Additionally, this type of conveying system is highly effective for long-distance transportation, with some models capable of moving powders over distances of several hundred meters or more. This makes it ideal for facilities where raw materials are stored in one location and processed in another, eliminating the need for manual handling and reducing labor costs.
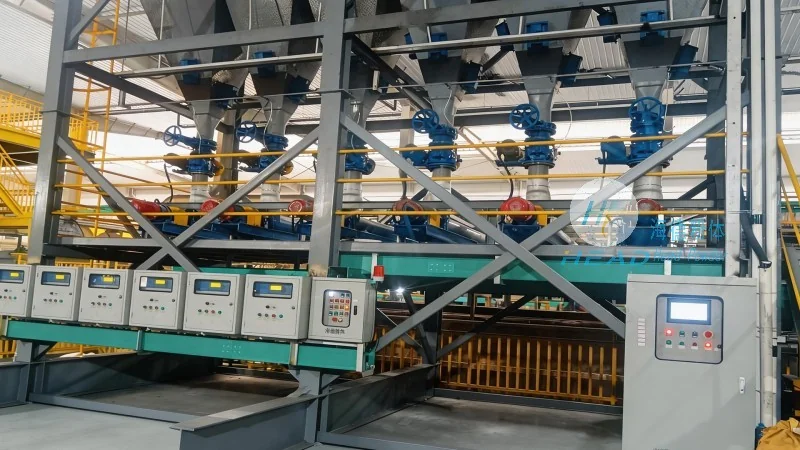
Application Scenarios and Industry Adaptability
Industries that benefit most from vacuum suction type powder conveying lines include chemical manufacturing, where various powders such as chemicals, pigments, and additives are transported. In the food industry, this technology is used to handle powders like flour, sugar, and spices, ensuring that the products remain free from contaminants and maintain their quality. The pharmaceutical sector also relies on this system for transporting active pharmaceutical ingredients (APIs) and other powders, as the enclosed and dust-free operation meets stringent regulatory requirements. Furthermore, the system's adaptability allows it to handle a wide variety of powder types, including fine powders, granules, and even cohesive materials, making it a versatile solution for diverse material handling needs. The ability to adjust the suction pressure and flow rate according to the specific characteristics of the powder being transported enhances its effectiveness in different operational contexts.
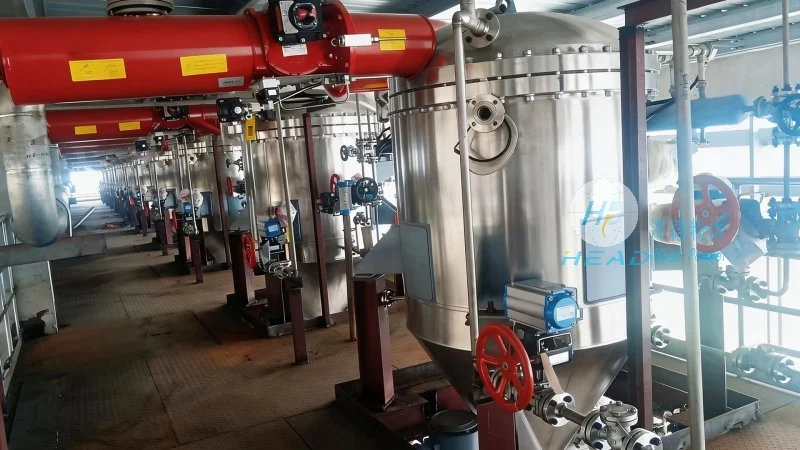
Advantages in Complex Operational Environments
Operating in complex environments, such as those with limited space or challenging layouts, is where the vacuum suction type powder conveying line excels. Unlike positive pressure systems that may require additional ventilation or exhaust systems, vacuum systems are self-contained and do not emit dust into the surrounding air. This makes them suitable for indoor applications where maintaining clean air quality is essential. The system's compact design also allows for installation in tight spaces, making it ideal for retrofitting into existing facilities without major structural modifications. Additionally, the low noise operation of modern vacuum pumps contributes to a safer and more comfortable working environment. These advantages make the vacuum suction type powder conveying line a preferred choice for facilities operating in confined or sensitive areas.
Conclusion and Company Overview
From its fundamental principle of using negative pressure to its wide range of application scenarios, the vacuum suction type powder conveying line represents a sophisticated solution for bulk powder handling. Developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a company based in Shandong, China, this technology combines efficiency, safety, and adaptability to meet the diverse needs of modern industries. Whether used in chemical, food, or pharmaceutical applications, the system's ability to transport powders reliably and in a dust-free manner ensures that it remains a vital component of material handling operations. As industries continue to prioritize product quality and operational efficiency, the vacuum suction type powder conveying line stands as a testament to innovative engineering and practical application.