

Principle and Working Scene Characteristics of Recycled Coke Powder Pneumatic Conveying System
Recycled coke powder, a byproduct in the coking industry, presents unique challenges for material handling and transportation. The pneumatic conveying system, as an efficient and flexible solution, has become a critical component in modern industrial processes for managing such powders. This article delves into the fundamental principles of a recycled coke powder pneumatic conveying system and explores the distinct characteristics of its working scenarios, offering insights into its practical applications and operational advantages.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is a professional enterprise based in Shandong, China. With a focus on engineering solutions for powder handling and material transportation, the company specializes in designing and implementing advanced pneumatic conveying systems tailored to the needs of various industrial sectors. HeadPowder's expertise lies in optimizing material flow, enhancing operational efficiency, and ensuring safety in the handling of bulk powders like recycled coke powder.
Principle of Pneumatic Conveying for Recycled Coke Powder
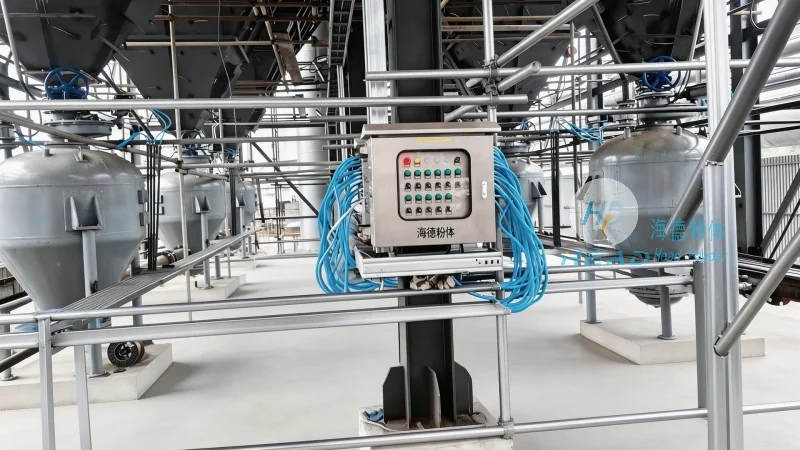
The core principle of a recycled coke powder pneumatic conveying system revolves around the use of air as the conveying medium to transport solid particles. This method typically involves creating a pressure differential or utilizing vacuum to move the powder through a pipeline. The system comprises several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. In the case of recycled coke powder, the system is engineered to handle the specific physical properties of the powder, such as its particle size, density, and moisture content, ensuring stable and efficient transport. The operation often involves either positive pressure (pressure conveying) or negative pressure (vacuum conveying), with the choice depending on the distance, volume, and environmental requirements of the application.
Working Scene Characteristics
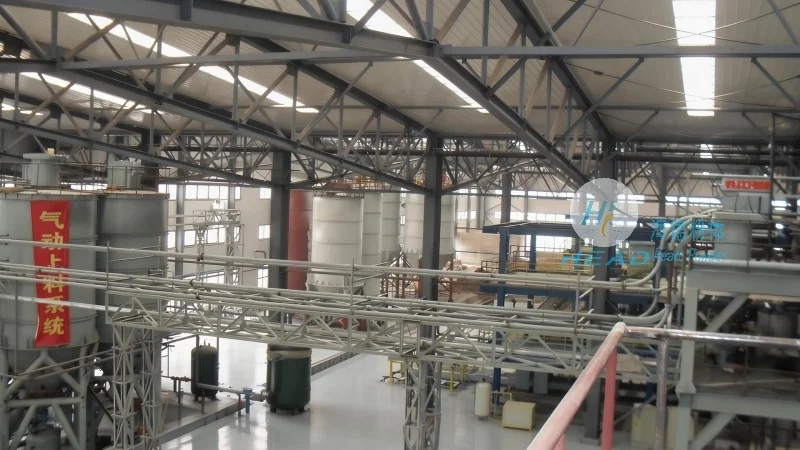
The working scene characteristics of a recycled coke powder pneumatic conveying system are shaped by the diverse industrial environments where it is applied. These characteristics include the system's adaptability to different production scales, the ability to integrate with existing industrial infrastructure, and the focus on minimizing material loss and contamination. In industrial settings, such as coking plants, steel mills, and chemical processing facilities, the system is used to transfer recycled coke powder from storage areas to processing units or to other parts of the production line. The working scenarios may vary from short-distance intra-factory transport to longer-distance inter-factory or even inter-site transfers, depending on the operational layout and logistical needs. Additionally, the system's design considerations, such as the selection of pipeline materials and the control of air flow, are tailored to the specific requirements of each working scene, ensuring optimal performance under varying conditions.
Operational Advantages and Practical Applications
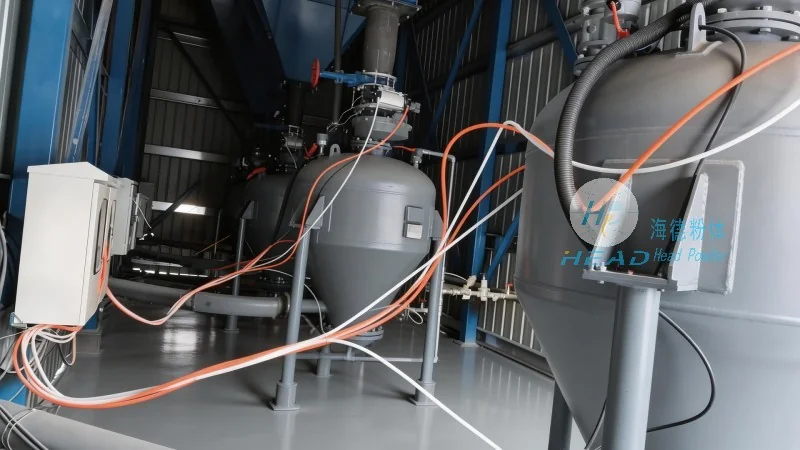
Implementing a recycled coke powder pneumatic conveying system offers several operational advantages that make it a preferred choice for many industries. These advantages include high efficiency in material transport, reduced labor costs compared to manual handling, and improved safety by minimizing direct human contact with the powder. The system also contributes to better environmental control, as it can be equipped with dust collection and filtration systems to prevent airborne particulate emissions. In practical applications, the system is used in the coking industry to recycle and reuse coke powder, thereby reducing waste and lowering production costs. It is also applicable in other sectors where bulk powder handling is required, such as in the production of cement, ceramics, and chemical products. The adaptability of the system allows it to be customized to meet the specific demands of different working scenes, ensuring reliable and consistent performance in various industrial environments.