

Principles and Operational Scenarios of Compound Fertilizer Powder Conveying
Compound fertilizer powder conveying systems are critical components in modern agricultural supply chains, designed to efficiently transport bulk materials from production sites to distribution centers or end-users. Understanding the underlying principles and the diverse operational scenarios where these systems are applied is essential for optimizing logistics and ensuring consistent product quality. This article explores the technical foundations of powder conveying, highlights key operational characteristics, and provides insights into the practical applications of such systems in the fertilizer industry.
The Fundamental Principles of Powder Conveying
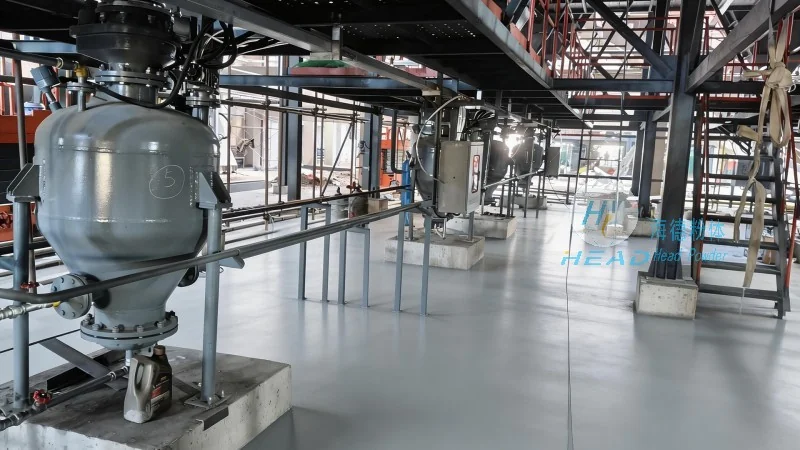
Powder conveying relies on a combination of mechanical and pneumatic principles to move granular materials. The core mechanisms include pressure differential, air flow, and material properties such as particle size, density, and moisture content. In pneumatic conveying systems, for example, air is used to create a flow that carries the powder through pipes. The choice of conveying method—whether dense-phase or dilute-phase—depends on factors like material characteristics and the distance to be covered. Dense-phase systems use higher air velocities and lower material concentrations, reducing the risk of blockages and ensuring smoother transport. Dilute-phase systems, conversely, operate at lower velocities and higher material concentrations, making them suitable for shorter distances or less abrasive materials. The selection of the appropriate conveying technology is crucial for maintaining product integrity and minimizing operational costs.
Key Operational Scenarios and Their Characteristics
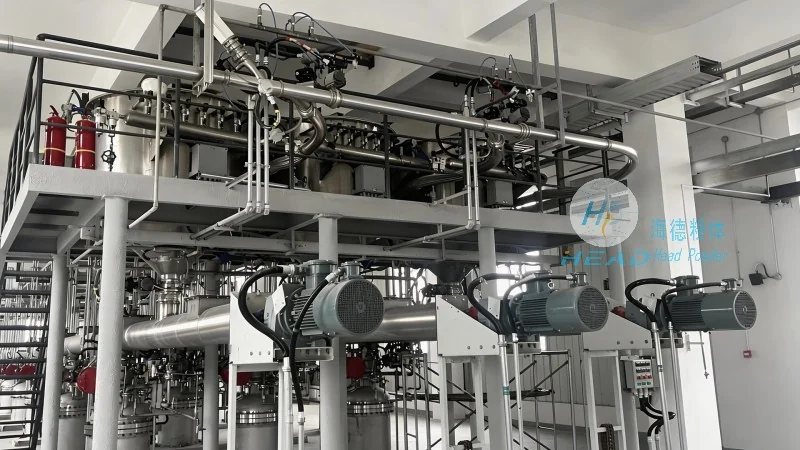
Compound fertilizer powder conveying systems are deployed in various operational scenarios, each with distinct requirements and challenges. One common scenario is the transfer of bulk fertilizer from storage silos to processing facilities or packaging lines. In this case, the system must handle large volumes of material while maintaining consistent flow rates to avoid bottlenecks. Another scenario involves the distribution of fertilizer from a central production plant to multiple regional depots or farms. Here, the conveying system must account for varying distances and potential changes in elevation, requiring adjustable pressure and flow controls. Additionally, some applications involve the integration of conveying systems with other processing equipment, such as mixing or blending units, where precise material delivery is critical to achieving the desired nutrient ratios. The operational characteristics of these scenarios, including material flow rates, pressure requirements, and system reliability, directly impact the overall efficiency of the fertilizer supply chain.
About Shandong HeadPowder Engineering Co., Ltd.
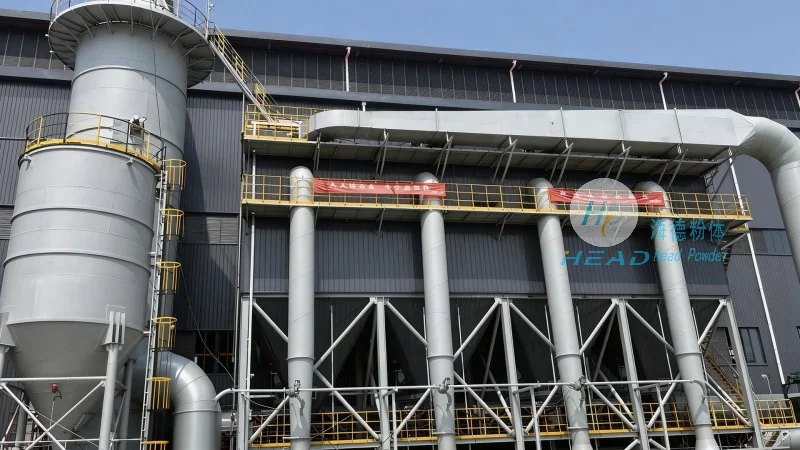
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for the powder handling industry. With a focus on innovation and customer-centric design, the company has developed advanced powder conveying systems tailored to the unique needs of the agricultural sector. HeadPowder's expertise lies in understanding the complex interactions between material properties and conveying technology, enabling the design of efficient, reliable, and cost-effective solutions. The company's operational base is located in Shandong, China, where it leverages local resources and industry knowledge to serve clients globally. By combining technical expertise with practical experience, HeadPowder ensures that its conveying systems meet the highest standards of performance and durability, supporting the sustainable growth of the fertilizer industry.
Conclusion and Practical Applications
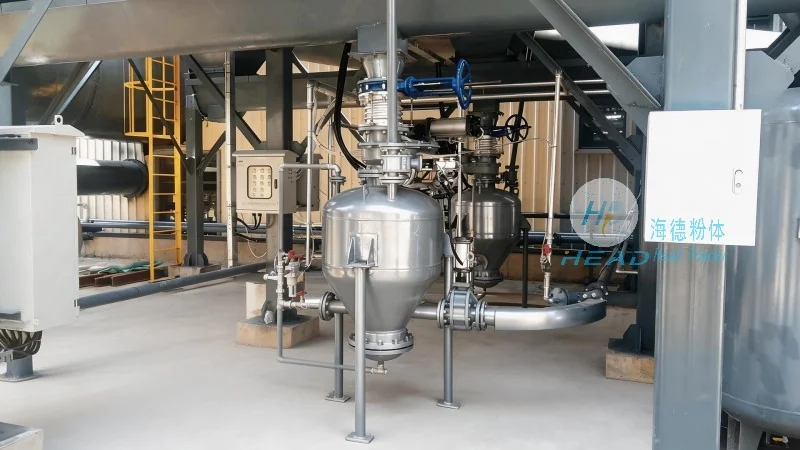
In summary, compound fertilizer powder conveying systems are essential for modern agricultural operations, leveraging fundamental principles of material handling to ensure efficient and reliable transport. The operational scenarios where these systems are applied vary widely, from on-site processing to long-distance distribution, each requiring tailored solutions to address specific challenges. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in developing and implementing these systems, providing the technical expertise and engineering solutions needed to optimize fertilizer logistics. By understanding the principles and characteristics of powder conveying, stakeholders in the fertilizer industry can make informed decisions to enhance operational efficiency, reduce costs, and support sustainable agricultural practices.