

Principle and Working Scene Characteristics of Sorghum Distiller's Grains Powder Conveying Line
For industrial applications involving the handling of sorghum distiller's grains, efficient and reliable powder conveying systems are crucial. The sorghum distiller's grains powder conveying line, developed by Shandong HeadPowder Engineering Co., Ltd., based in China, addresses the unique challenges associated with transporting this material. This article explores the underlying principles of the system and highlights its key characteristics in various operational environments.
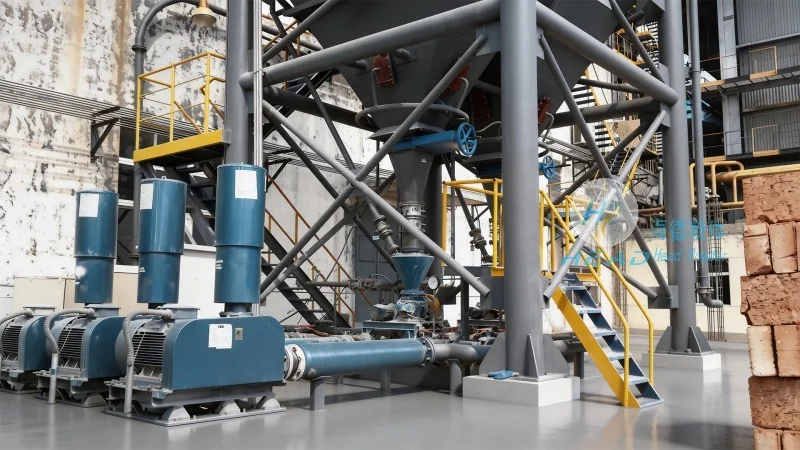
Overview of Sorghum Distiller's Grains and Conveying Needs
Sorghum distiller's grains are a byproduct of the ethanol production process, rich in nutrients and commonly used as animal feed or in biofuel applications. Due to their fine powder-like texture and varying moisture content, these materials present specific challenges during handling. Traditional conveying methods, such as belt conveyors or manual loading, often suffer from material buildup, clogging, and inefficient energy use. The sorghum distiller's grains powder conveying line from HeadPowder Engineering Co., Ltd. is engineered to overcome these issues, ensuring smooth and consistent material transport from source to destination.
Principle of Operation for the Powder Conveying Line
The core principle of the sorghum distiller's grains powder conveying line is based on a combination of mechanical and pneumatic technologies tailored to the physical properties of the material. The system typically consists of a hopper for material storage, a conveyor section (either screw or pneumatic), and a discharge mechanism. The hopper is designed with a sloped bottom to facilitate material flow, preventing blockages caused by agglomeration. The conveyor section uses a low-speed, high-torque motor to drive the screw or air duct, ensuring gentle handling of the fine particles. This approach minimizes material degradation and maintains the integrity of the distiller's grains, which is critical for downstream applications like feed production or biofuel processing.
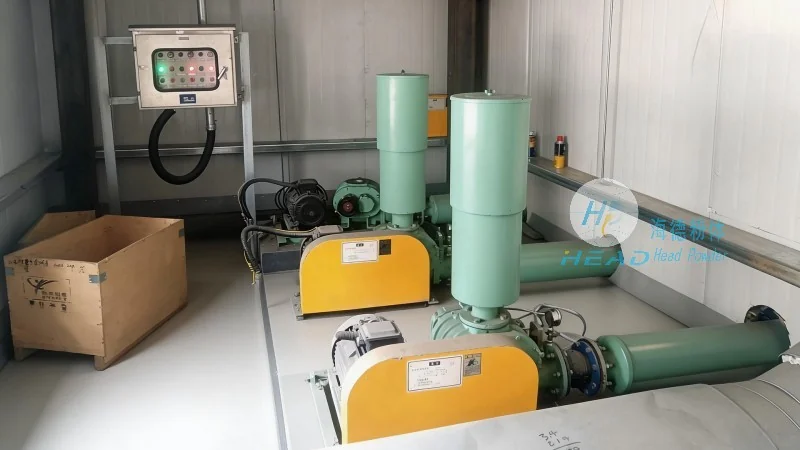
Key Working Scene Characteristics
The effectiveness of the sorghum distiller's grains powder conveying line is enhanced by its adaptability to diverse industrial settings. In a typical distillery, the system can be integrated into the ethanol production line, connecting the distiller's grains dryer to storage silos or feed mills. The line operates continuously, with adjustable flow rates to match production volumes, ensuring that material is transferred without interruption. In feed manufacturing facilities, the conveying line efficiently moves the distiller's grains from storage to mixing equipment, maintaining consistent moisture levels and preventing contamination. The system's compact design and low maintenance requirements make it suitable for both large-scale industrial plants and smaller-scale operations, providing flexibility across different operational scales.
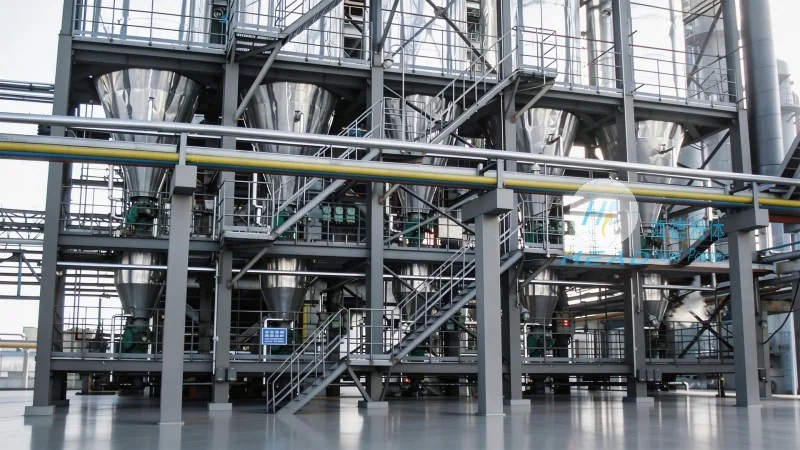
Advantages in Specific Application Environments
In environments where hygiene and material purity are paramount, such as in the production of animal feed, the sorghum distiller's grains powder conveying line excels. The enclosed design of the conveyor system prevents dust emissions and cross-contamination, meeting stringent industry standards. Additionally, the system's ability to handle varying particle sizes and moisture content makes it ideal for processing different batches of distiller's grains, ensuring uniform quality in the final product. For biofuel plants, the line's energy-efficient operation reduces operational costs while maintaining high throughput, contributing to the overall sustainability of the production process. The robust construction and durable components of the conveying line also ensure long-term reliability, minimizing downtime and maintenance expenses for industrial operators.
Conclusion and Practical Implications
The sorghum distiller's grains powder conveying line from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient handling of this valuable byproduct. By integrating advanced engineering principles with practical operational considerations, the system addresses the unique challenges of sorghum distiller's grains transportation. Its adaptability to various industrial settings, combined with its energy efficiency and reliability, makes it a preferred choice for companies in the ethanol and animal feed industries. As industries continue to seek sustainable and cost-effective processing solutions, the technology behind this powder conveying line remains a critical component in optimizing material flow and enhancing overall production efficiency.