

Principle and Working Scene Characteristics of Tonne Bag Quantitative Feeding Material Conveying Lin
For industrial operations that require precise material handling and feeding, the tonne bag quantitative feeding material conveying line has emerged as a critical solution. This system is designed to efficiently and accurately transfer bulk materials from tonne bags into processing equipment, ensuring consistent and reliable operation across various industrial applications. The following article explores the fundamental principles behind this technology and highlights its key working scene characteristics, providing insights into how it enhances productivity and operational efficiency.
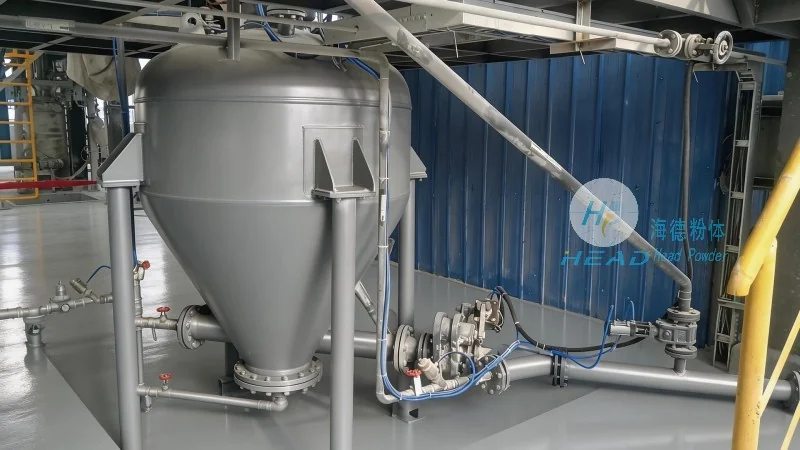
Understanding the Core Principle of Tonne Bag Quantitative Feeding Material Conveying Lines
The tonne bag quantitative feeding material conveying line operates on a principle of precision and automation. At its heart, the system integrates several key components, including a tonne bag opening mechanism, a quantitative feeder, and a conveying system. The process begins with the tonne bag being positioned and secured by the opening mechanism, which typically involves cutting or tearing the bag to release the contents. Once the bag is opened, the quantitative feeder, often a screw or volumetric feeder, measures and dispenses the material in controlled, pre-set quantities. This ensures that the exact amount of material is transferred to the conveying system, which then transports it to the processing unit. The entire process is automated, minimizing human intervention and reducing the risk of errors or inconsistencies.
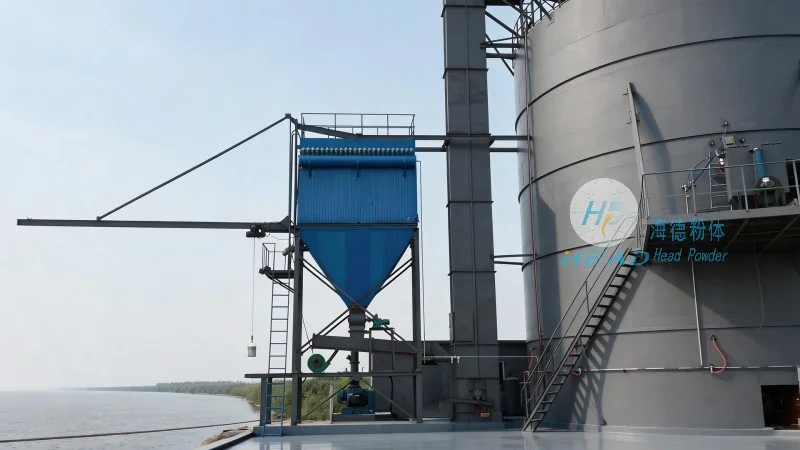
Key Working Scene Characteristics and Applications
The tonne bag quantitative feeding material conveying line is particularly well-suited for industrial environments where bulk material handling is essential. Its working scene characteristics include high accuracy in material measurement, consistent feeding rates, and the ability to handle a wide range of materials, from powders and granules to bulk solids. The system is commonly used in sectors such as chemical manufacturing, food processing, pharmaceuticals, and mining, where precise dosing and reliable material transfer are critical to product quality and process efficiency. For example, in chemical plants, this system ensures that raw materials are fed into reactors in exact proportions, preventing over or under-dosing that could affect reaction outcomes. In food processing facilities, it maintains the integrity of ingredients by delivering them in controlled quantities, which is vital for maintaining product consistency and meeting regulatory standards. The adaptability of the system to different material types and processing requirements makes it a versatile solution for diverse industrial applications.
Advantages and Operational Benefits
Implementing a tonne bag quantitative feeding material conveying line offers several advantages that enhance operational performance. One of the primary benefits is the significant improvement in material handling accuracy. By using a quantitative feeder, the system reduces material waste and minimizes the need for manual adjustments, which can be time-consuming and prone to errors. Additionally, the automated nature of the system increases operational efficiency, allowing for continuous and uninterrupted material transfer, even during long production runs. This leads to higher throughput and reduced downtime, which are crucial for maintaining competitive advantage in industrial markets. The system also contributes to improved workplace safety by minimizing manual handling of heavy tonne bags and reducing the risk of material spills or leaks. Furthermore, the modular design of the conveying line allows for easy integration with existing production lines, making it a cost-effective solution for upgrading or expanding material handling capabilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in industrial material handling solutions. With a focus on innovation and precision engineering, HeadPowder has developed a range of advanced conveying systems, including the tonne bag quantitative feeding material conveying line. The company is headquartered in Shandong, China, and has established a strong reputation for delivering high-quality, reliable equipment tailored to the specific needs of industrial clients. HeadPowder's commitment to quality and customer satisfaction is reflected in its rigorous testing processes and comprehensive after-sales support, ensuring that clients receive products that meet or exceed industry standards. The company's expertise in material handling technology enables it to provide customized solutions that enhance operational efficiency and support long-term business growth.