

Principle and Working Scene Characteristics of Calcium Nitrite Material Pneumatic Conveying Machine
Calcium nitrite, a critical chemical compound widely used in industrial applications such as corrosion inhibitors, concrete additives, and flame retardants, requires efficient and reliable material handling solutions. The pneumatic conveying machine designed for calcium nitrite material transport addresses these needs by leveraging air pressure to move the substance from one location to another. This article explores the fundamental principles behind such systems and highlights key working scene characteristics that make them suitable for calcium nitrite processing environments.
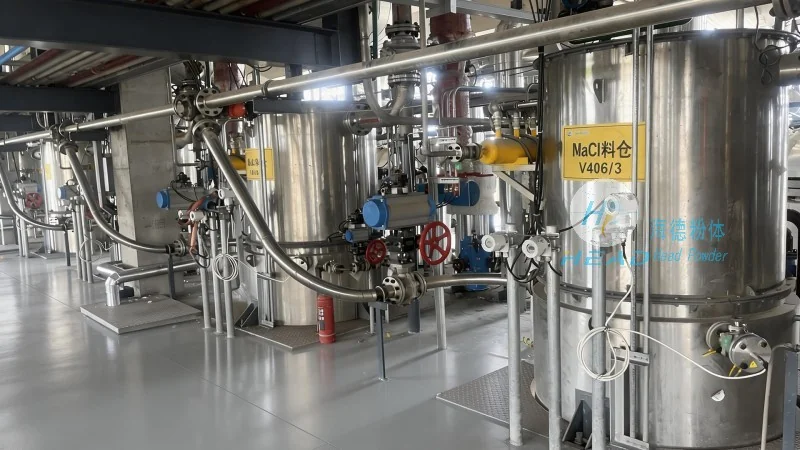
Core Principle of Pneumatic Conveying Technology
The pneumatic conveying machine operates on the principle of transporting bulk materials through a pipeline using compressed air or gas. In the case of calcium nitrite, the system typically employs a positive displacement or pressure-assisted design to ensure stable and consistent material flow. The process involves feeding the calcium nitrite powder into a hopper, where it is then drawn into a pipeline by the moving air stream. This method eliminates the need for mechanical components like belts or screws, reducing maintenance requirements and minimizing the risk of material contamination. The system’s efficiency is enhanced by controlling the air velocity and pressure to match the specific characteristics of calcium nitrite, such as its density and flowability.
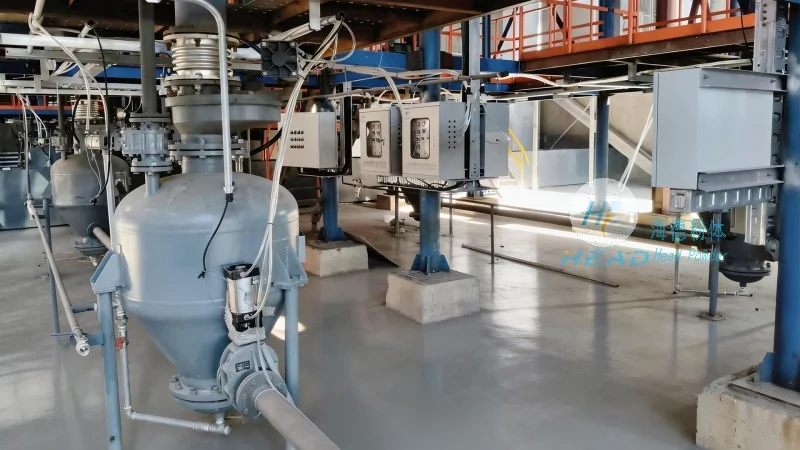
Working Scene Characteristics for Calcium Nitrite Applications
The pneumatic conveying machine for calcium nitrite is tailored to specific industrial settings, where the material’s properties and handling requirements dictate the system’s design. Key working scene characteristics include:
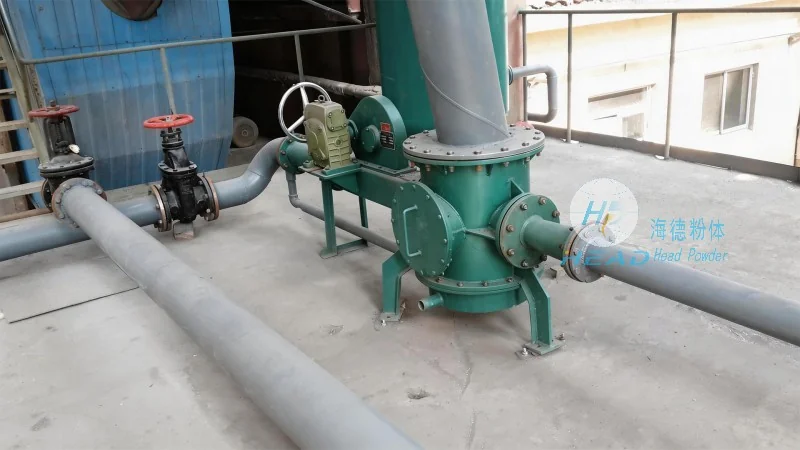
- High-Purity Environments: Calcium nitrite is often used in applications where contamination is unacceptable, such as in food processing or pharmaceuticals. The pneumatic conveying system’s enclosed pipeline design prevents dust and particles from escaping, maintaining a clean and controlled environment.
- Continuous Material Flow: In large-scale production facilities, the need for uninterrupted material transport is crucial. The system’s ability to handle continuous feed rates ensures that production lines operate smoothly without interruptions, which is essential for maintaining output efficiency.
- Space Optimization: Many industrial plants have limited floor space, and the pneumatic conveying machine’s compact design allows for flexible installation in confined areas. This is particularly beneficial in facilities where vertical or horizontal space is constrained, enabling efficient use of available real estate.
- Low Maintenance Requirements: Unlike traditional mechanical conveyors, the pneumatic system has fewer moving parts, reducing the likelihood of breakdowns and minimizing downtime. This makes it ideal for 24/7 operations in industrial settings, where reliability is paramount.
Application Examples in Industrial Settings
The calcium nitrite pneumatic conveying machine is widely used in various industrial sectors, including chemical manufacturing, construction materials production, and food processing. For instance, in a chemical plant producing calcium nitrite as a corrosion inhibitor, the system efficiently transports the material from storage silos to reaction vessels, ensuring precise dosing and consistent product quality. In a concrete additive factory, the machine moves calcium nitrite into mixing equipment, enabling uniform incorporation into the concrete mix, which enhances the final product’s durability and performance.
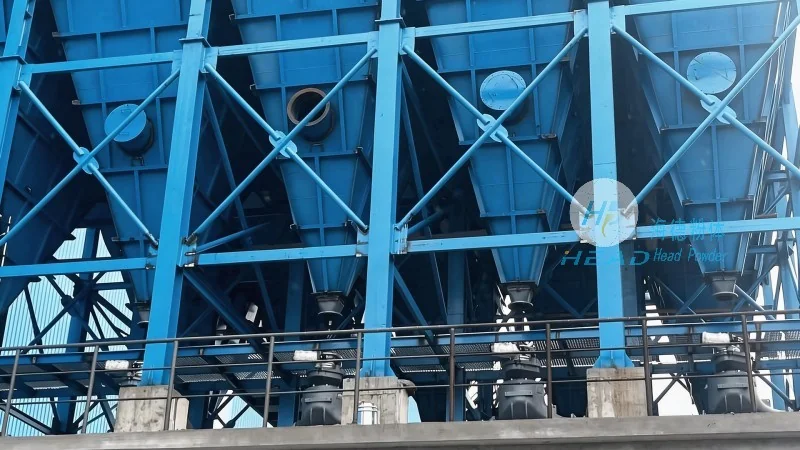
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of specialized material handling equipment, is dedicated to providing high-quality solutions for calcium nitrite and other industrial materials. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the chemical and construction industries. HeadPowder’s facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and a skilled workforce to produce reliable pneumatic conveying systems tailored to client needs. The company’s commitment to quality and efficiency has earned it a reputation for delivering durable and effective equipment that meets the demands of modern industrial operations.