

[Detailed Explanation of Carbon Black Powder Pneumatic Conveying Systems]
Carbon black powder pneumatic conveying systems are essential for efficient material handling in various industrial applications. These systems utilize air or other gases to transport carbon black powder from one location to another, offering a flexible and effective solution for industries that require reliable and low-maintenance material transport. The technology behind these systems has evolved significantly, providing enhanced performance and adaptability to meet the diverse needs of modern manufacturing processes.
Key Components of Carbon Black Powder Pneumatic Conveying Systems
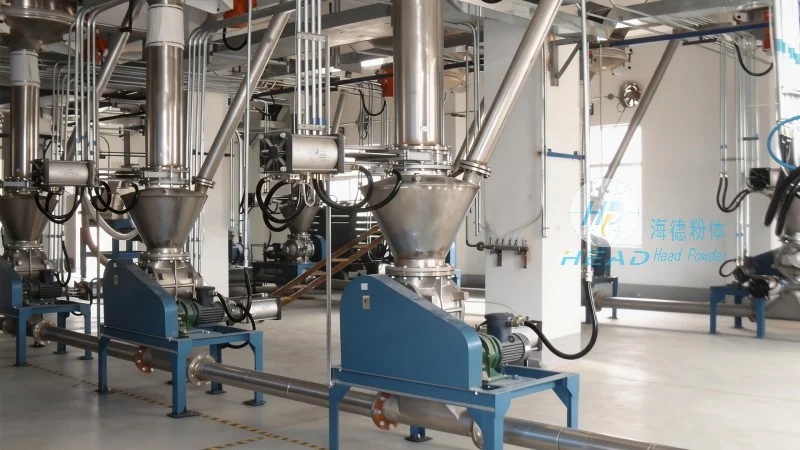
At the core of any carbon black powder pneumatic conveying system are several critical components that work in tandem to ensure efficient operation. The primary components include the hopper or feed tank, which holds the carbon black powder and feeds it into the system. The feeder, often a rotary valve or screw feeder, controls the flow rate of the powder into the conveying line. The conveying line itself, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of carbon black powder. The air compressor or blower provides the necessary pressure and airflow to move the powder through the system. Additionally, a filter system is crucial for capturing any fine particles and ensuring clean air discharge, maintaining environmental compliance and system longevity.
Types of Carbon Black Powder Pneumatic Conveying Systems
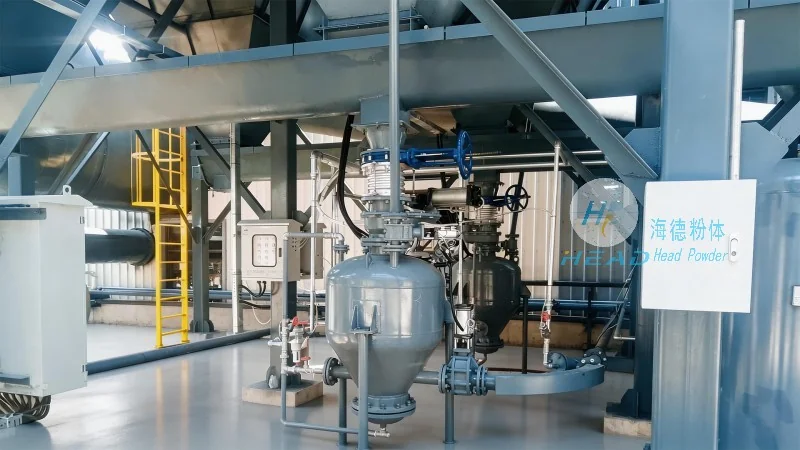
There are two main types of carbon black powder pneumatic conveying systems: positive pressure and negative pressure systems. Positive pressure systems operate by blowing air into the conveying line, pushing the powder forward. This type is commonly used for short to medium distances and for handling powders that are prone to caking or agglomeration. Negative pressure systems, on the other hand, draw air and powder into a vacuum, pulling them through the system. These systems are ideal for longer distances and for applications where dust control is a priority. The choice between positive and negative pressure systems depends on factors such as the distance of transport, the nature of the powder, and the specific requirements of the industrial process.
Advantages of Carbon Black Powder Pneumatic Conveying Systems
Carbon black powder pneumatic conveying systems offer numerous advantages over traditional mechanical conveying methods. One of the most significant benefits is the reduction in material handling costs and labor. By eliminating the need for manual handling or mechanical conveyors like belt or screw conveyors, these systems streamline the material transport process, leading to increased productivity. Additionally, pneumatic conveying systems provide better control over the flow rate and pressure, allowing for precise dosing and consistent material delivery. This is particularly important in applications where the quality of the carbon black powder is critical, such as in the production of tires, plastics, and other rubber products. The systems also offer enhanced safety features, as they minimize the risk of dust explosions and reduce exposure to airborne particles for operators. Furthermore, the flexibility of pneumatic conveying allows for easy integration with existing production lines and the ability to transport materials to multiple destinations from a single source.
Applications of Carbon Black Powder Pneumatic Conveying Systems
Carbon black powder pneumatic conveying systems are widely used in various industries that rely on carbon black as a key raw material. In the tire manufacturing industry, these systems are essential for transporting carbon black to mixing and compounding equipment, ensuring consistent quality and performance of the final tire products. The rubber and plastic industries also benefit from these systems, as they efficiently convey carbon black to extrusion and molding machines. Additionally, in the pigment and coating industries, carbon black is used as a pigment and reinforcing agent, and pneumatic conveying systems help in the precise and controlled delivery of this material. The food and pharmaceutical industries may also utilize these systems, though with specialized equipment to meet stringent hygiene and safety standards. The versatility of carbon black powder pneumatic conveying systems makes them suitable for a wide range of applications across different sectors.
Installation and Maintenance Considerations
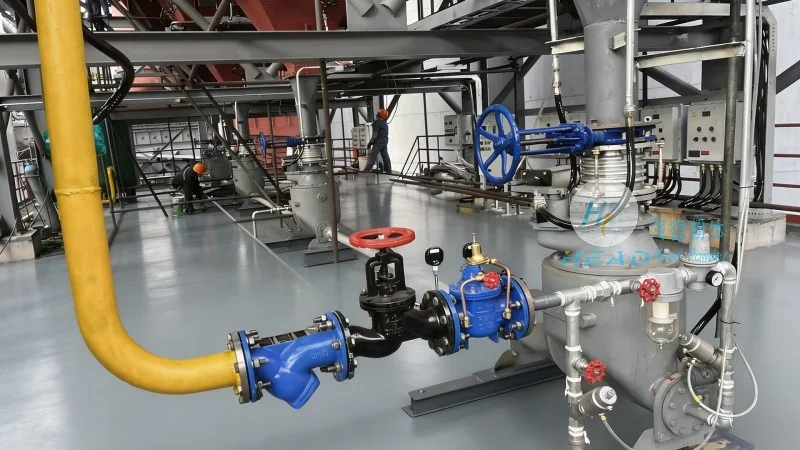
Proper installation and regular maintenance are crucial for the optimal performance and longevity of carbon black powder pneumatic conveying systems. During installation, it is important to ensure that all components are properly aligned and that the system is free from leaks, which can lead to air loss and reduced conveying efficiency. The hopper and feeder should be designed to prevent material buildup and clogging, especially for carbon black powders that may have a tendency to agglomerate. Regular cleaning of the conveying line and filter system is necessary to prevent the accumulation of fine particles, which can reduce airflow and increase pressure drop. Additionally, monitoring the air pressure and flow rate is essential to detect any issues early and prevent system failures. The use of high-quality, corrosion-resistant materials for the conveying line and components is recommended to withstand the abrasive nature of carbon black powder and extend the system's lifespan. Regular inspections and maintenance by qualified technicians can help identify potential problems before they escalate, ensuring the system operates efficiently and reliably.
Case Study: HeadPowder's Carbon Black Powder Pneumatic Conveying System
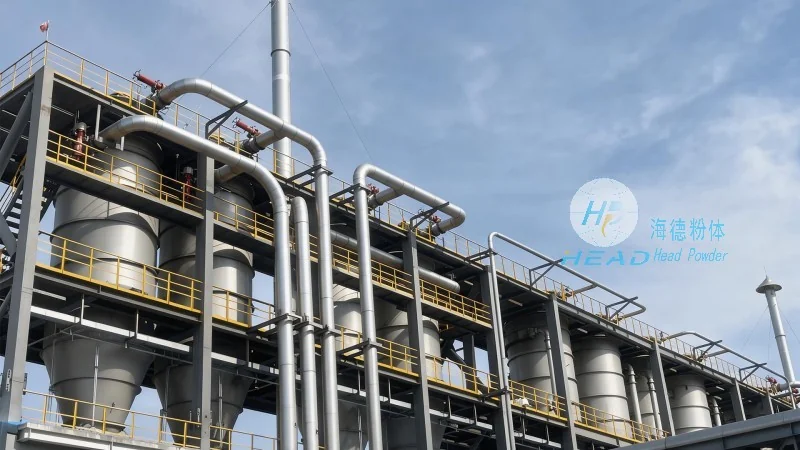
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, has successfully implemented carbon black powder pneumatic conveying systems for several clients in the tire and rubber industry. One notable case involved a tire manufacturer in China who required a system to transport carbon black from storage silos to the mixing plant. The system designed by HeadPowder featured a positive pressure design with a large hopper and rotary valve feeder, capable of handling high volumes of carbon black powder. The system was installed with stainless steel components to resist corrosion and equipped with a high-efficiency filter to meet environmental regulations. The client reported significant improvements in production efficiency, with reduced downtime and lower material handling costs. The system also provided better control over the carbon black dosage, leading to improved quality and consistency of the final tire products. This case study highlights the effectiveness of HeadPowder's carbon black powder pneumatic conveying systems in addressing the specific needs of industrial clients and delivering measurable benefits.
Conclusion
Carbon black powder pneumatic conveying systems are a vital technology for modern industrial applications, offering efficient, flexible, and reliable material handling solutions. With their ability to transport carbon black powder over various distances and in different industrial settings, these systems play a crucial role in enhancing productivity and product quality. The key to successful implementation lies in understanding the specific requirements of the application, selecting the appropriate system type, and ensuring proper installation and maintenance. Companies like Shandong HeadPowder Engineering Co., Ltd. continue to innovate and provide tailored solutions that meet the evolving needs of industries, ensuring the continued advancement of material handling technology.