

Application of Pneumatic Conveying Technology in Barley Malt Transport Design Optimization
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for the transportation of barley malt, leveraging cutting-edge pneumatic conveying technology to enhance efficiency and reliability in malt handling processes. Our expertise in this field ensures that the unique characteristics of barley malt—such as its moisture content, bulk density, and susceptibility to degradation—are carefully considered in the design and implementation of transport systems. By integrating state-of-the-art equipment and engineering principles, we deliver systems that meet the highest standards of quality and performance, supporting the needs of modern breweries and malt producers worldwide.
Advantages of Pneumatic Conveying for Barley Malt
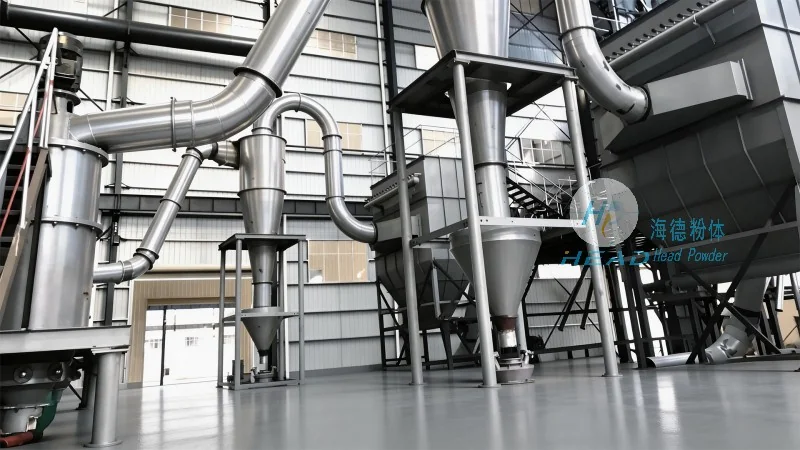
Pneumatic conveying systems offer several key advantages when transporting barley malt compared to traditional methods like belt conveyors or bucket elevators. The primary benefit is the ability to handle the material in a closed system, which minimizes exposure to air and reduces the risk of oxidation or microbial growth. This is critical for maintaining the quality and flavor profile of the malt, which is essential for brewing applications. Additionally, pneumatic conveyors can transport malt over longer distances with fewer intermediate transfer points, reducing the need for multiple equipment setups and streamlining the overall production flow. The technology also provides better control over the speed and direction of material movement, allowing for precise dosing and integration with downstream processes like mashing or drying. Furthermore, the gentle handling of malt by pneumatic systems reduces particle breakage and dust generation, contributing to a cleaner and safer working environment.
Optimizing Transport Design for Barley Malt
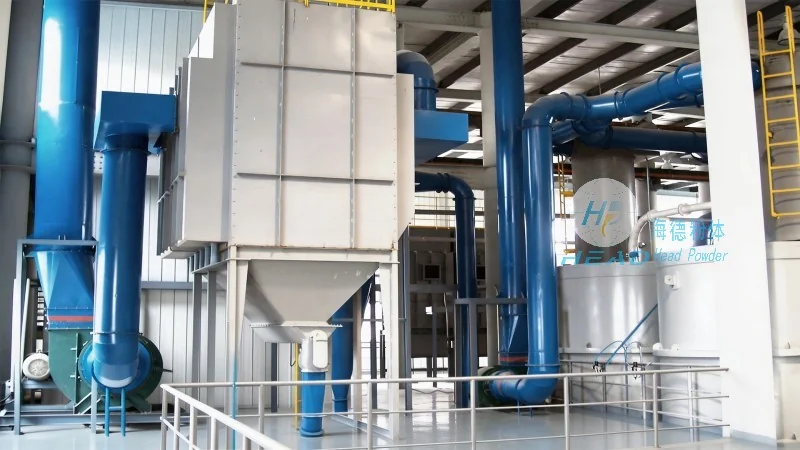
At Shandong HeadPowder Engineering Co., Ltd., we focus on optimizing the design of pneumatic conveying systems to meet the specific requirements of barley malt transport. This involves careful selection of components such as air pumps, ducts, and separation equipment to ensure efficient and gentle handling of the malt. For example, the use of low-velocity conveying systems can reduce product degradation by minimizing particle impact and abrasion. Our engineers also consider the moisture content and bulk density of the malt, as these factors influence the required air flow rates and pressure levels. By customizing the system design to the unique properties of each client's barley malt, we achieve optimal performance and minimize energy consumption. The design process also includes simulations and testing to validate the system's performance under real-world conditions, ensuring that the final solution is both effective and reliable.
Ensuring Quality and Efficiency in Malt Handling
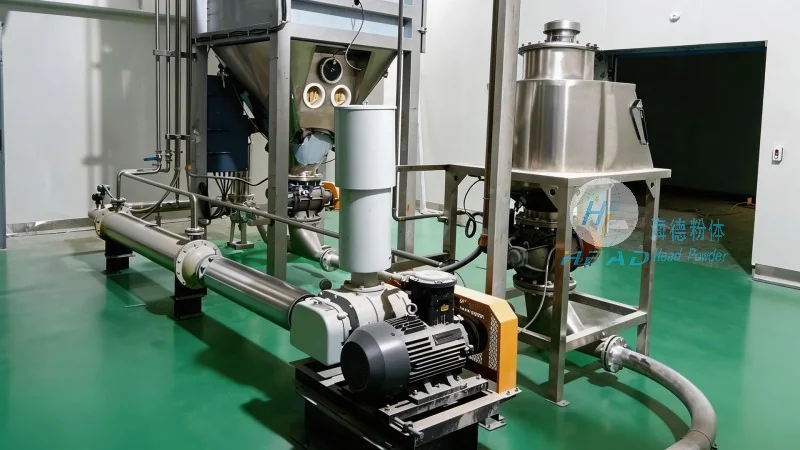
Quality control is a top priority in our pneumatic conveying solutions for barley malt. The closed system design prevents contamination from external sources and maintains consistent product quality throughout the transport process. This is particularly important for breweries that rely on high-quality malt to produce premium beers. Furthermore, the energy efficiency of pneumatic conveyors compared to other methods contributes to lower operational costs over time. Our systems are designed to minimize air leakage and optimize pressure usage, resulting in reduced energy consumption and lower utility bills for our clients. The reliability of pneumatic conveying technology also reduces downtime and maintenance needs, ensuring that malt can be transported consistently and reliably. This reliability is crucial for maintaining production schedules and meeting customer demand in the competitive brewing industry.
Customized Solutions for Diverse Malt Handling Needs
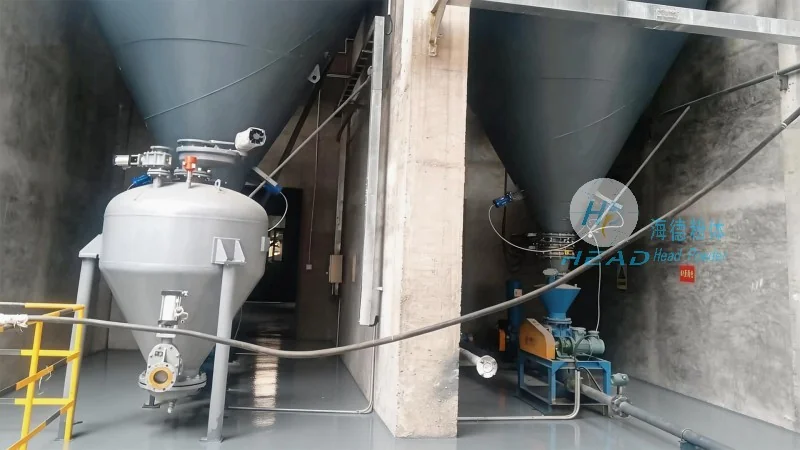
Shandong HeadPowder Engineering Co., Ltd. understands that different breweries and malt producers have varying needs when it comes to transporting barley malt. Whether the goal is to move large volumes of malt from storage to the brewhouse or to transfer smaller batches for quality testing, our team works closely with clients to develop customized solutions. We consider factors such as the scale of production, the distance of transport, and the specific processing requirements to design a system that meets all operational and quality standards. Our approach involves thorough consultation with the client to understand their unique challenges and then provide tailored recommendations that address those challenges effectively. By focusing on the specific needs of each project, we ensure that the pneumatic conveying system not only improves transport efficiency but also enhances the overall productivity and profitability of the malt handling operation. This customized approach has helped us serve a wide range of clients, from small craft breweries to large-scale industrial producers, all of whom have benefited from our expertise in pneumatic conveying technology.