

Effective Pneumatic Conveying Solutions for Silica Fume Powder Transport
HeadPowder, a leading engineering firm based in Shandong, China, specializes in advanced material handling technologies. The company's expertise lies in developing and implementing efficient pneumatic conveying systems tailored to the unique challenges of transporting fine powders like silica fume. With a focus on reliability and performance, HeadPowder provides customized solutions that enhance operational efficiency and reduce downtime in industrial applications.
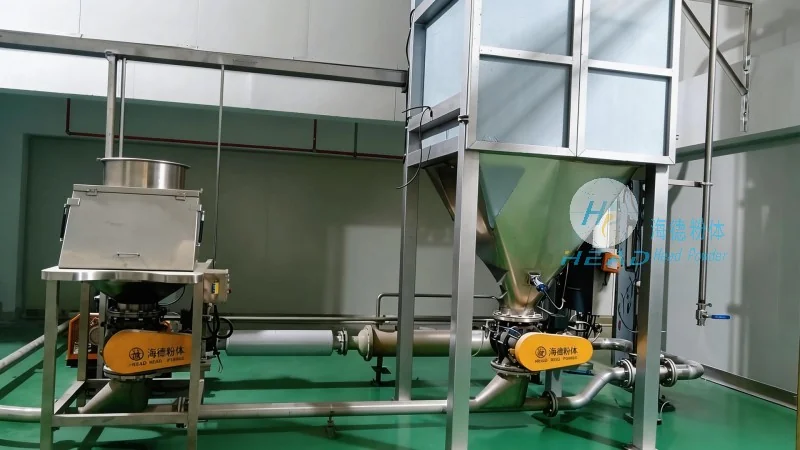
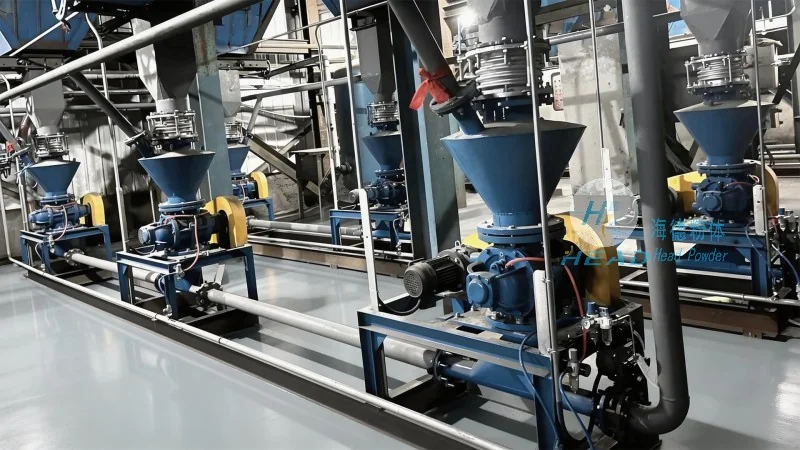
Advanced Pneumatic Conveying Systems for Silica Fume Handling
HeadPowder's pneumatic conveying systems are engineered to address the specific demands of silica fume powder transport. These systems utilize air pressure to move fine particles through pipelines, offering a dust-free and low-maintenance alternative to traditional methods. The technology is designed to handle the high moisture content and abrasive nature of silica fume, ensuring consistent flow rates and minimal product degradation. Key components include high-efficiency blowers, flexible hose connections, and specialized pipeline designs that optimize material movement while maintaining product integrity. By integrating advanced control systems, the equipment allows for precise regulation of air pressure and flow, enabling seamless integration into existing production lines. The systems are equipped with sensors and monitoring tools that provide real-time data on material flow, pressure, and temperature, allowing operators to adjust parameters dynamically and maintain optimal performance.
Applications and Operational Benefits
The pneumatic conveying solutions from HeadPowder are widely adopted in various industrial sectors where silica fume is a critical raw material. In concrete production, for example, the system ensures uniform mixing of silica fume with cement, leading to improved concrete strength and durability. In chemical processing facilities, the technology facilitates the safe and efficient transfer of silica fume between processing stages, reducing the risk of dust exposure and operational hazards. Operational benefits include reduced labor costs due to automated material handling, lower maintenance requirements compared to mechanical conveyors, and enhanced safety through enclosed systems that prevent dust dispersion. Additionally, the systems are designed for scalability, allowing companies to expand their operations without significant infrastructure changes. For instance, a manufacturing plant that increased its production capacity by 30% was able to integrate the pneumatic conveying system with minimal modifications, demonstrating the flexibility and adaptability of the technology.
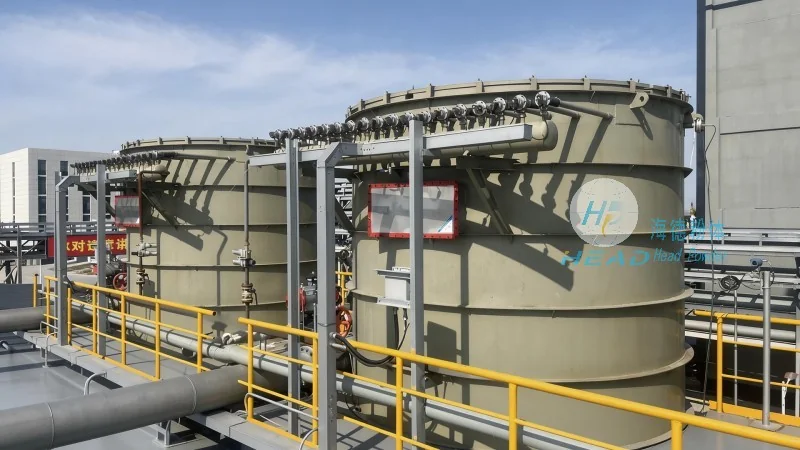
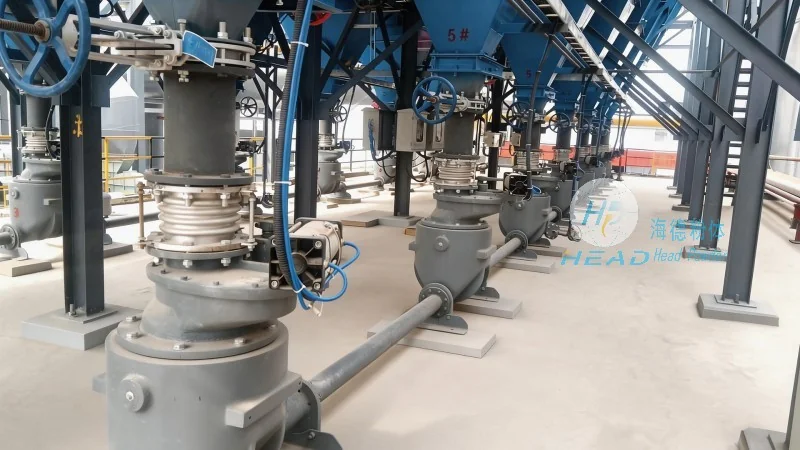
Customized Solutions for Diverse Industrial Needs
HeadPowder understands that each industrial application has unique requirements. The company offers customized pneumatic conveying systems that are tailored to specific process parameters, such as particle size distribution, moisture content, and production volume. This approach ensures that the system operates at peak efficiency, minimizing energy consumption and maximizing material throughput. The engineering team at HeadPowder works closely with clients to assess their current material handling challenges and develop solutions that align with their long-term goals. From initial design and installation to ongoing maintenance and support, HeadPowder provides comprehensive services to ensure the longevity and reliability of the conveying systems. The company's commitment to quality and innovation has earned it a reputation as a trusted partner in the material handling industry. For example, a client in the cement industry reported a 20% reduction in material handling time and a 15% decrease in energy costs after implementing HeadPowder's customized pneumatic conveying system, highlighting the tangible benefits of the technology.