

Working Principle and Features of Sodium Hypochlorite Powder Pneumatic Conveying System
Sodium hypochlorite is a widely used chemical in various industries, including water treatment, disinfection, and industrial cleaning. The efficient and safe transportation of sodium hypochlorite powder is crucial for industrial operations. A pneumatic conveying system is an effective solution for handling this powder, ensuring minimal dust generation and maintaining product integrity. This article explores the working principle and key features of a sodium hypochlorite powder pneumatic conveying system, highlighting its advantages and practical applications.
Working Principle of the Pneumatic Conveying System
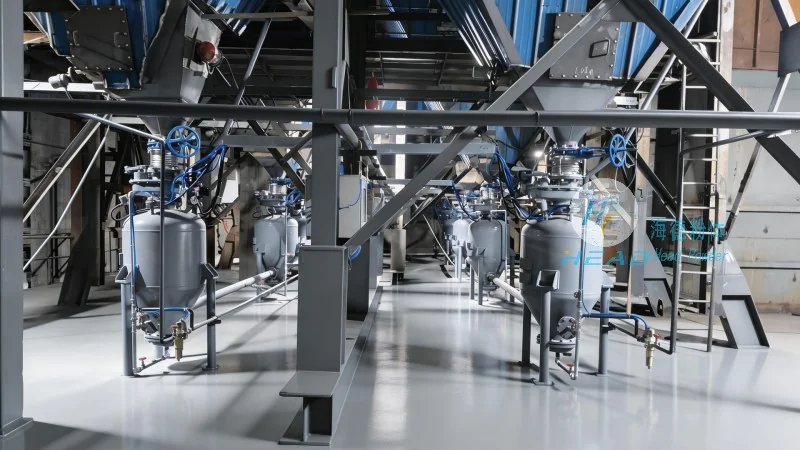
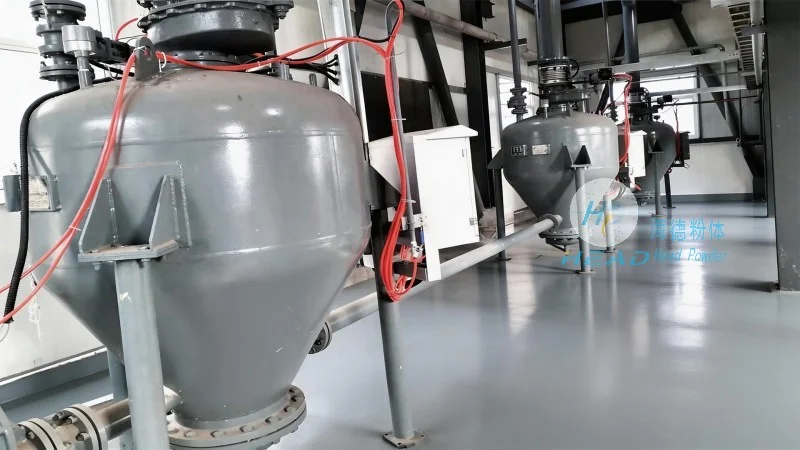
The sodium hypochlorite powder pneumatic conveying system operates based on the principle of air movement to transport dry powder materials. The system typically consists of a hopper, a rotary airlock valve, a conveying line, and a receiver. The process begins with the powder being fed into the hopper from a storage container. As the powder accumulates, a rotary airlock valve at the bottom of the hopper regulates the flow of powder into the conveying line. Simultaneously, a blower or compressor generates a high-pressure air stream that travels through the conveying line. The air stream carries the sodium hypochlorite powder particles along the pipeline, moving them from the source to the destination. The receiver at the end of the line collects the powder, and the air is then filtered and returned to the system or released, depending on the design. This continuous process ensures a steady and controlled flow of the powder, minimizing the risk of clogging and ensuring consistent performance.
Key Features and Advantages
The sodium hypochlorite powder pneumatic conveying system offers several notable features that make it suitable for industrial applications. First, it provides a dust-free environment, which is critical for maintaining safety and compliance with environmental regulations. Unlike traditional belt or bucket elevators, pneumatic systems do not generate significant dust, reducing the risk of inhalation hazards and contamination. Second, the system is highly flexible in terms of layout and can be adapted to various plant configurations. It can transport powder over long distances and through multiple bends and changes in elevation, making it versatile for different industrial setups. Third, the system ensures minimal product degradation, as the powder is not exposed to mechanical stress or excessive friction during transport. This is particularly important for sodium hypochlorite, which can be sensitive to temperature and moisture changes. Fourth, the system is easy to maintain and operate, with components that are readily accessible for inspection and cleaning. The rotary airlock valves and blower units are designed for low maintenance, reducing downtime and operational costs. Additionally, the system can be equipped with monitoring and control systems to optimize performance and ensure consistent operation.
Applications and Industrial Use Cases
Sodium hypochlorite powder pneumatic conveying systems are widely used in various industries where sodium hypochlorite is a key component. In water treatment plants, the system is used to transport sodium hypochlorite from storage tanks to dosing points, ensuring accurate and reliable dosing for disinfection. In industrial cleaning applications, the system delivers the powder to cleaning equipment, such as spray systems or foam generators, maintaining consistent cleaning performance. The system is also used in the chemical manufacturing industry, where sodium hypochlorite is produced and needs to be transported to packaging or processing units. Additionally, in the food and beverage industry, the system can be used for transporting sodium hypochlorite used in sanitizing equipment, ensuring food safety and compliance with hygiene standards. The versatility of the pneumatic conveying system makes it suitable for a wide range of applications, from small-scale operations to large industrial facilities.
Conclusion and Company Overview
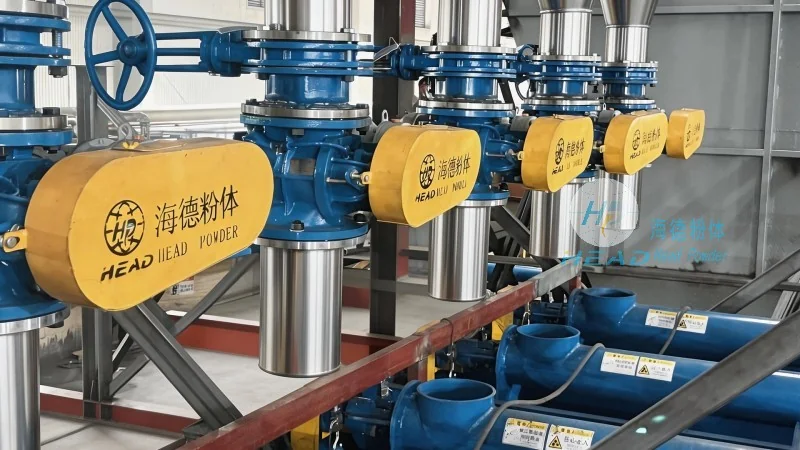
In conclusion, the sodium hypochlorite powder pneumatic conveying system is an efficient and reliable solution for transporting this critical chemical. Its working principle, based on air movement, ensures a dust-free and controlled transport process, while its key features, such as flexibility, minimal product degradation, and ease of maintenance, make it a preferred choice for industrial applications. The system is essential for maintaining safety, compliance, and operational efficiency in industries that rely on sodium hypochlorite. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of its clients. With a focus on innovation and customer satisfaction, HeadPowder provides solutions that enhance productivity and ensure the safe handling of sodium hypochlorite powder. Based in Shandong, China, the company leverages its expertise and advanced technology to deliver systems that meet the highest industry standards. Whether for water treatment, industrial cleaning, or chemical manufacturing, the sodium hypochlorite powder pneumatic conveying system from HeadPowder is a reliable and effective choice for businesses seeking to optimize their material handling processes.