

Principle and Working Scene Characteristics of Magnesium Hydroxide Powder Handling Systems
For industrial applications involving magnesium hydroxide powder, efficient and reliable handling systems are crucial. The systems designed by Shandong HeadPowder Engineering Co., Ltd. leverage advanced engineering principles to ensure optimal performance in various operational environments. This article explores the fundamental principles behind these systems and highlights key characteristics that define their effectiveness in real-world scenarios.
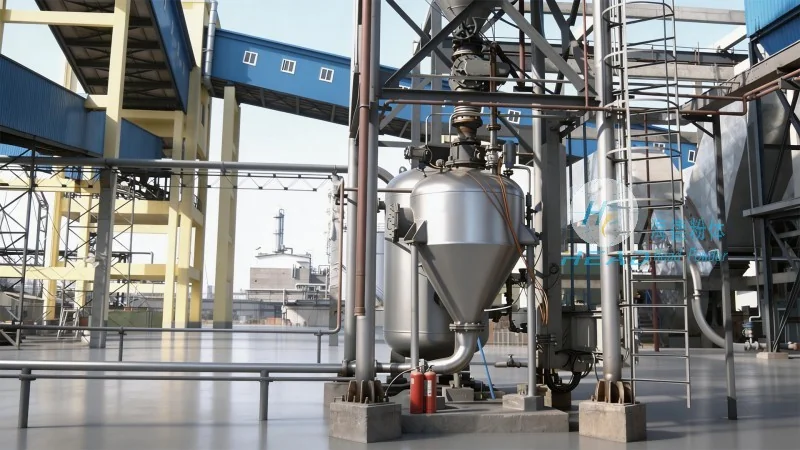
Core Principles of the Powder Handling System
The magnesium hydroxide powder handling system operates on several core principles that ensure consistent and safe material transport. The primary mechanism involves the use of specialized equipment such as screw conveyors, pneumatic conveyors, and bulk material handling devices. These components work in tandem to maintain the integrity of the powder, preventing agglomeration and ensuring uniform flow. The system is engineered to handle the unique properties of magnesium hydroxide, including its fine particle size and potential for static charge accumulation. By integrating features like anti-static coatings and controlled airflow, the system minimizes material degradation and ensures smooth operation. The design also emphasizes energy efficiency, with variable speed drives and optimized conveyor configurations reducing operational costs while maintaining high throughput rates.
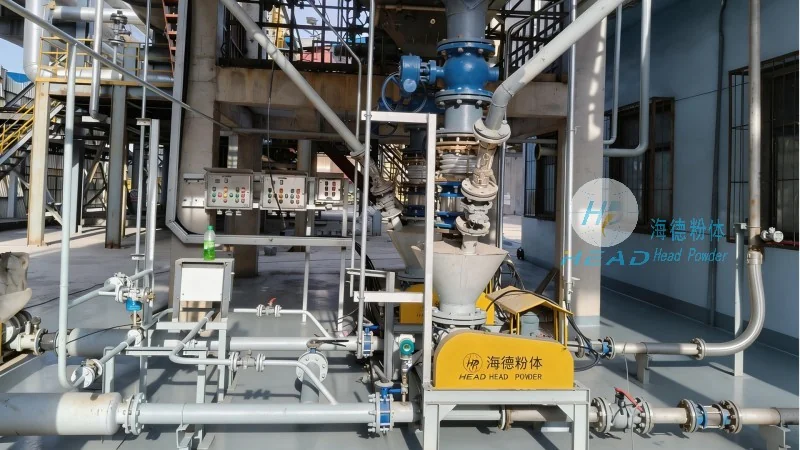
Key Working Scene Characteristics
Shandong HeadPowder Engineering Co., Ltd.'s magnesium hydroxide powder handling systems are tailored to meet diverse operational requirements across different industries. The systems are particularly effective in applications such as chemical manufacturing, pharmaceutical processing, and environmental remediation, where precise control over powder flow is essential. In chemical plants, the system ensures that magnesium hydroxide is delivered to reactors and processing units without clogging or loss of material. In pharmaceutical settings, the handling system maintains the purity and consistency of the powder, which is critical for product quality and regulatory compliance. Environmental applications, such as flue gas desulfurization, benefit from the system's ability to handle large volumes of powder while minimizing dust emissions and ensuring environmental safety. The systems are also adaptable to different production scales, from small-scale laboratory operations to large-scale industrial facilities, making them versatile for various production needs.
Technical Advantages and Performance Metrics
The magnesium hydroxide powder handling systems from Shandong HeadPowder Engineering Co., Ltd. offer several technical advantages that enhance operational efficiency and reliability. One key advantage is the system's ability to handle fine powders without significant pressure drop or material buildup. This is achieved through the use of high-quality materials and precise engineering, which reduces maintenance requirements and extends the service life of the equipment. The systems also feature advanced control systems that allow for real-time monitoring and adjustment of flow rates, ensuring consistent performance under varying load conditions. Performance metrics such as throughput capacity, energy consumption per ton of material, and dust emission levels are optimized to meet industry standards. The systems are designed to operate with minimal downtime, with quick maintenance access points and modular components that facilitate easy repairs and replacements. Additionally, the systems comply with relevant safety and environmental regulations, providing peace of mind to operators and ensuring regulatory compliance.
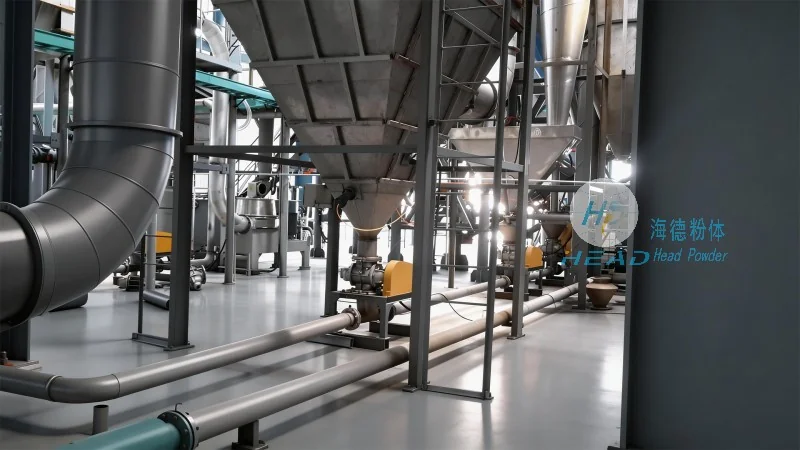
Application Examples and Case Studies
Real-world applications of the magnesium hydroxide powder handling systems demonstrate their effectiveness in various industrial settings. For instance, in a chemical manufacturing plant, the system successfully handled 500 tons of magnesium hydroxide per day, maintaining a consistent flow rate and preventing any material blockages. The plant reported a 20% reduction in energy consumption compared to traditional handling methods, attributed to the efficient design of the conveyor system. In a pharmaceutical facility, the system ensured that the magnesium hydroxide powder was delivered to production lines with minimal contamination, resulting in higher product quality and reduced waste. Environmental projects, such as the installation of flue gas desulfurization units, utilized the system to transport large volumes of powder to the treatment facilities, with the system's dust control features significantly reducing air pollution. These case studies highlight the system's adaptability and reliability in diverse operational environments, making it a preferred choice for industries requiring high-performance powder handling solutions.