

Principle and Working Scene Characteristics of Powder Tanker Material Conveying System Equipment
HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design, development, and production of advanced material conveying systems tailored for powder tanker applications. Our company, Shandong HeadPowder Engineering Co., Ltd., has been committed to delivering high-quality solutions that meet the diverse needs of industrial sectors, ensuring efficient and reliable material handling processes.
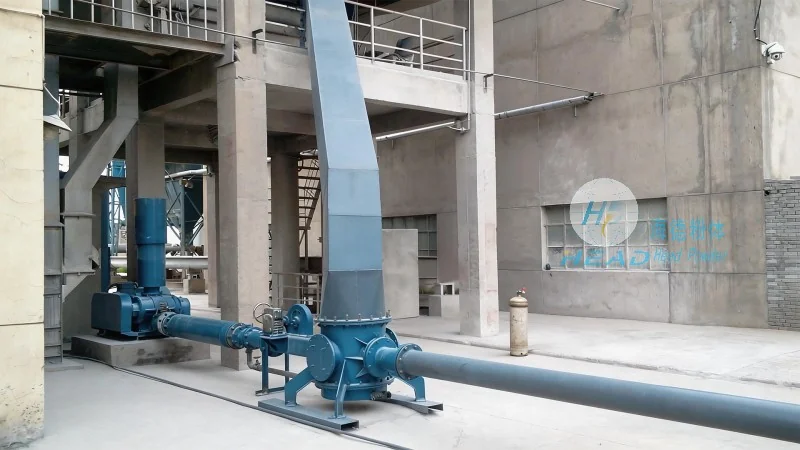
About HeadPowder: A Leading Provider of Material Conveying Solutions
HeadPowder, headquartered in Shandong, China, is a reputable enterprise dedicated to providing innovative material conveying systems. With years of experience in the industry, we have established ourselves as a trusted partner for businesses seeking efficient and reliable solutions for powder transportation and handling. Our team of experts focuses on understanding client requirements and developing customized systems that enhance operational efficiency and safety.
Principle of Powder Tanker Material Conveying Systems
The core principle of our powder tanker material conveying systems revolves around the seamless transfer of bulk materials from the tanker to processing or storage facilities. These systems typically integrate advanced pneumatic or mechanical components, such as rotary valves, conveyor belts, and airlocks, to ensure a controlled and continuous flow of material. The design emphasizes minimizing material degradation, preventing contamination, and optimizing energy consumption. By leveraging precise engineering and quality materials, our systems maintain consistent performance under various operational conditions, ensuring reliable operation in industrial settings.
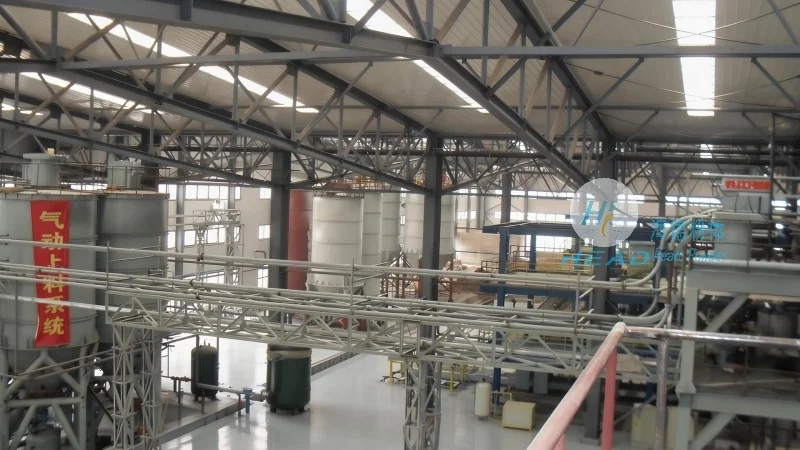
Working Scene Characteristics of the Systems
Our powder tanker material conveying systems are designed to operate in diverse industrial environments, including chemical, food, pharmaceutical, and mining sectors. The working scene characteristics highlight the adaptability and robustness of the equipment, which can handle a wide range of powder types, from fine powders to bulk materials. The systems are engineered to withstand harsh conditions, such as high temperatures, corrosive substances, and abrasive materials, ensuring long-term durability and minimal maintenance. In addition, the modular design allows for easy integration with existing production lines, reducing downtime and enhancing overall productivity. The systems also prioritize safety, incorporating features like automatic shut-off valves and pressure relief mechanisms to prevent accidents and ensure operator safety.
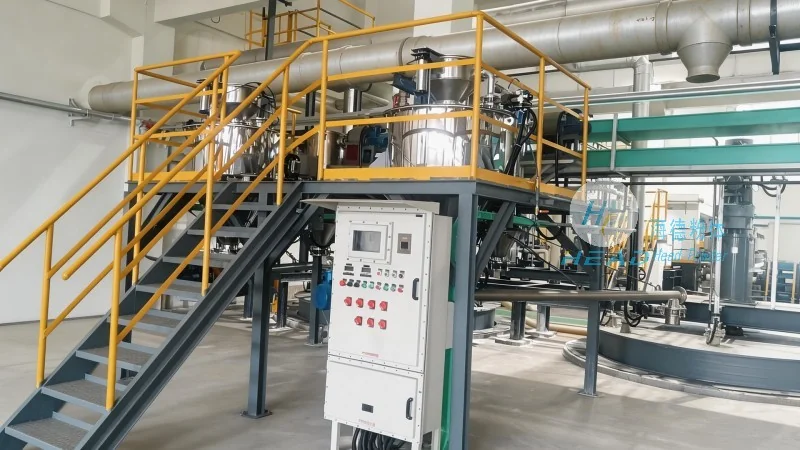
Key Features and Benefits
HeadPowder's powder tanker material conveying systems are equipped with several key features that contribute to their effectiveness and efficiency. These include high-capacity conveying capabilities, precise control over material flow, and low maintenance requirements. The systems are designed to minimize material loss and contamination, which is crucial for industries where product purity is paramount. Additionally, the advanced control systems enable real-time monitoring and adjustment, allowing operators to optimize performance based on specific production needs. The robust construction ensures long service life, reducing the need for frequent replacements and associated costs. Overall, our systems provide significant benefits, including increased productivity, reduced operational costs, and enhanced safety in material handling processes.
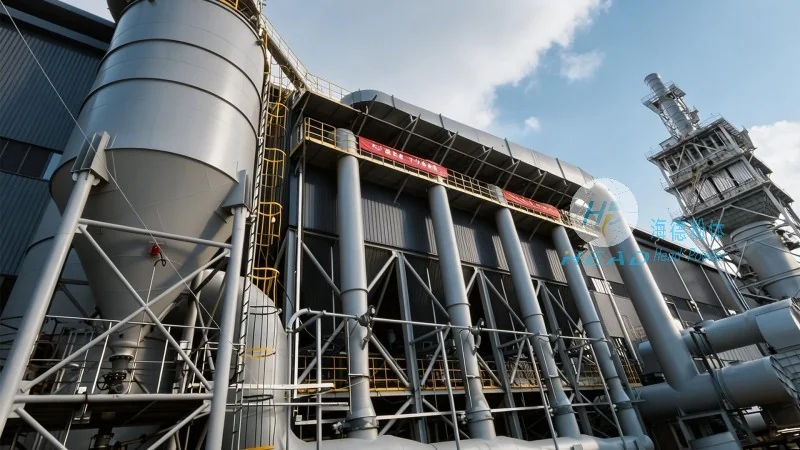
Application Examples and Industry Impact
The versatility of our powder tanker material conveying systems is evident in their application across various industries. In the chemical industry, the systems are used to transport raw materials and finished products, ensuring smooth production workflows. In the food and pharmaceutical sectors, the equipment is crucial for maintaining product quality and safety, as it prevents cross-contamination and ensures consistent material handling. The mining industry benefits from the efficient transportation of ore and other bulk materials, improving extraction and processing efficiency. By addressing the unique challenges of each industry, our systems contribute to improved operational performance and competitive advantage for our clients. The consistent performance and reliability of our equipment have made HeadPowder a preferred choice for businesses seeking dependable material conveying solutions.
Conclusion and Future Outlook
HeadPowder continues to innovate and advance its powder tanker material conveying systems, focusing on enhancing performance, efficiency, and sustainability. With a strong commitment to quality and customer satisfaction, we remain dedicated to providing solutions that meet the evolving needs of the industrial market. Our systems are designed to adapt to future technological advancements, ensuring that our clients can leverage the latest innovations in material handling. As we move forward, HeadPowder will continue to be at the forefront of developing cutting-edge conveying solutions, supporting the growth and success of industries worldwide.