

Principle and Working Scene Characteristics of Alumina Hydroxide Material Handling System Equipment
Alumina hydroxide, a critical industrial chemical, demands efficient and reliable material handling solutions to ensure seamless production processes. The material handling systems engineered for alumina hydroxide operations integrate advanced technology with robust construction to deliver optimal performance. This article explores the underlying principles of these systems and highlights key working scene characteristics that define their effectiveness in industrial settings.
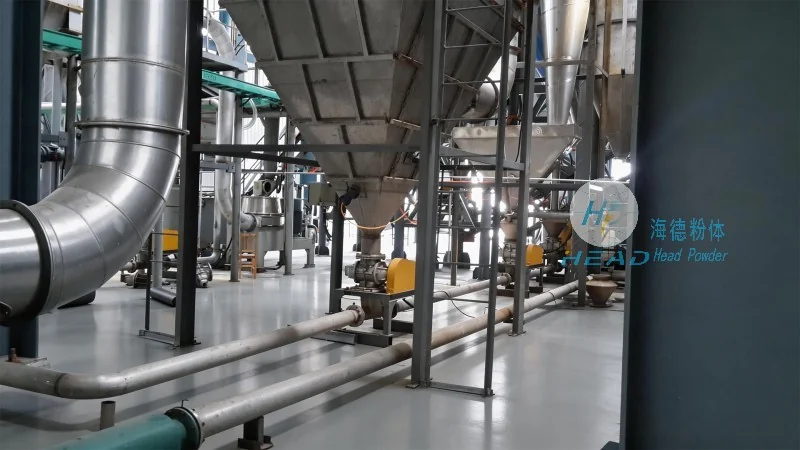
HeadPowder: A Leading Provider of Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a prominent company based in Shandong, China, specializes in the design, manufacturing, and supply of advanced material handling equipment. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for industries dealing with alumina hydroxide and similar materials. The company’s expertise lies in developing customized solutions that address the unique challenges of material handling in various industrial applications.
The Core Principles of Alumina Hydroxide Material Handling Systems
The material handling systems for alumina hydroxide operate on several fundamental principles to ensure safe and efficient transport. These systems typically include conveyors, elevators, and storage units, each tailored to the physical properties of alumina hydroxide (granular or powder form). The primary principle is maintaining material integrity during transport, preventing segregation, agglomeration, or contamination. This is achieved through specialized equipment like screw conveyors, belt conveyors, and pneumatic conveying systems, optimized for alumina hydroxide characteristics.
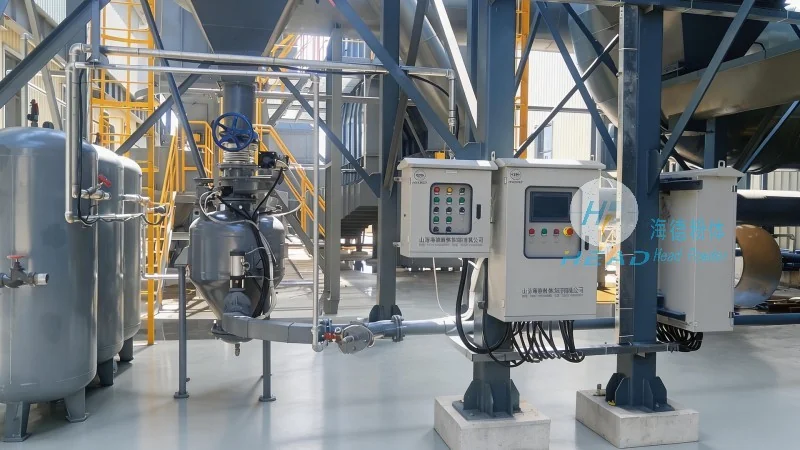
Working Scene Characteristics: Optimizing Material Flow
The working scene characteristics of alumina hydroxide material handling systems are critical to real-world industrial effectiveness. These include handling varying material loads, maintaining consistent flow rates, and adapting to operational conditions. In industrial settings, the systems must integrate with existing production lines for seamless material transfer from storage to processing units. The working scene also considers space constraints, environmental factors, and safety protocols, all addressed through equipment design and implementation.
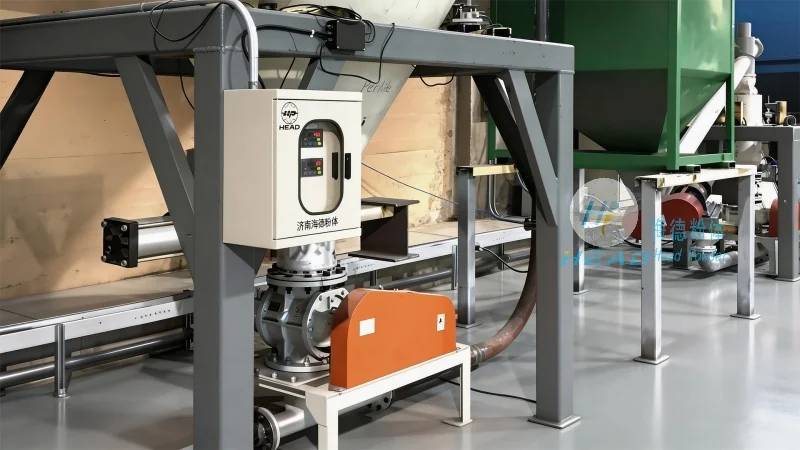
Key Features and Benefits of HeadPowder's Systems
HeadPowder's alumina hydroxide material handling systems feature high-capacity conveying, low maintenance, and energy-efficient operation. The systems minimize material degradation and loss, ensuring optimal condition throughout handling. Constructed from durable materials to withstand alumina hydroxide's corrosive/abrasive nature, they offer long-term durability and cost-effectiveness.
Application Scenarios and Operational Efficiency
The working scene characteristics are evident in application scenarios like aluminum, ceramics, and alumina-based product production. Here, the systems maintain production continuity and reduce downtime by handling large material volumes. This boosts operational efficiency and lowers production costs, making them a valuable asset for industrial operations.