

Introduction to the Structure and Working Principle of PUR Pneumatic Conveying Equipment
PUR pneumatic conveying equipment, also known as pneumatic conveyors, represents a critical technology in material handling and processing across various industrial sectors. These systems are designed to transport bulk materials such as powders, granules, and fine particles through a pipeline using air or other gases as the conveying medium. The efficiency and reliability of PUR pneumatic conveyors make them indispensable in applications ranging from food processing and pharmaceuticals to chemical manufacturing and construction materials.
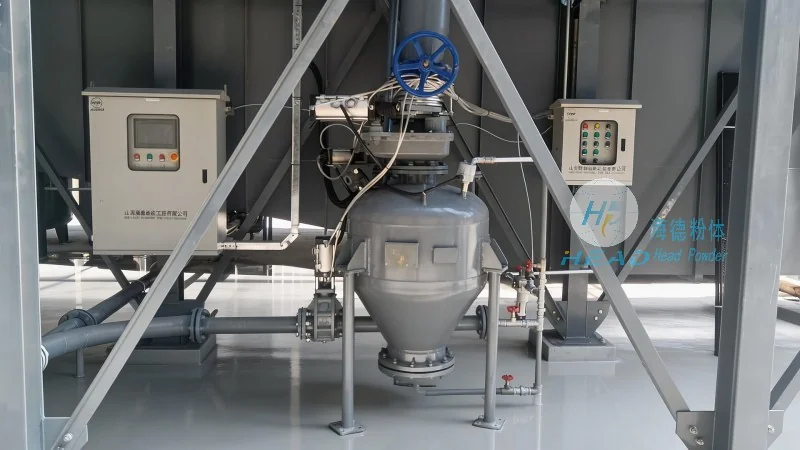
The core structure of a typical PUR pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. The primary components include the feeding unit, conveying pipeline, air supply system, and separation or discharge equipment. The feeding unit is responsible for introducing the material into the system, often through a hopper or feeder that ensures a consistent flow rate. This unit is crucial for maintaining the integrity of the material and preventing blockages or uneven distribution.
The conveying pipeline, typically made from durable materials like polyurethane (PUR) or other corrosion-resistant polymers, forms the main pathway for the material and air mixture. The choice of pipeline material is critical as it must withstand the abrasive nature of many bulk materials and resist chemical degradation. The pipeline is usually arranged in a straight or slightly curved configuration to minimize pressure losses and ensure smooth material flow. In some designs, the pipeline may include bends, expansion joints, or special fittings to accommodate changes in direction or elevation.
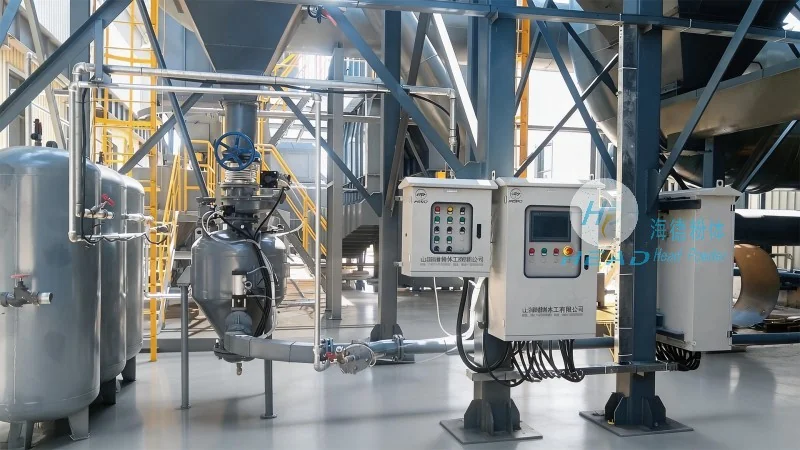
At the heart of the system is the air supply unit, which generates the necessary pressure and volume of air to move the material through the pipeline. This unit typically includes a blower or compressor, a filter to remove contaminants from the air, and a control valve to regulate the airflow. The air pressure and flow rate are carefully controlled to achieve optimal conveying performance, balancing the need for efficient material transport with energy efficiency and system longevity.
The separation or discharge equipment is the final component of the system, responsible for separating the conveyed material from the air and delivering it to the target destination. This may involve a cyclone separator, a bag filter, or a rotary valve, depending on the specific application and material characteristics. The separator ensures that the material is collected in a clean and controlled manner, while the air is either recycled back into the system or vented to the atmosphere after being filtered.
The working principle of PUR pneumatic conveying is based on the physical properties of the material and the behavior of the air flow. When the material is introduced into the pipeline, it is suspended in the air stream, which carries it along the pipeline. The velocity of the air is maintained above the material's terminal velocity to prevent deposition or settling. The system operates on the principle of fluidization, where the material particles are kept in motion by the continuous airflow, allowing them to be transported over long distances without the need for mechanical components like belts or buckets.
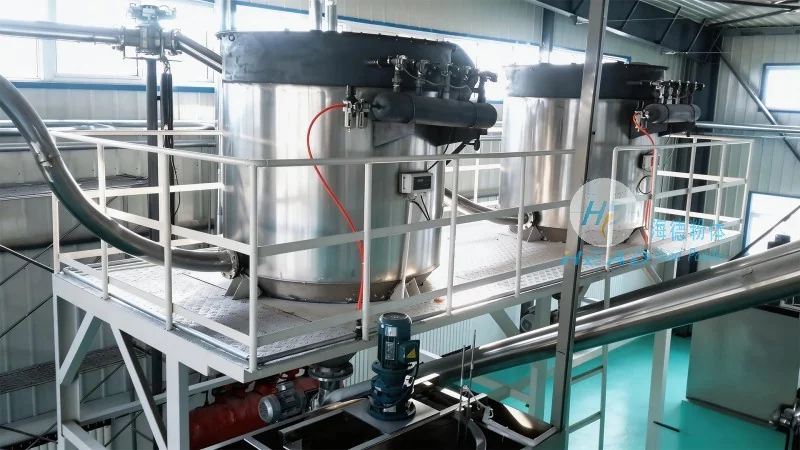
The advantages of PUR pneumatic conveyors over traditional mechanical conveying systems are significant. These systems offer high efficiency in material transport, with the ability to handle a wide range of materials, including those that are abrasive, dusty, or have high moisture content. The lack of moving parts in the pipeline reduces maintenance requirements and extends the service life of the equipment. Additionally, PUR materials used in the construction of the pipeline provide excellent resistance to wear and corrosion, ensuring long-term reliability in harsh operating conditions.
HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying equipment, specializes in the design, manufacturing, and supply of high-quality PUR pneumatic conveyors. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the material handling industry. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing facilities and a team of experienced engineers to develop cutting-edge solutions tailored to the diverse needs of its clients.
HeadPowder's PUR pneumatic conveying systems are engineered to meet the stringent requirements of modern industrial applications. The company's product line includes a variety of configurations, such as pressure and vacuum systems, to accommodate different material handling scenarios. Each system is customized based on the specific characteristics of the material, the required conveying distance, and the operational environment. The company's engineering team works closely with clients to provide comprehensive solutions that enhance productivity, reduce downtime, and improve overall operational efficiency.
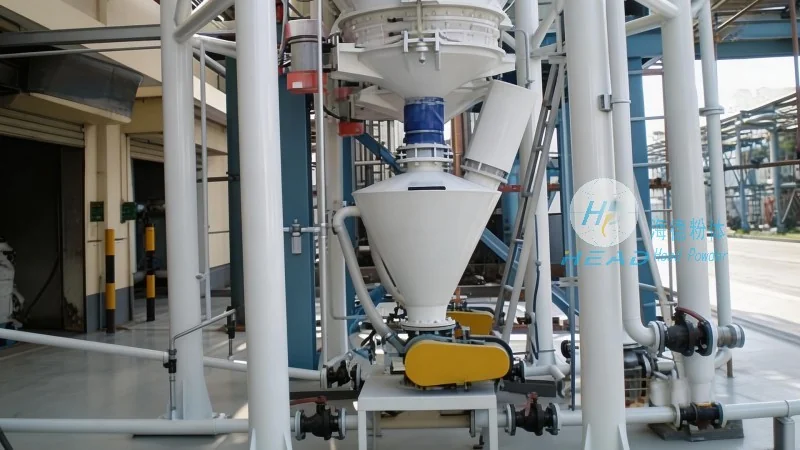
By combining advanced materials science with sophisticated design techniques, HeadPowder ensures that its PUR pneumatic conveyors deliver superior performance and durability. The use of high-quality polyurethane in the pipeline construction provides excellent resistance to abrasion, impact, and chemical exposure, making the equipment suitable for a wide range of industrial applications. The company's focus on quality control and rigorous testing ensures that each product meets or exceeds industry standards, providing customers with reliable and long-lasting solutions.
HeadPowder Engineering Co., Ltd. is dedicated to providing comprehensive support to its clients, from initial consultation and system design to installation and after-sales service. The company's team of experts is available to assist with material selection, system configuration, and troubleshooting, ensuring that clients can maximize the benefits of their PUR pneumatic conveying equipment. With a strong presence in the Chinese market and growing international recognition, HeadPowder continues to lead the way in the development of advanced material handling technologies.