

Design of a Sulfur Powder Pneumatic Conveying System
For industrial applications requiring the efficient and reliable transport of sulfur powder, specialized pneumatic conveying systems are essential. The design of such equipment involves careful consideration of material properties, operational requirements, and system integration to ensure optimal performance and safety. This article provides an overview of the key components and design principles behind sulfur powder pneumatic conveying systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in developing tailored solutions for diverse industrial needs.
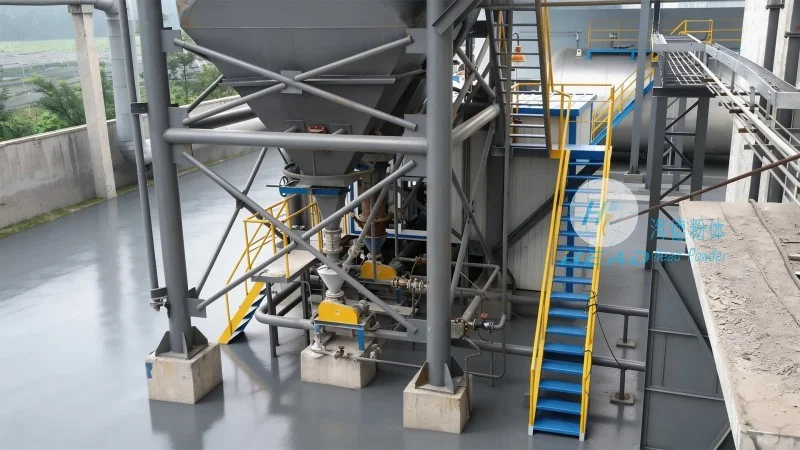
Key Design Considerations for Sulfur Powder Conveying
The successful design of a sulfur powder pneumatic conveying system begins with a thorough analysis of the material characteristics. Sulfur powder, being a fine, non-Newtonian powder, presents unique challenges in terms of flowability, dust generation, and potential for agglomeration. Engineers at HeadPowder, the company’s brand, address these challenges by selecting appropriate air velocities, conveying line configurations, and material handling components. The system design typically includes a feed hopper, a rotary valve for controlled material discharge, and a conveying pipeline that may incorporate bends, expansions, or specialized sections to accommodate the powder’s behavior. Additionally, the selection of appropriate air filtration and dust collection systems is critical to maintain environmental compliance and ensure operator safety.
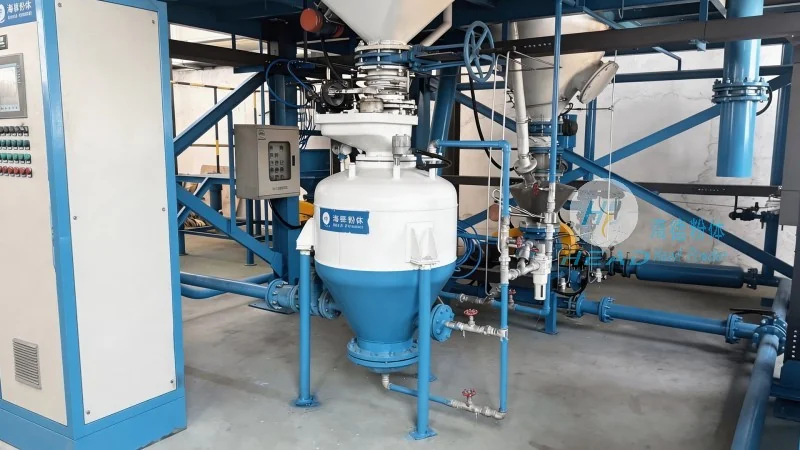
Components and Technology in Sulfur Powder Pneumatic Conveying
HeadPowder’s sulfur powder pneumatic conveying systems incorporate a range of advanced components to ensure reliable operation. The feed system, which may include a hopper with a level indicator and a rotary airlock valve, ensures consistent material feeding and prevents blockages. The conveying pipeline is constructed from materials resistant to sulfur’s corrosive properties, such as stainless steel or specialized coatings, to extend the system’s lifespan. Air compressors and control valves regulate the air flow, while pressure sensors and flow meters monitor system performance in real-time. The system may also include a receiver tank at the discharge end, equipped with a discharge valve to control material release, and a dust collection unit to capture any particles that escape the conveying line.
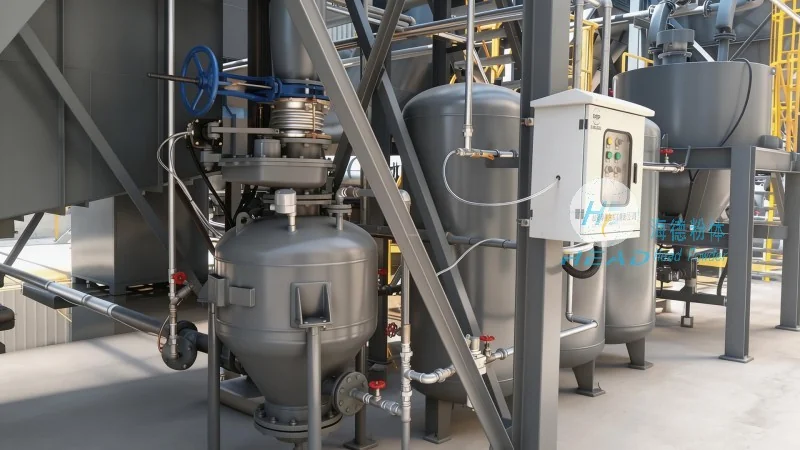
Application and Performance of Sulfur Powder Conveying Systems
These pneumatic conveying systems are widely used in industries such as chemical manufacturing, fertilizer production, and sulfur processing. The ability to transport sulfur powder over long distances with minimal loss and contamination makes the system ideal for large-scale operations. HeadPowder’s designs are tailored to meet specific client requirements, including varying conveyor capacities, distances, and environmental standards. The systems are engineered to operate efficiently, with low energy consumption and minimal maintenance requirements, ensuring cost-effective operation for industrial clients. By integrating advanced control systems and monitoring technologies, the equipment provides operators with real-time data on system performance, enabling proactive maintenance and optimizing operational efficiency.
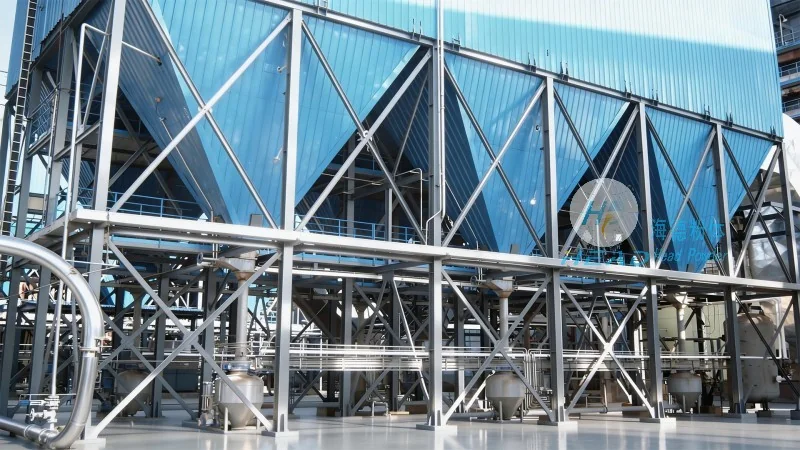
Company Background and Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer of pneumatic conveying equipment in China. With a focus on innovation and customer-centric solutions, the company has developed extensive expertise in designing and manufacturing systems for handling various powders, including sulfur. HeadPowder’s team of engineers and technicians brings years of experience in material handling and process engineering, ensuring that each system is customized to meet the unique needs of the client. The company’s facilities in Shandong, China, are equipped with state-of-the-art manufacturing equipment and quality control processes, guaranteeing the reliability and durability of their products. HeadPowder’s commitment to quality and customer satisfaction has established it as a trusted partner in the industrial equipment sector, providing clients with efficient and reliable sulfur powder conveying solutions.