

What is Gray Bin Powder Conveying? And What Are Its Design Principles?
Gray bin powder conveying is a specialized industrial method for transporting bulk powder materials efficiently. It centers on the use of a gray bin—a large storage container—as the primary vessel to hold the powder, with a system of pipes, valves, and other components facilitating its movement from the bin to processing equipment or other destinations. The design of such systems is critical, as it directly impacts the reliability, safety, and overall performance of powder handling operations across various industries, including pharmaceuticals, food processing, and chemical manufacturing.
Key Components and Their Functions
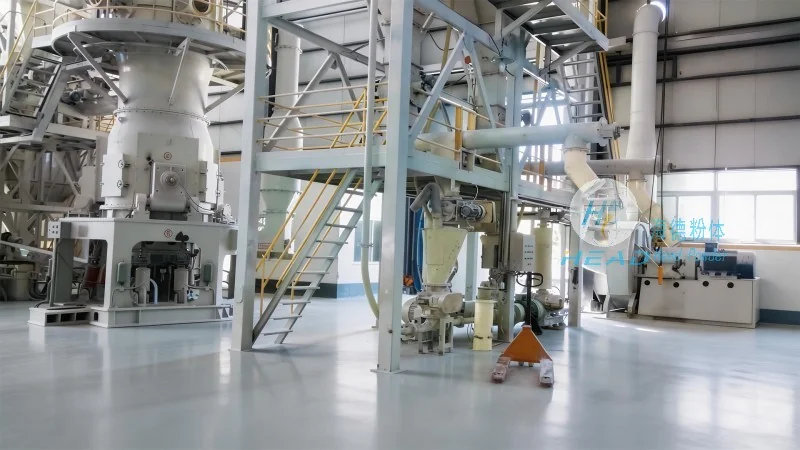
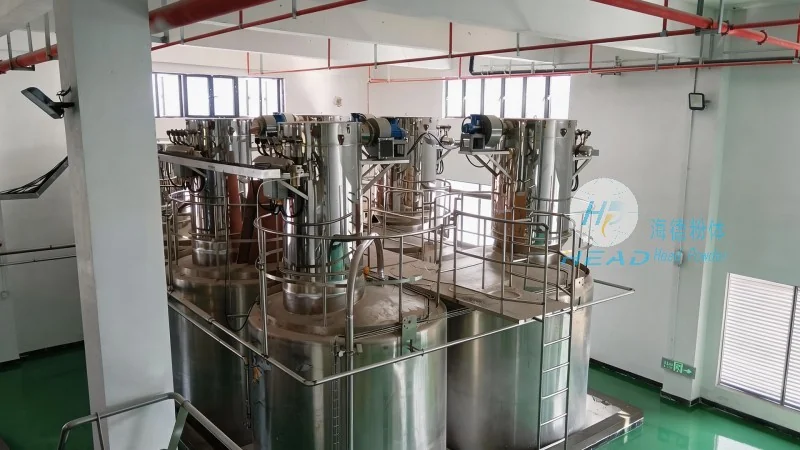
The effectiveness of gray bin powder conveying systems relies on several essential components that work together to ensure smooth operation. The gray bin itself is engineered to withstand the physical and chemical properties of the powder, constructed from materials like stainless steel or high-density polyethylene to resist corrosion and wear. The conveying line, typically made of durable materials, serves as the pathway for the powder, connecting the bin to downstream equipment. This line may include bends, elbows, and straight sections, all designed to maintain consistent flow and minimize pressure losses. Valves, such as rotary air locks (rotary valves) or gate valves, are integral to controlling the flow of powder, preventing backflow, and regulating discharge rates. Additionally, a dust collection system may be incorporated to capture airborne particles, ensuring a clean and safe working environment while complying with regulatory standards.
Design Principles for Optimal Performance
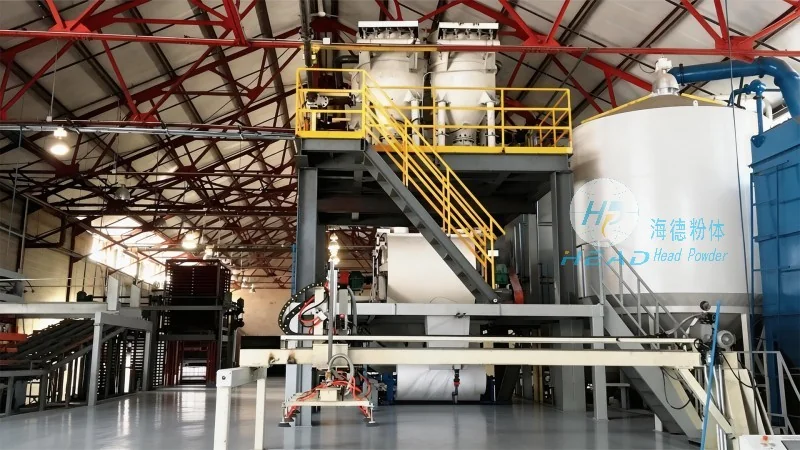
The design of gray bin powder conveying systems is guided by several fundamental principles that prioritize efficiency, safety, and adaptability. First, the system must be tailored to the specific characteristics of the powder, including its density, flowability (e.g., angle of repose), and moisture content. This customization is vital to prevent issues like bridging, caking, or blockages, which can disrupt operation and lead to material loss. Second, the design emphasizes maintaining consistent pressure and flow rates throughout the system. This is achieved through pressure regulators, flow meters, and control mechanisms that adjust parameters in real-time, ensuring smooth and uninterrupted conveying. Third, safety is a paramount consideration, with designs incorporating measures to prevent dust explosions, such as explosion-proof components and proper ventilation systems. Compliance with industry standards, including those from organizations like the American Society of Mechanical Engineers (ASME) and the National Fire Protection Association (NFPA), is also a critical aspect of the design process.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of advanced powder handling solutions. With a strong commitment to innovation and quality, the company specializes in the design, manufacturing, and implementation of gray bin powder conveying systems. HeadPowder’s expertise stems from decades of experience in understanding the unique challenges faced by industries relying on bulk powder transport. The company’s team of engineers and technicians works closely with clients to develop customized solutions that enhance operational efficiency, reduce downtime, and improve safety. HeadPowder’s products are known for their durability, reliability, and adherence to international standards, making them a trusted choice for businesses seeking dependable powder conveying systems. The company’s headquarters are located in Shandong, China, where it continues to lead the industry in providing cutting-edge solutions for powder handling needs.