

What is PCTFE Material Handling Equipment? And What Are Its Design Principles?
When considering material handling solutions for industries that demand exceptional chemical resistance and low friction, PCTFE (Polychlorotrifluoroethylene) material handling equipment stands out as a reliable and efficient choice. This specialized equipment is engineered to transport and process materials under harsh conditions, offering a robust approach to material management. The design principles behind PCTFE equipment are centered on the unique properties of the PCTFE polymer, which provides superior resistance to chemicals, high temperatures, and mechanical stress, making it ideal for challenging applications.
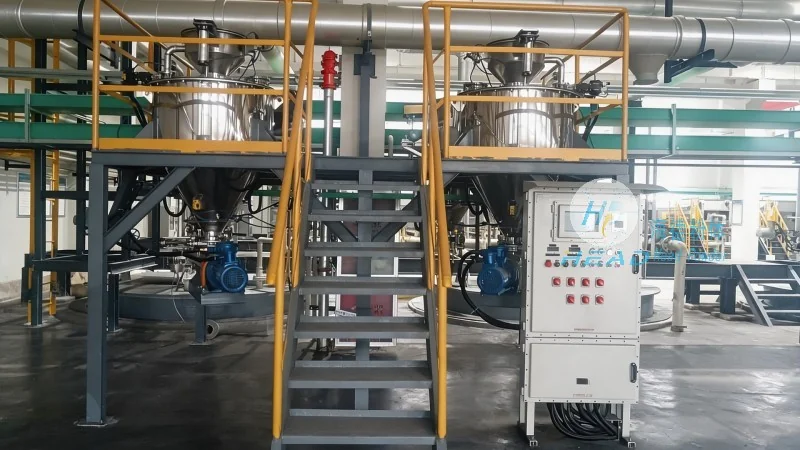
Introduction to PCTFE Material Handling Equipment
PCTFE material handling equipment is specifically designed for applications where conventional materials would be inadequate. The polymer's inherent chemical inertness allows it to handle aggressive chemicals, solvents, and other corrosive substances without degradation. Additionally, its low coefficient of friction ensures smooth material flow, reducing wear on both the equipment and the materials being transported. This combination of properties makes PCTFE equipment a preferred solution in industries such as pharmaceuticals, semiconductor manufacturing, and chemical processing, where material integrity and process efficiency are critical.
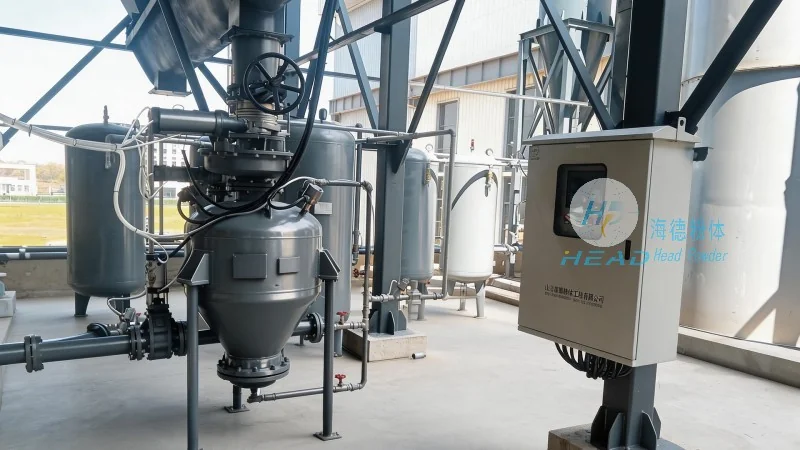
The Core Design Principles of PCTFE Equipment
The design of PCTFE material handling equipment is guided by several key principles that ensure optimal performance and longevity. First, the equipment is constructed from PCTFE, which offers unmatched chemical resistance, preventing degradation when exposed to harsh environments. Second, the design incorporates smooth, non-porous surfaces to minimize material adhesion and facilitate easy cleaning, which is essential in industries where hygiene and contamination control are paramount. Third, the equipment is engineered for low friction, allowing materials to move efficiently with minimal energy consumption. Fourth, the structural design prioritizes durability, with reinforced components to withstand high pressures and mechanical stresses. These principles collectively contribute to the reliability and efficiency of PCTFE material handling systems, ensuring they can operate continuously in demanding conditions.
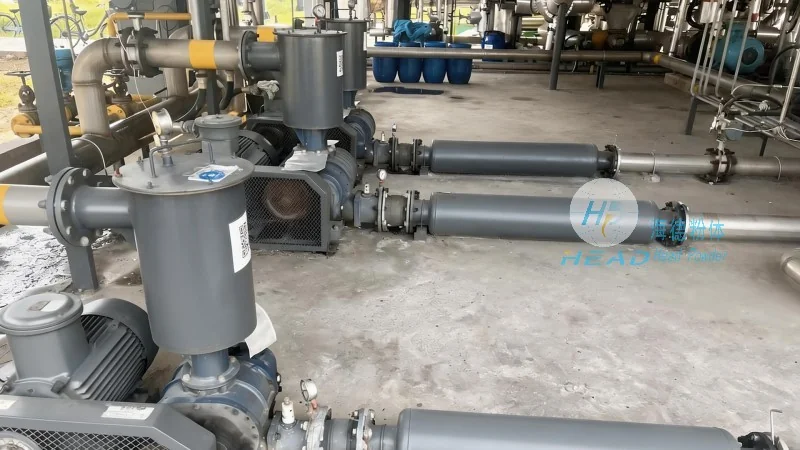
Applications of PCTFE Material Handling Equipment
PCTFE material handling equipment is widely utilized in various industrial applications. In the pharmaceutical industry, it is used to handle active pharmaceutical ingredients (APIs) and other sensitive materials that require sterile and chemically inert conditions, ensuring product purity and safety. In semiconductor manufacturing, PCTFE equipment is employed to transport wafers and other delicate components, protecting them from contamination and maintaining precise handling. In chemical processing, it is used to handle corrosive chemicals and hazardous materials, providing a safe and effective means of material transport. The versatility of PCTFE equipment makes it suitable for a broad range of applications where traditional materials are insufficient, and the need for reliable material handling is critical.
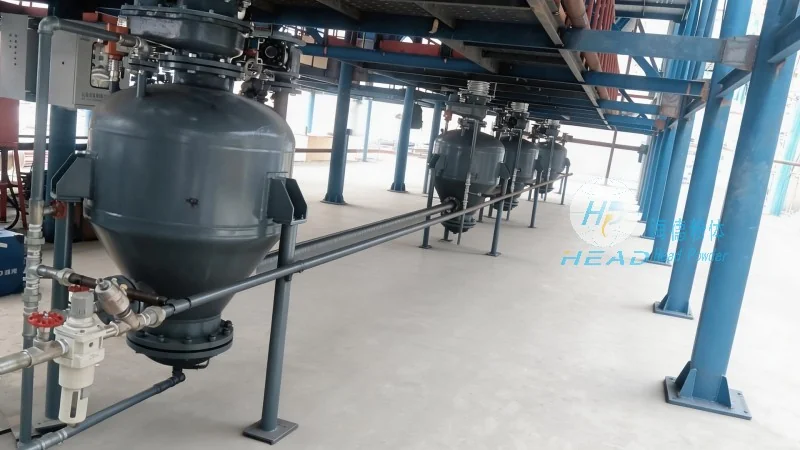
Advantages of PCTFE Material Handling Equipment
There are several distinct advantages to using PCTFE material handling equipment. First, its chemical resistance allows it to handle a wide range of materials without degradation, reducing the need for frequent equipment replacement and lowering long-term costs. Second, the low friction properties result in energy savings and reduced wear on components, leading to lower maintenance expenses and extended equipment lifespan. Third, the equipment is easy to clean and maintain, which is crucial in industries where strict hygiene standards must be met, such as food processing and pharmaceutical manufacturing. Fourth, PCTFE equipment offers long-term durability, with a service life that can exceed that of conventional materials, making it a cost-effective investment for businesses operating in demanding environments. These advantages make PCTFE equipment a top choice for manufacturers seeking to enhance operational efficiency and maintain high standards of quality and safety.