

What is a dilute phase material conveying line? What are its design principles?
A dilute phase material conveying line is a sophisticated system engineered to transport bulk materials in a low concentration state, typically suspended in a gas stream. This method is widely adopted in industries such as mining, chemical processing, and food production due to its efficiency in handling fine powders and granules over long distances. The core of this technology lies in the design principles that ensure optimal performance, reliability, and energy efficiency.
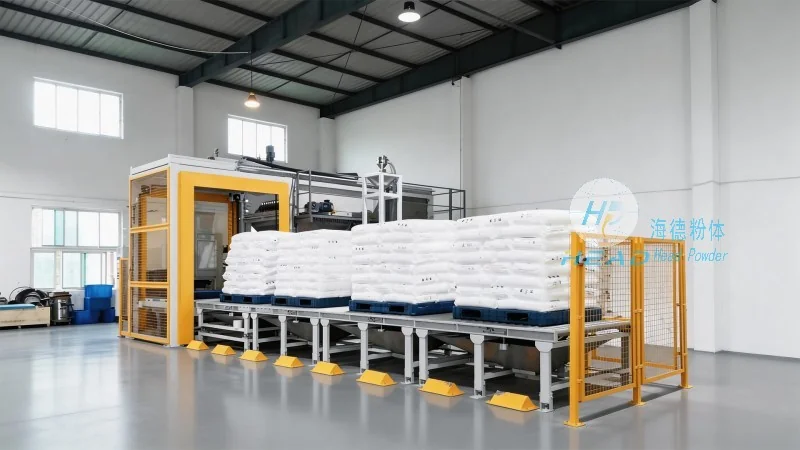
Key Design Principles of Dilute Phase Conveying Systems
The design of a dilute phase material conveying line involves several critical principles that work in concert to achieve effective material transport. First, the system must maintain a consistent gas velocity to keep the material particles suspended, preventing settling or blockages. This is typically achieved through the use of positive pressure or vacuum systems, depending on the application requirements. Second, the selection of appropriate pipe diameters and gas flow rates is crucial. Larger diameters reduce pressure drop and energy consumption, while maintaining sufficient velocity to keep particles airborne. Third, the incorporation of specialized components like cyclones, separators, and control valves ensures that the material is efficiently separated from the gas stream at the destination, minimizing dust emissions and optimizing material recovery.
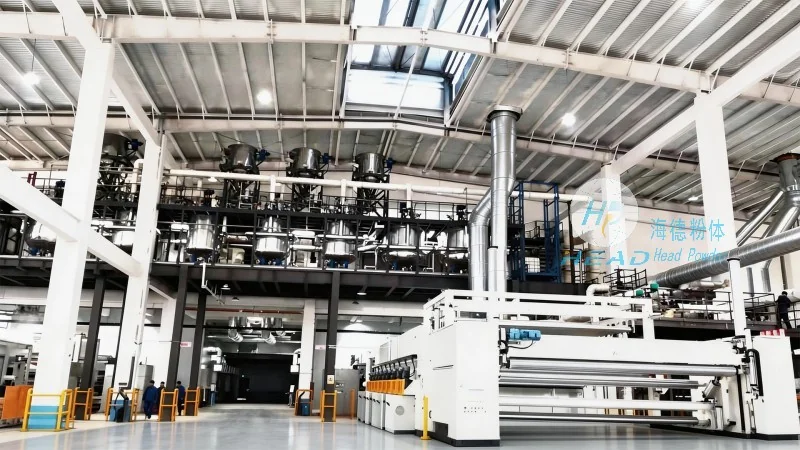
How Dilute Phase Conveying Enhances Material Handling Efficiency
Compared to dense phase or pneumatic conveying methods, dilute phase systems offer distinct advantages in terms of throughput and energy usage. By maintaining a low particle concentration, these lines can handle high volumes of material with lower operational pressures, reducing the risk of system failures and maintenance costs. Additionally, the design allows for flexible routing, enabling the integration of multiple transfer points and complex layouts without compromising performance. The technology also supports the transportation of materials with varying particle sizes and moisture content, making it versatile for diverse industrial applications.
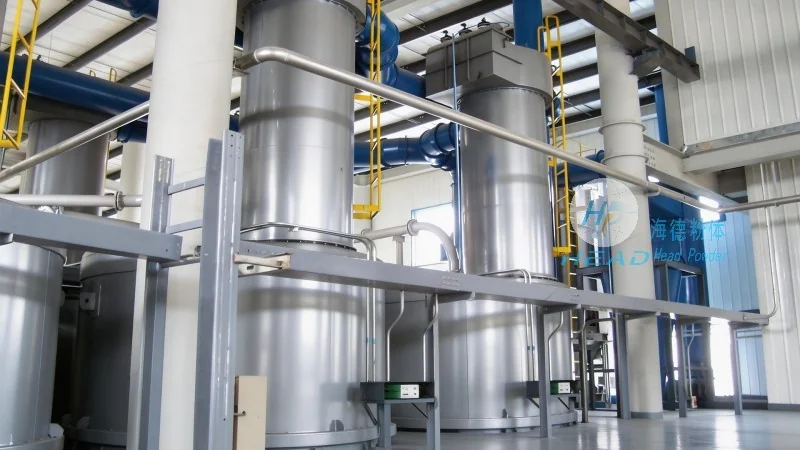
HeadPowder Engineering: Your Partner in Dilute Phase Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, manufacturing, and installation of dilute phase material conveying systems. With years of experience in the industry, HeadPowder has developed a comprehensive range of products tailored to meet the specific needs of clients across various sectors. The company’s commitment to quality and innovation ensures that each system is engineered to deliver reliable performance and long-term durability.
Customized Solutions for Diverse Industrial Needs
HeadPowder understands that every industrial operation has unique material handling requirements. Therefore, the company offers customized solutions that incorporate advanced design principles and cutting-edge technology. From initial consultation and system design to installation and after-sales support, HeadPowder provides end-to-end services to ensure client satisfaction. The company’s team of experts works closely with clients to assess their specific needs, recommend optimal solutions, and implement systems that enhance operational efficiency and reduce costs.
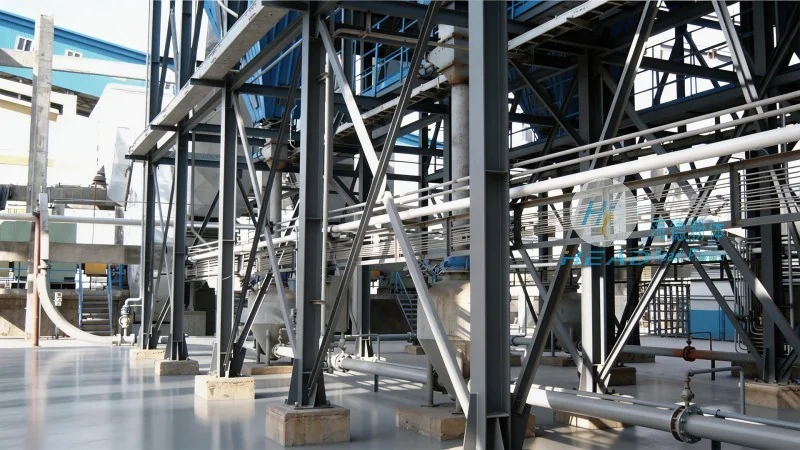
Ensuring Reliability and Longevity in Dilute Phase Systems
Reliability is a top priority for HeadPowder when designing dilute phase material conveying lines. The company employs rigorous quality control measures and uses high-quality materials to construct components that can withstand the demands of continuous operation. Regular maintenance and monitoring are also integral to the system’s longevity, ensuring that the equipment remains in optimal condition and minimizes downtime. HeadPowder’s dedication to customer support extends beyond the initial installation, with ongoing services that help clients maximize the performance and lifespan of their conveying systems.