

Working Principle and Features of Silicate Powder Handling Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design and manufacturing of advanced powder handling solutions. The company's focus is on providing reliable and efficient systems for transporting silicate powders, which are widely used in various industrial applications such as ceramics, construction materials, and chemical processing. This article will explore the working principle and key features of their silicate powder transport systems, highlighting how they address the unique challenges of handling these materials.
The Working Principle of Silicate Powder Conveying Systems
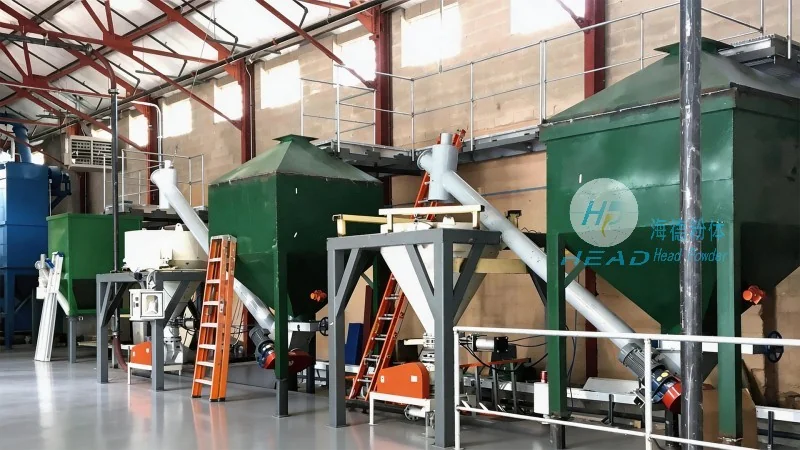
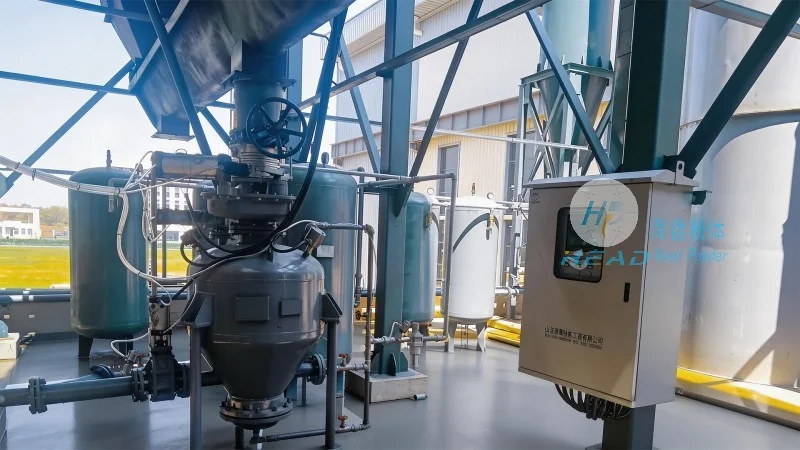
The silicate powder handling system operates on a principle of controlled material flow, ensuring consistent and safe transportation from the source to the destination. The system typically includes several core components: a feeding mechanism, a conveying device, and a control unit. The feeding mechanism, often a hopper or a rotary valve, regulates the flow of silicate powder into the system, preventing overfilling and maintaining a steady feed rate. This is crucial for preventing material bridging or clogging, which are common issues with cohesive powders like silicates. The conveying device, such as a screw conveyor, pneumatic conveyor, or a combination of both, then transports the powder through a pipeline or a series of connected sections. The control unit monitors parameters like pressure, flow rate, and temperature, adjusting the system's operation in real-time to maintain optimal performance. For example, in a screw conveyor system, the rotating screw pushes the powder forward, while the speed of the screw can be adjusted to control the flow rate. In pneumatic systems, compressed air propels the powder through the pipeline, with the air pressure and flow rate managed by the control unit to ensure smooth transport. The system is designed to handle different types of silicate powders, including fine powders that are prone to dust generation and larger particles that require more force to move. By integrating these components, the system ensures a continuous and efficient flow of material, minimizing downtime and maximizing productivity.
Key Features of Silicate Powder Transport Systems
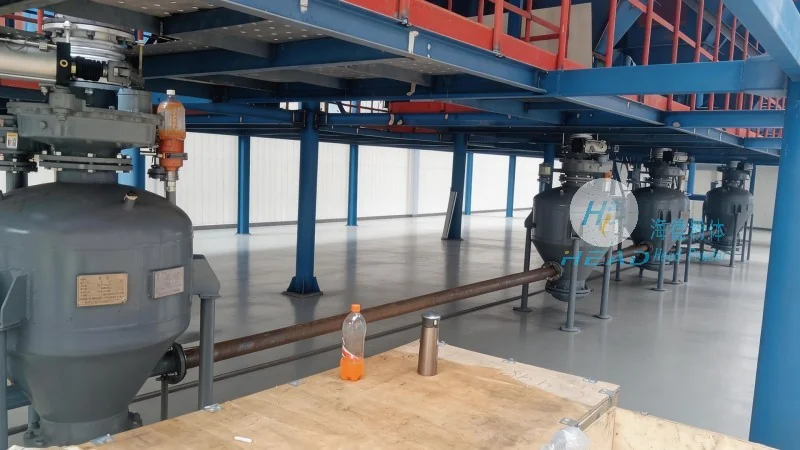
HeadPowder's silicate powder handling systems are characterized by several key features that enhance their performance and reliability. One of the primary features is the robust design, which is built to withstand the abrasive nature of silicate powders and the harsh operating conditions often encountered in industrial environments. The materials used for the components, such as stainless steel or high-grade alloys, are resistant to corrosion and wear, ensuring a long service life. Another important feature is the advanced control technology, which allows for precise regulation of the system's operation. The control unit uses sensors to monitor critical parameters, such as pressure, temperature, and flow rate, and adjusts the system's settings automatically to maintain optimal conditions. This not only improves efficiency but also reduces the risk of material degradation or equipment damage. The system also incorporates safety features, such as emergency stop buttons and overload protection, to prevent accidents and ensure the safety of operators. Additionally, the modular design of the system allows for easy customization and expansion, enabling it to adapt to different production requirements. For instance, the system can be configured with additional feeding or conveying sections to handle higher volumes of powder, or with special filters to reduce dust emissions. The compact design of the system also saves space in the production facility, making it suitable for both small and large-scale operations. Furthermore, the system is designed for easy maintenance, with accessible components that can be quickly inspected and replaced. This reduces downtime and maintenance costs, contributing to the overall cost-effectiveness of the system. The integration of these features makes the silicate powder handling system a reliable and efficient solution for industries that rely on consistent and safe transportation of silicate powders.
Applications and Benefits
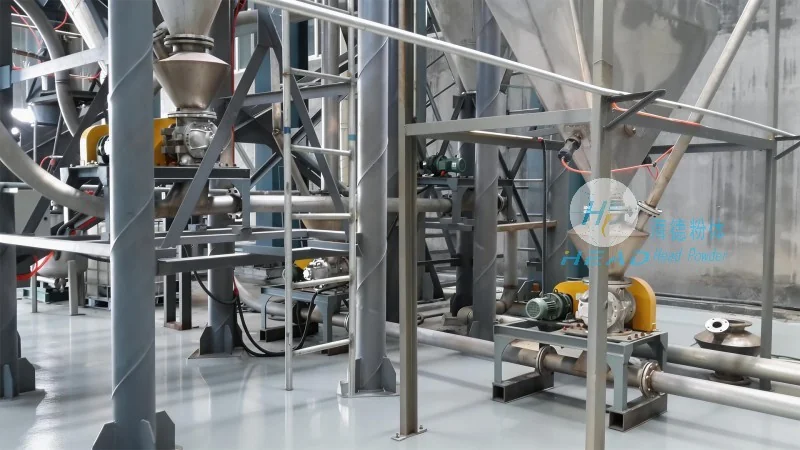
The silicate powder handling systems from Shandong HeadPowder Engineering Co., Ltd. are widely used in various industries due to their versatility and effectiveness. In the ceramics industry, the system is used to transport raw materials like clay and feldspar, which are essential for manufacturing tiles, bricks, and other ceramic products. The consistent flow of these materials ensures uniform product quality and reduces waste. In the construction industry, the system handles cement and other building materials, facilitating their transport to construction sites. The ability to handle large volumes of powder efficiently helps in meeting the high demand for construction materials. In the chemical industry, the system transports silicate-based chemicals, which are used in the production of various products such as detergents and coatings. The system's ability to handle fine powders and control dust emissions is particularly beneficial in this industry. The benefits of using these systems extend beyond efficiency and reliability. The reduced risk of material clogging and bridging minimizes production downtime, leading to higher productivity. The improved safety features protect operators from potential hazards, creating a safer working environment. The modular design allows for scalability, enabling companies to upgrade their systems as their production needs grow. The long service life of the components reduces replacement costs, contributing to lower overall operating expenses. Overall, the silicate powder handling systems from HeadPowder provide a comprehensive solution for industries that require reliable and efficient transportation of silicate powders, enhancing their operational performance and profitability.