

Working Principle and Features of Cement Raw Material Powder Conveying Systems
Cement raw material powder conveying systems are critical components in the cement production process, responsible for efficiently transporting bulk powders such as limestone, clay, and iron ore from storage silos to the grinding and processing units. The effectiveness of these systems directly impacts production efficiency, material handling costs, and overall plant performance. Understanding the working principles and key features of such systems is essential for optimizing cement manufacturing operations.
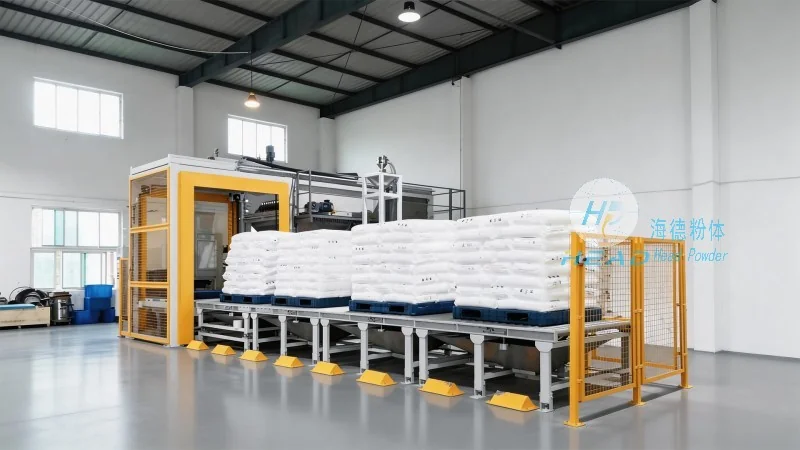
The Working Principle of Cement Raw Material Powder Conveying Systems
HeadPowder's cement raw material powder conveying systems typically operate based on pneumatic or mechanical conveying technologies. The most common pneumatic systems use positive pressure or negative pressure to move powders through pipelines. In positive pressure systems, a fan or blower generates compressed air that propels the material forward. The air and material mixture travels through the pipeline, with the material being separated from the air at the destination point, often via a cyclone separator or a filter. Mechanical systems, on the other hand, utilize screw conveyors, belt conveyors, or bucket elevators to physically move the material. These systems are particularly suitable for handling materials with higher moisture content or larger particle sizes.
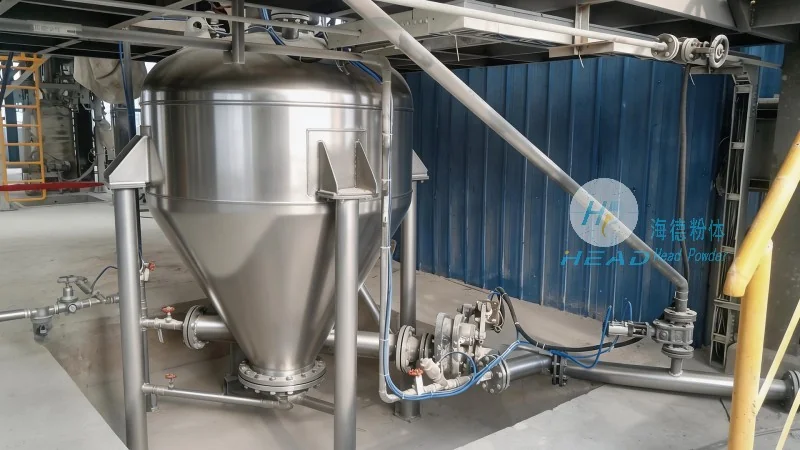
Key Features of Cement Raw Material Powder Conveying Systems
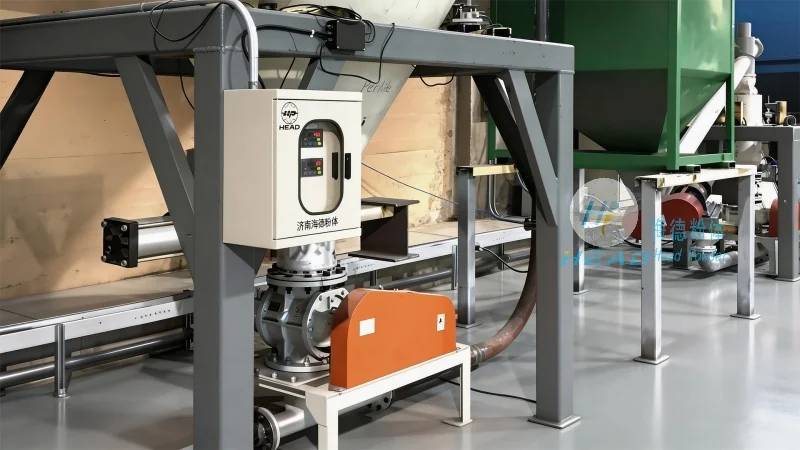
HeadPowder's conveying systems are designed with several key features to ensure reliable and efficient operation. Firstly, they offer high conveying capacity, capable of handling large volumes of raw materials at a consistent rate, which is crucial for maintaining steady production in cement plants. Secondly, the systems are engineered for minimal material degradation, using gentle handling mechanisms to preserve the quality of the raw materials, which is vital for achieving the desired cement quality. Thirdly, the equipment is built for durability and low maintenance, with robust components that can withstand the abrasive nature of cement raw materials, reducing downtime and operational costs. Additionally, the systems are equipped with advanced control systems that allow for precise flow regulation and monitoring, ensuring optimal performance and safety. The modular design of these systems also facilitates easy installation and integration into existing cement production lines, providing flexibility for plant expansions or upgrades.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as a leading provider of cement raw material powder conveying solutions, is committed to delivering high-quality, reliable equipment tailored to the specific needs of cement manufacturers. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the cement industry. HeadPowder's systems are designed and manufactured in China, with the company's headquarters located in Shandong, providing local support and expertise to clients worldwide. The company adheres to international standards and continuously invests in research and development to enhance the performance and efficiency of its conveying systems, ensuring they meet the evolving demands of the cement production sector.