

Working Principle and Features of Soap Granule Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier based in Shandong, China. The company specializes in the research, development, and production of advanced powder conveying systems, particularly those designed for handling soap granules. This article provides an in-depth exploration of the working principle and key features of the soap granule powder conveying system equipment offered by headpowder.
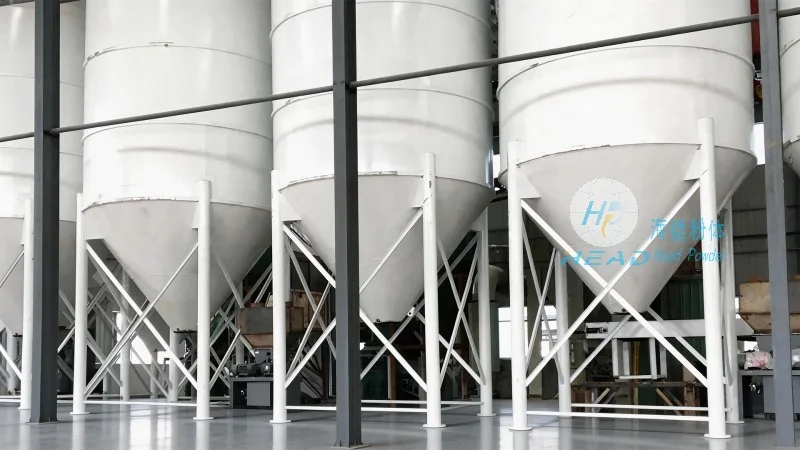
Working Principle of the Soap Granule Powder Conveying System
The soap granule powder conveying system is engineered to efficiently transport soap granules from storage silos or bulk containers to processing lines or packaging stations. The system typically comprises several core components, including a hopper, a conveyor mechanism (such as a screw conveyor or pneumatic conveyor), a control panel, and a dust collection system. The process begins when soap granules are fed into the hopper. From there, the granules are transferred to the conveyor, which moves them through the system under controlled conditions. The control panel allows operators to adjust parameters like speed and pressure to optimize the conveying process. A dust collection system is integrated to ensure a clean and safe working environment by capturing any airborne particles during the transfer.
Key Features of the Soap Granule Powder Conveying System
The soap granule powder conveying system from headpowder is designed with several notable features that enhance its performance and reliability. Firstly, it offers high conveying efficiency, ensuring that soap granules are moved quickly and consistently without significant loss or degradation. The system is also built for durability, using high-quality materials that can withstand the abrasive nature of soap granules and the demands of continuous operation. Another key feature is its adaptability, as it can be customized to accommodate different granule sizes and throughput requirements. The control panel provides real-time monitoring and adjustment capabilities, allowing for precise management of the conveying process. Additionally, the system incorporates safety features, such as overload protection and emergency stop buttons, to ensure operational safety. The integration of a dust collection system not only maintains a clean environment but also helps in complying with environmental regulations by reducing dust emissions.
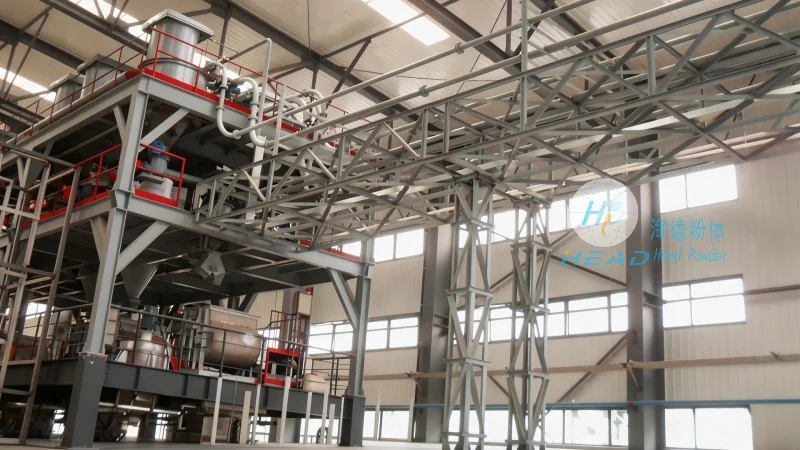
Benefits of Using the Soap Granule Powder Conveying System
Implementing the soap granule powder conveying system from headpowder brings several benefits to industrial operations. The primary advantage is improved operational efficiency, as the system minimizes downtime and maximizes throughput. By automating the powder transfer process, it reduces the need for manual handling, which in turn lowers labor costs and the risk of human error. The system also enhances product quality by preventing contamination and ensuring consistent particle size distribution. Furthermore, the durability and reliability of the equipment contribute to long-term cost savings, as it requires less maintenance and has a longer service life compared to traditional conveying methods. The adaptability of the system allows it to be integrated into existing production lines without major modifications, making it a flexible solution for various industrial applications.
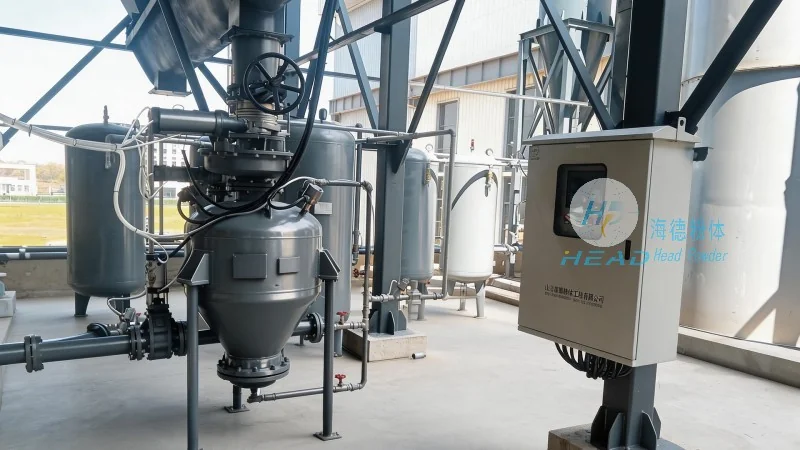
Application Scenarios
The soap granule powder conveying system is widely used in industries that require the handling of soap granules, such as the soap manufacturing, detergent production, and personal care product sectors. In these applications, the system is crucial for maintaining a smooth production flow, from raw material storage to final product packaging. The system's ability to handle large volumes of soap granules efficiently makes it ideal for high-capacity production lines. Additionally, its integration with other processing equipment, such as mixers and reactors, allows for seamless operation, ensuring that the soap granules are transferred without any interruption in the production cycle.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides a robust and efficient soap granule powder conveying system that combines advanced technology with practical design. The system's working principle, which involves controlled feeding, conveying, and dust management, ensures reliable and safe operation. Its key features, including high efficiency, durability, adaptability, and safety, make it a superior choice for industries dealing with soap granules. By leveraging this equipment, businesses can enhance their production processes, reduce costs, and improve overall operational performance. As a leading manufacturer based in Shandong, China, headpowder continues to innovate and provide solutions that meet the evolving needs of the powder handling industry.