

Working Principle and Features of Glucose Powder Pneumatic Conveying Systems
Glucose powder pneumatic conveying systems are advanced industrial equipment designed to efficiently transport granular or powdered materials, such as glucose, through a pipeline using air or gas as the conveying medium. These systems are widely used in the food, pharmaceutical, and chemical industries due to their ability to handle sensitive materials while maintaining high levels of hygiene and efficiency.
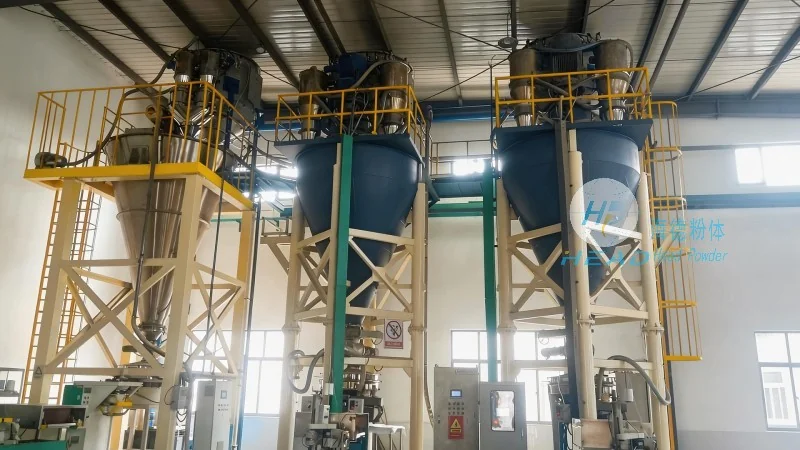
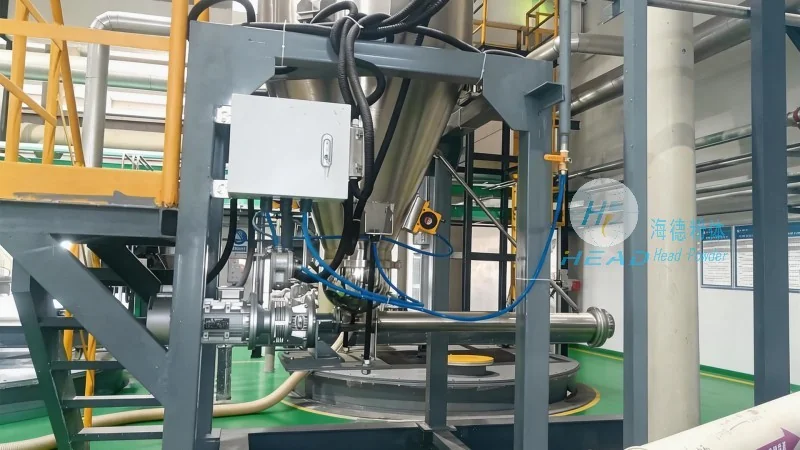
Working Principle of Glucose Powder Pneumatic Conveying Systems
The core working principle of a glucose powder pneumatic conveying system involves the use of a pressure or vacuum source to move the powder through a pipeline. In a typical pressure system, compressed air is introduced into the material hopper, creating a pressure differential that propels the powder forward. The system typically includes components like a feeder, a conveying line, a receiver, and a filter system. The feeder controls the flow rate of the glucose powder, while the conveying line transports it from the source to the destination. The receiver collects the material, and the filter system ensures that any fine particles or dust are captured, preventing contamination and maintaining air quality.
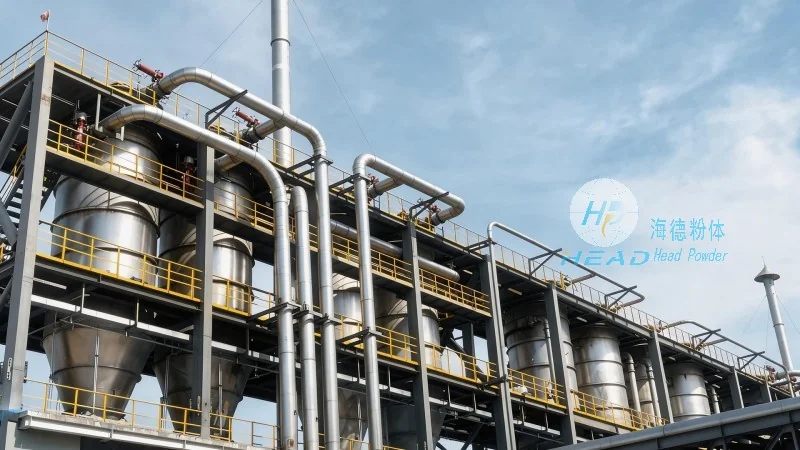
Key Features of Glucose Powder Pneumatic Conveying Systems
Several key features make glucose powder pneumatic conveying systems ideal for handling glucose and similar materials. First, they offer a closed system, which is crucial for maintaining product purity and preventing contamination from external sources. This is particularly important in the food and pharmaceutical industries where product quality and safety are paramount. Second, these systems provide high conveying efficiency, allowing for the transport of large quantities of material over long distances with minimal energy consumption. Third, they are highly flexible, capable of handling various particle sizes and shapes, including fine powders like glucose. Fourth, the systems are easy to clean and maintain, with components that can be disassembled for thorough sanitation, ensuring compliance with industry regulations. Finally, they offer a compact design, saving space in industrial facilities and making them suitable for both new installations and retrofitting existing processes.
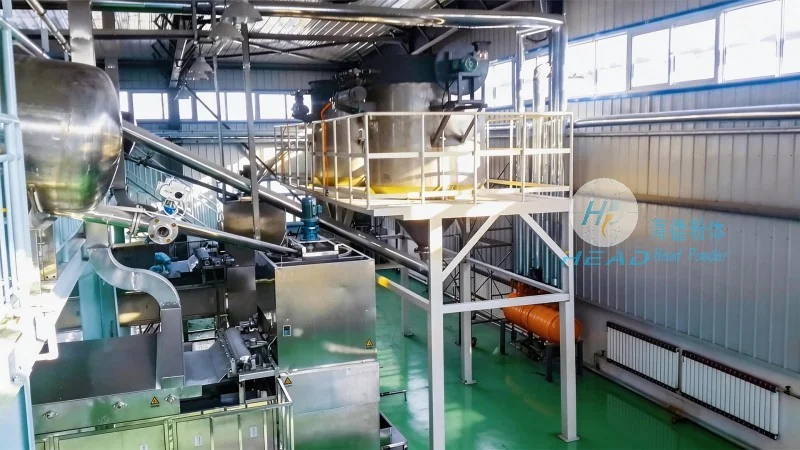
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Headpowder, the manufacturer of these advanced conveying systems, is a leading company based in Shandong, China. With years of experience in the engineering and manufacturing of pneumatic conveying equipment, Headpowder specializes in providing customized solutions tailored to the specific needs of clients in the food, pharmaceutical, and chemical sectors. The company's commitment to quality, innovation, and customer satisfaction has made it a trusted partner for businesses seeking reliable and efficient material handling solutions. Headpowder's products are designed to meet international standards and are backed by a team of skilled engineers and technicians who provide comprehensive support, from installation to maintenance, ensuring optimal performance and longevity of the equipment.