

Working Principle and Features of Industrial Alkali Powder Pneumatic Conveying Systems
Industrial alkali powder pneumatic conveying systems are critical components in modern material handling and processing industries. These systems are designed to efficiently transport alkaline powders, such as sodium hydroxide or calcium carbonate, over long distances with minimal loss and contamination. The core technology behind these systems leverages the principles of pneumatic transport, combining air flow and pressure differentials to move bulk materials. Understanding the working principle and key features of such systems is essential for optimizing industrial operations and ensuring product quality.
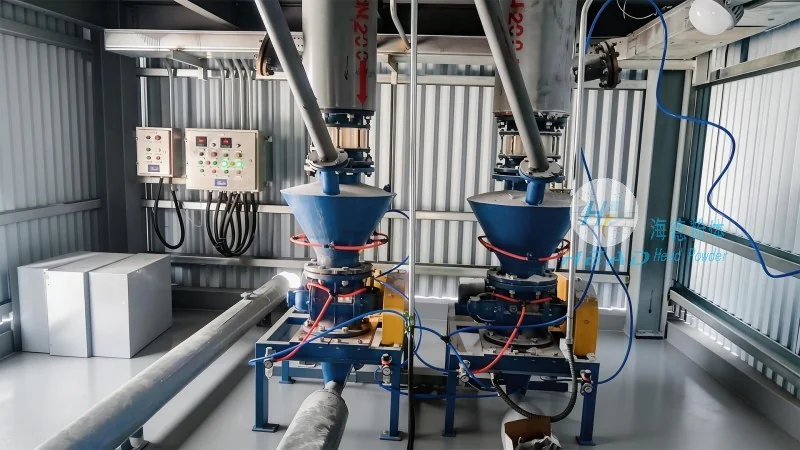
Company Introduction: HeadPowder
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced material handling solutions. Based in Shandong, China, the company specializes in designing, manufacturing, and installing pneumatic conveying systems tailored to the needs of various industrial sectors. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for businesses requiring reliable and efficient powder transport solutions.
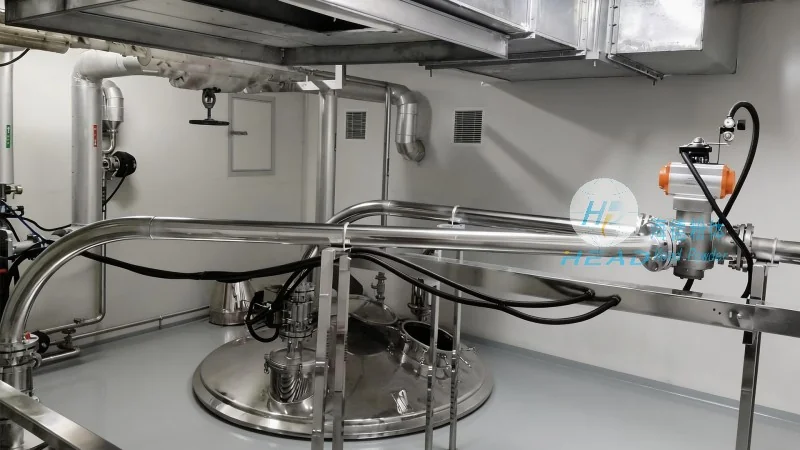
Working Principle of Industrial Alkali Powder Pneumatic Conveying Systems
The operation of industrial alkali powder pneumatic conveying systems is based on the fundamental principle of air-driven transport. The system typically consists of a hopper, a conveyor line, and a receiver. The process begins when the alkaline powder is fed into the hopper. A fan or blower then generates a high-pressure air stream, which is introduced into the conveyor line. As the air flows through the pipe, it creates a negative pressure environment that draws the powder particles into the air stream. The mixture of air and powder travels through the pipeline to the receiver, where the powder is separated from the air and collected. The air is then filtered and discharged, ensuring that no dust or particles are released into the environment. This method allows for continuous, automated transport of large quantities of alkali powders with high efficiency and minimal human intervention.
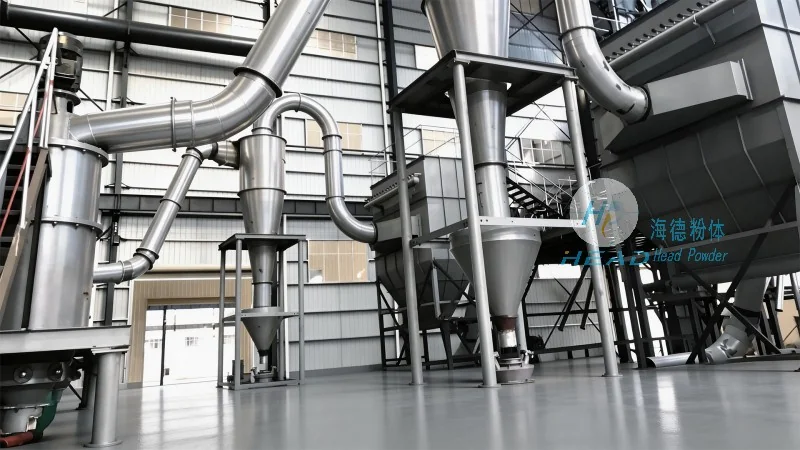
Key Features of Industrial Alkali Powder Pneumatic Conveying Systems
Industrial alkali powder pneumatic conveying systems offer several distinct advantages that make them ideal for handling sensitive and corrosive materials. One of the primary features is their ability to transport powders over long distances without the need for mechanical components like belts or buckets. This reduces wear and tear on equipment and minimizes the risk of material contamination. Additionally, these systems can handle a wide range of particle sizes and densities, making them versatile for various industrial applications. Another significant feature is the system's self-cleaning capability. As the air flows through the pipeline, it helps to prevent clogging by continuously moving the powder, which is particularly important for handling sticky or cohesive alkali powders. The systems also provide precise control over the flow rate and pressure, allowing for accurate dosing and consistent product quality. Furthermore, the enclosed design of the conveying line ensures that the alkaline powders are contained, preventing dust emissions and protecting the environment and workers from exposure to harmful substances.
Applications and Benefits in Industrial Settings
The industrial alkali powder pneumatic conveying systems manufactured by HeadPowder are widely used in industries such as chemical manufacturing, food processing, and pharmaceuticals. In chemical plants, these systems are crucial for transporting sodium hydroxide, which is used in the production of soaps, detergents, and other chemical products. The ability to handle corrosive materials without damage to the equipment makes the system highly suitable for such applications. In food processing, the systems ensure that alkaline powders, like calcium carbonate, are transported safely and hygienically, maintaining the quality of food products. The benefits of using these systems extend beyond efficiency and safety; they also contribute to cost savings by reducing material loss and minimizing downtime due to equipment failure. The enclosed and automated nature of the systems also enhances workplace safety by eliminating the need for manual handling of powders, which can be hazardous if not handled properly.
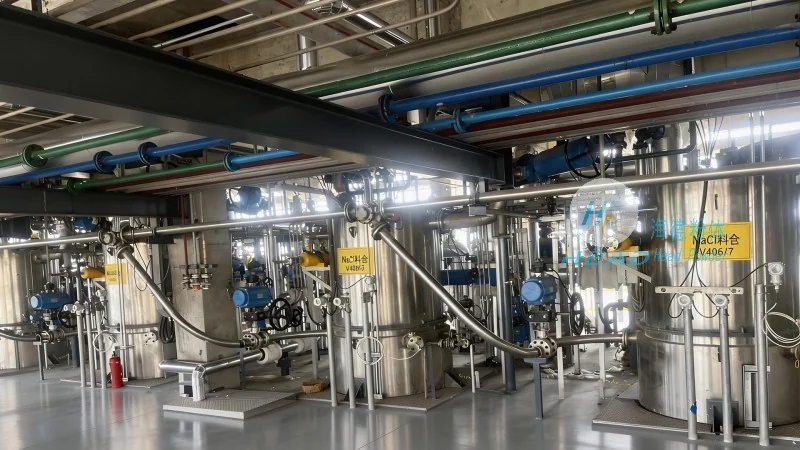
Conclusion and Company Commitment
Industrial alkali powder pneumatic conveying systems, as exemplified by those from HeadPowder, represent a sophisticated solution for the efficient and safe transport of alkaline powders in industrial settings. By understanding the working principle and leveraging the key features of these systems, businesses can optimize their material handling processes, improve product quality, and enhance operational efficiency. HeadPowder's expertise in designing and manufacturing these systems ensures that clients receive tailored solutions that meet their specific requirements, whether for large-scale production or specialized applications. With a focus on quality, innovation, and customer satisfaction, HeadPowder continues to be a leader in providing reliable material handling solutions for the global industrial community.