

Principle and Working Scene Characteristics of Heavy Calcium Pneumatic Conveying Equipment
Heavy calcium, also known as heavy calcium carbonate, is a widely used industrial material in various sectors such as plastics, coatings, and papermaking. The efficient and reliable transportation of heavy calcium powder is crucial for industrial production processes. Pneumatic conveying equipment offers an effective solution for handling these powders, ensuring smooth material flow and minimizing operational disruptions. This article delves into the principles behind heavy calcium pneumatic conveying systems and explores the typical working scenarios where such equipment is applied.
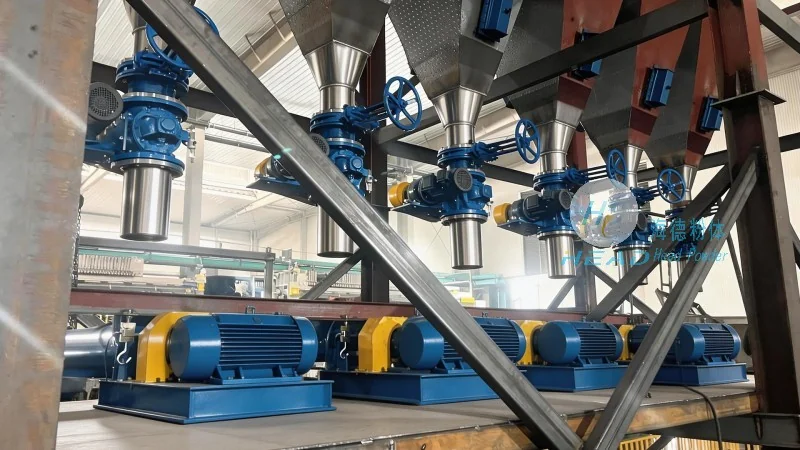
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier specializing in pneumatic conveying equipment. With a strong focus on innovation and quality, the company has established itself as a leading player in the industry. HeadPowder's products are designed to meet the specific needs of clients, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where it operates its research and development, production, and customer service facilities.
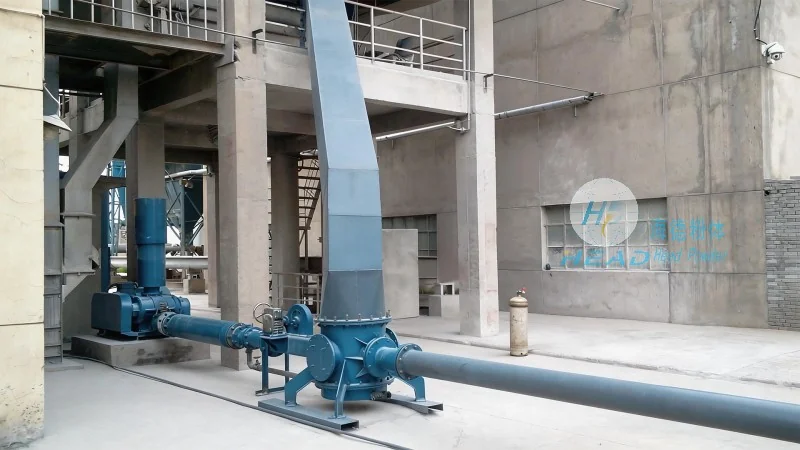
The Principle of Pneumatic Conveying for Heavy Calcium
Pneumatic conveying systems utilize air or gas to transport bulk materials like heavy calcium powder through a pipeline network. The core principle involves creating a pressure differential between the inlet and outlet of the conveying line. By injecting air at a controlled pressure, the system generates sufficient velocity to lift and move the powder particles. There are two main types of pneumatic conveying: dilute-phase and dense-phase. Dilute-phase systems operate at higher air velocities, suitable for short distances and low to medium material loads. Dense-phase systems, on the other hand, use lower air velocities and higher material concentrations, ideal for longer distances and high material loads. The choice between these systems depends on the specific application requirements and the characteristics of the heavy calcium powder being transported.
Working Scene Characteristics of Heavy Calcium Pneumatic Conveying
The application of heavy calcium pneumatic conveying equipment varies across different industrial sectors, each with its unique characteristics and requirements. In the plastics industry, for instance, these systems are used to transport heavy calcium powder from storage silos to production lines, ensuring a consistent and uninterrupted supply of raw material. The equipment's ability to handle fine powders without clogging or degradation is particularly important in this sector. In the coating industry, pneumatic conveying is employed to move heavy calcium powder from blending tanks to spray booths, maintaining the quality and consistency of the coating materials. The working scene also includes scenarios in the papermaking industry, where heavy calcium is used as a filler, and the conveying system must be capable of handling high volumes of material while preventing dust generation and ensuring environmental compliance. Additionally, in the chemical industry, these systems are used to transport heavy calcium powder in processes involving mixing and compounding, where precise control over material flow is critical for product quality.
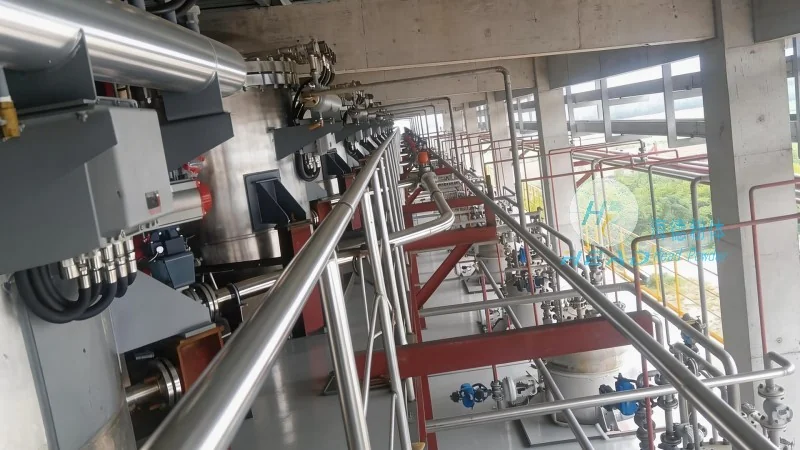
Advantages and Application Scenarios
Shandong HeadPowder Engineering Co., Ltd. provides customized pneumatic conveying solutions tailored to the specific needs of heavy calcium powder handling. The company's expertise in material flow dynamics and system design ensures that the equipment operates efficiently and reliably. The working scene characteristics, such as the need for low maintenance, high material throughput, and minimal dust generation, are all addressed in the design of the conveying systems. By leveraging advanced technology and rigorous quality control, HeadPowder's equipment delivers superior performance, contributing to increased productivity and reduced operational costs for clients. The company's commitment to customer satisfaction and technical support further enhances the value of its products, making them a preferred choice in the market.