

Principle and Working Scene Characteristics of Bulk Bag Powder Handling Systems
Bulk bag powder handling systems represent a critical technology in the modern industrial landscape, designed to efficiently transport and manage large quantities of powdered materials. These systems are essential for industries ranging from chemicals and food processing to pharmaceuticals and construction, where the reliable and safe movement of bulk materials is paramount. Understanding the underlying principles and operational characteristics of such systems is crucial for optimizing workflow and ensuring compliance with safety standards.
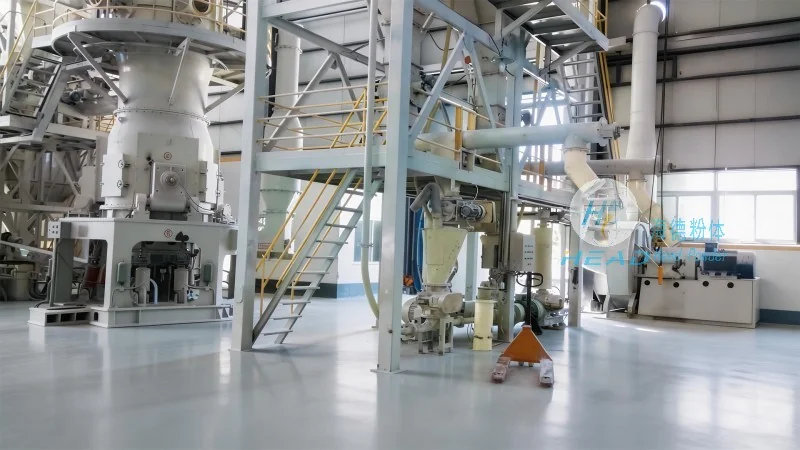
The Core Principle of Bulk Bag Powder Transport Systems
The fundamental principle of bulk bag powder handling systems revolves around the controlled movement of materials within a flexible container, commonly known as a bulk bag or super sack. These systems typically employ either vacuum or pressure-based mechanisms to draw or push the powder from the bag into a processing or storage vessel. The process begins with the bulk bag being securely placed on a discharge spout or hopper, which is integrated with the transport system. Through the application of negative pressure (vacuum) or positive pressure (compressed air or gas), the powder is extracted from the bag and directed towards the next stage of the production line. This method ensures minimal material loss and maintains the integrity of the product, which is particularly important for sensitive or high-value powders.
Key Working Scene Characteristics
One of the most notable characteristics of bulk bag powder handling systems is their adaptability to diverse operational environments. These systems are designed to handle a wide range of powder types, from fine powders like flour or cement to coarser materials such as sand or granules. The flexibility of bulk bags allows for the containment of various particle sizes and moisture levels, making them suitable for both dry and slightly moist powders. Additionally, the systems are engineered for high efficiency, capable of processing large volumes of material in a short period, which enhances production throughput. Safety is another critical characteristic, as the systems are equipped with features like dust suppression, leak prevention, and overload protection to minimize risks associated with handling powders. The modular design of these systems also facilitates easy integration into existing production lines, allowing for scalability as business needs evolve.
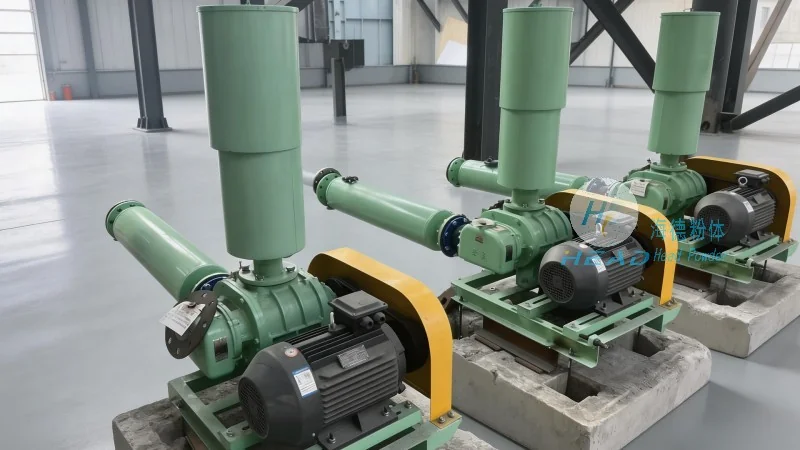
Application Scenarios and Operational Advantages
Bulk bag powder handling systems find extensive application across multiple industries, each benefiting from the unique advantages these systems offer. In the chemical industry, for instance, they are used to transport raw materials like pigments, polymers, and catalysts, ensuring precise dosing and reducing the risk of contamination. The food and beverage sector utilizes these systems for handling ingredients such as sugar, spices, and flour, maintaining hygiene standards and preventing cross-contamination. In the pharmaceutical industry, the systems are crucial for transporting active pharmaceutical ingredients (APIs) and excipients, where strict quality control and sterility are non-negotiable. The construction industry also relies on bulk bag handling systems for transporting cement, lime, and other building materials, supporting large-scale projects with consistent material supply. The operational advantages of these systems include reduced labor costs, as automated processes minimize manual handling, and improved material accuracy, as the systems can be calibrated to deliver precise quantities. Furthermore, the use of bulk bags reduces the need for multiple packaging and repackaging steps, streamlining the supply chain and enhancing overall operational efficiency.
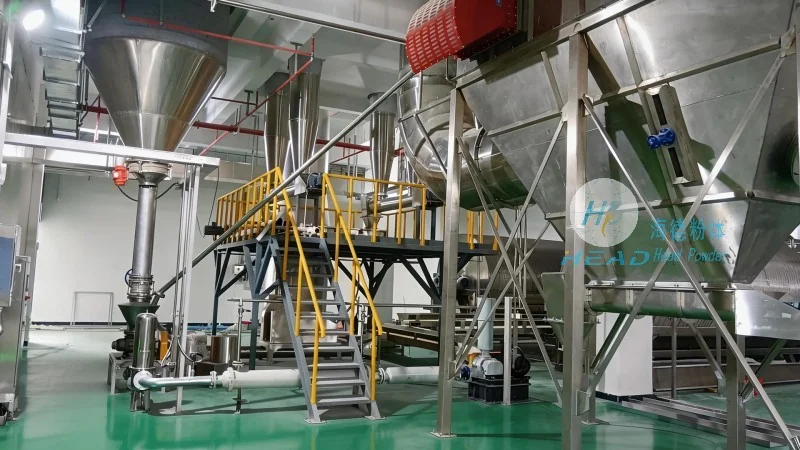
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading provider of advanced bulk bag powder handling solutions. With its headquarters located in Shandong, China, the company specializes in designing, manufacturing, and installing customized powder transport systems tailored to the specific needs of its clients. HeadPowder leverages years of industry experience to develop innovative solutions that address the challenges of material handling, ensuring reliability, efficiency, and safety. The company's commitment to quality is evident in its adherence to international standards and continuous investment in research and development. By partnering with HeadPowder, businesses gain access to state-of-the-art technology and expert support, enabling them to optimize their material handling processes and achieve competitive advantages in their respective markets.
Conclusion
Bulk bag powder handling systems are indispensable tools for modern industries, offering a combination of efficiency, safety, and adaptability that traditional material handling methods cannot match. The principles behind these systems, coupled with their operational characteristics, make them ideal for a wide range of applications. As industries continue to evolve and demand higher standards of productivity and safety, the importance of reliable bulk bag handling systems will only grow. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in meeting these demands, providing tailored solutions that enhance operational performance and support long-term growth. By understanding and implementing these systems effectively, businesses can unlock new levels of efficiency and ensure the smooth flow of their material processes.