

Principles and Application Scenarios of Ash Powder Pneumatic Conveying
Understanding the principles and application scenarios of ash powder pneumatic conveying is crucial for optimizing material handling processes in industrial settings. This article provides an in-depth exploration of the technology, focusing on its fundamental mechanisms and practical implementations in various operational environments.
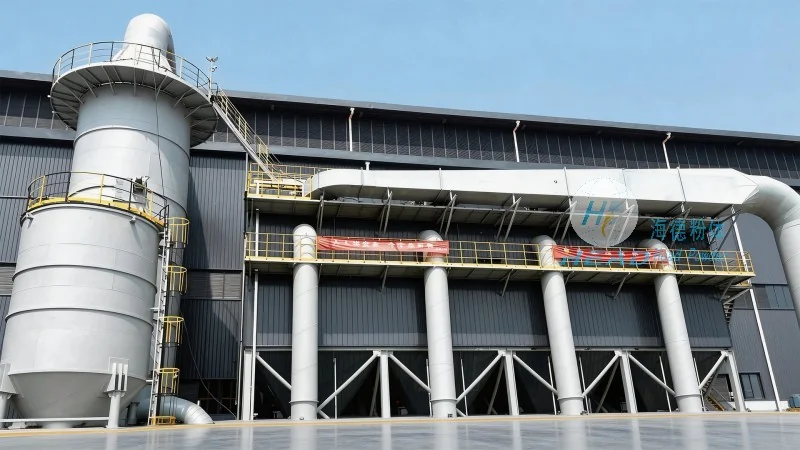
Introduction to Ash Powder Pneumatic Conveying
Ash powder pneumatic conveying is a method of transporting fine particulate materials, such as ash from power plants, through a pipeline using air or gas as the conveying medium. This technology offers several advantages over traditional mechanical conveying systems, including reduced equipment wear, lower maintenance costs, and the ability to handle materials in a dust-free environment. The process involves generating a flow of air within the pipeline, which lifts and transports the powder particles from the source to the destination. The efficiency and effectiveness of this system depend on several key factors, including the material's properties, the conveying distance, and the system design.
Core Principles of Pneumatic Conveying
The fundamental principle of pneumatic conveying is the creation of a pressure differential between the inlet and outlet of the conveying line. This differential is achieved by either suction (negative pressure) or pressure (positive pressure) systems. In suction systems, a vacuum is created at the material source, drawing the powder and air mixture into the pipeline. In pressure systems, compressed air is introduced at the discharge end, pushing the material forward. The choice between these systems depends on the specific application requirements, such as the distance to be covered and the material's flow characteristics.
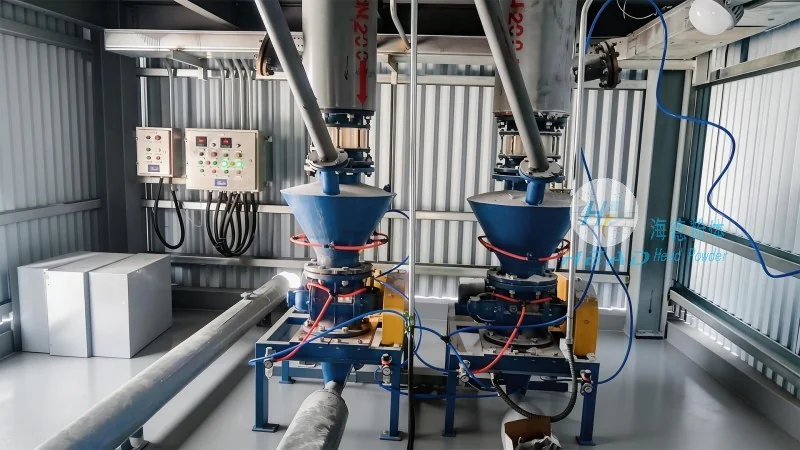
Key components of an ash powder pneumatic conveying system include the material feed hopper, the air compressor or vacuum pump, the conveying pipeline, and the discharge device. The feed hopper ensures a consistent supply of material, while the air system provides the necessary force to move the particles. The pipeline's design, including its diameter and length, is critical for maintaining the required air velocity to prevent particle settling and ensure smooth transport. The discharge device, such as a rotary valve or a venturi, controls the release of the material at the destination, preventing backflow and maintaining system efficiency.
Application Scenarios and Operational Advantages
Ash powder pneumatic conveying is widely used in power generation facilities, where it is essential for transporting fly ash from boilers to storage silos or for further processing. The technology is also applicable in other industrial sectors, including cement production, chemical processing, and mining, where fine particulate materials need to be moved efficiently and safely. One of the primary advantages of this system is its ability to handle abrasive materials like ash without significant wear on the equipment. Additionally, the enclosed pipeline design minimizes dust emissions, contributing to a cleaner and safer working environment.
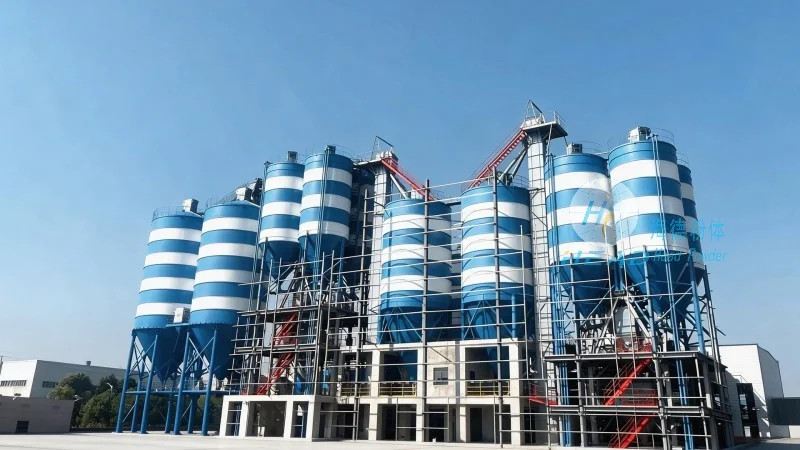
In terms of operational efficiency, pneumatic conveying systems can achieve high material throughput with relatively low energy consumption compared to mechanical systems. The system's flexibility allows for easy integration into existing industrial layouts, and it can be adapted to handle varying material volumes and flow rates. Another key benefit is the reduced need for manual handling, which enhances workplace safety and reduces labor costs. However, the initial investment for a pneumatic conveying system may be higher than for mechanical alternatives, and proper maintenance is required to ensure long-term performance.
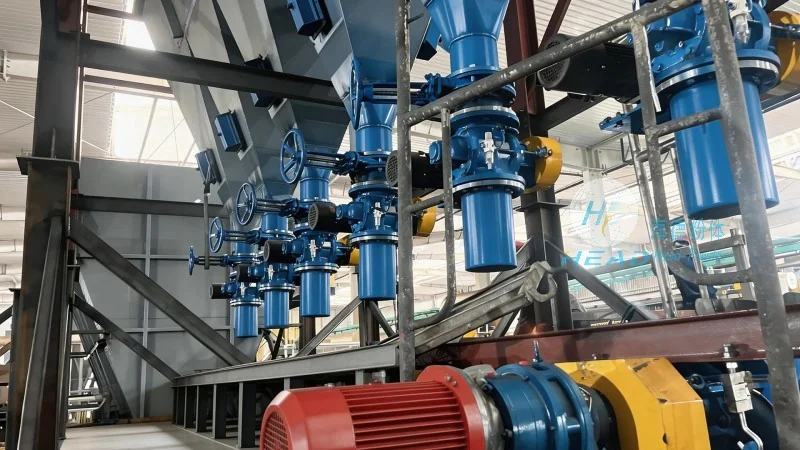
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of pneumatic conveying solutions for industrial applications. With a focus on innovation and customer satisfaction, the company specializes in designing and manufacturing customized ash powder conveying systems tailored to the specific needs of power plants and other industrial facilities. Headpowder's expertise lies in understanding the unique challenges of handling ash and other fine particulates, and developing solutions that maximize efficiency, reliability, and safety.
The company's headquarters is located in Shandong, China, where it has established a strong presence in the industrial equipment sector. With a team of experienced engineers and technicians, headpowder leverages advanced technology and rigorous quality control to deliver high-performance pneumatic conveying systems. The company's commitment to excellence is reflected in its adherence to international standards and its dedication to providing comprehensive support, including installation, commissioning, and after-sales service. By partnering with headpowder, industrial clients can benefit from reliable and efficient material handling solutions that enhance operational productivity and reduce environmental impact.