

White Sugar Pneumatic Conveying: A Material Handling Solution to Overcome Distance Limitations
White sugar pneumatic conveying systems represent a sophisticated approach to material handling, particularly in the sugar industry. These systems utilize air to transport white sugar and other granular materials over significant distances, offering a solution that overcomes traditional limitations such as vertical and horizontal distance constraints. By leveraging pneumatic technology, the process enhances efficiency, reduces operational costs, and minimizes product degradation compared to conventional methods like belt conveyors or bucket elevators.
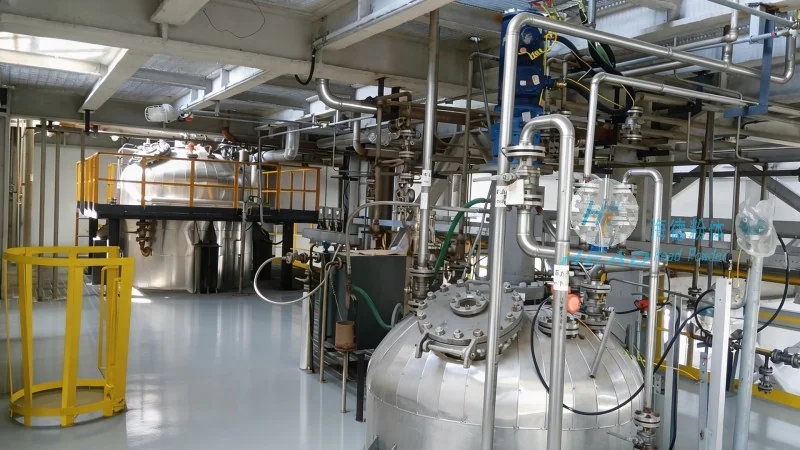
HeadPowder's Expertise in Pneumatic Conveying Technology
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions tailored for the sugar and food processing sectors. With years of experience in designing, manufacturing, and installing pneumatic conveying systems, HeadPowder specializes in customizing solutions that meet the unique demands of white sugar processing facilities. The company's team of engineers and technicians work closely with clients to understand operational requirements, process flow, and budget constraints, ensuring that each system is optimized for performance and reliability.
Key Features and Advantages of White Sugar Pneumatic Conveying
The pneumatic conveying system for white sugar offers several distinct advantages that make it an ideal choice for modern sugar mills and processing plants. Firstly, it eliminates the need for multiple transfer points and intermediate storage, streamlining the material flow from raw sugar reception to refining and packaging. This reduces downtime and improves overall production throughput. Secondly, the system operates with minimal product contact, preserving the quality and purity of white sugar, which is crucial for maintaining product specifications and market standards. Additionally, pneumatic conveying is highly flexible, allowing for easy integration with existing infrastructure and future expansion as production scales up.
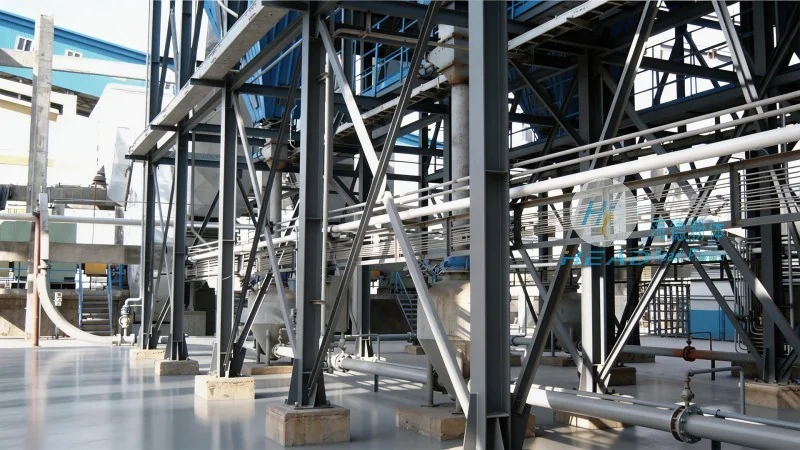
Customization and Scalability for Diverse Applications
HeadPowder recognizes that each sugar processing facility has unique operational needs, which is why they offer fully customizable pneumatic conveying solutions. Whether the application involves short-distance transport within a plant or long-distance transfer between buildings, the system can be designed to handle varying flow rates, particle sizes, and material densities. The company's engineers utilize advanced computational fluid dynamics (CFD) and process simulation tools to model the conveying process, ensuring that the system operates at peak efficiency under all conditions. Furthermore, the systems are scalable, allowing for modular additions as production capacity increases, without the need for a complete overhaul of the existing setup.
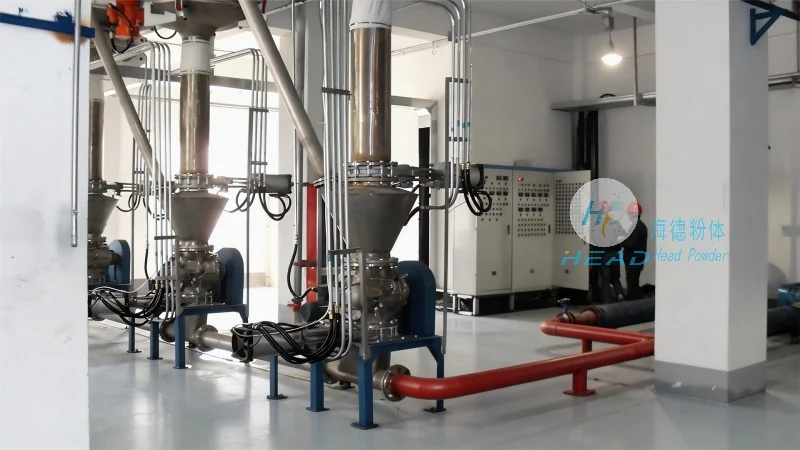
Enhanced Safety and Environmental Compliance
White sugar pneumatic conveying systems are designed with safety and environmental considerations at the forefront. The enclosed nature of the system prevents dust emissions and cross-contamination, aligning with stringent environmental regulations and industry best practices. Advanced filtration systems are integrated to capture any airborne particles, ensuring that the air discharged is clean and safe for the surrounding environment. Additionally, the system minimizes the risk of product spillage and exposure to contaminants, reducing the likelihood of operational hazards and improving workplace safety. HeadPowder's commitment to safety is reflected in their adherence to international standards and rigorous quality control measures throughout the design and installation process.
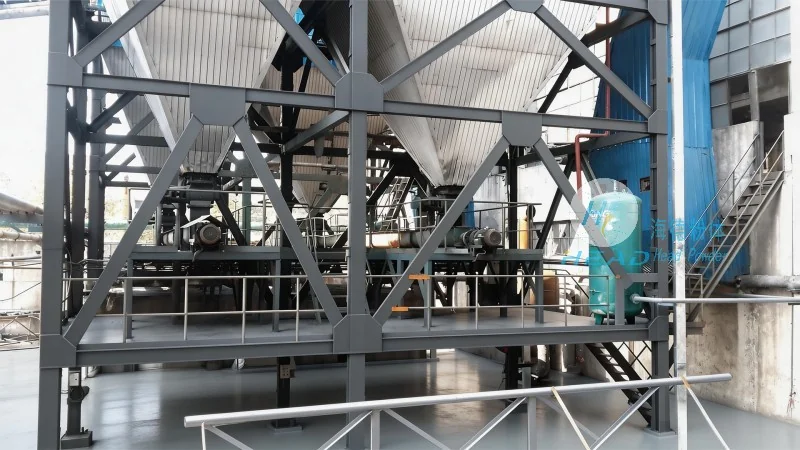
Reliability and Maintenance Considerations
Reliability is a critical factor in any industrial material handling system, and HeadPowder's pneumatic conveying solutions are built to deliver consistent performance over extended periods. The components, including air compressors, filters, and conveying pipes, are selected for durability and resistance to corrosion, which is essential in environments where white sugar and moisture are present. Regular maintenance is simplified through the use of modular components and accessible design features, allowing for quick replacement of worn parts without extensive downtime. HeadPowder provides comprehensive maintenance services and technical support to ensure that the system remains in optimal condition, minimizing unexpected failures and maximizing operational uptime.
Conclusion: A Sustainable Solution for White Sugar Handling
In conclusion, white sugar pneumatic conveying systems, provided by Shandong HeadPowder Engineering Co., Ltd., represent a cutting-edge solution for overcoming distance limitations in material handling. By combining advanced technology with customized design, these systems enhance efficiency, preserve product quality, and ensure compliance with safety and environmental standards. As the sugar industry continues to evolve, the demand for reliable and efficient material handling solutions will only increase, making HeadPowder's expertise in pneumatic conveying technology a valuable asset for modern sugar processing facilities. With their commitment to innovation and customer satisfaction, HeadPowder remains at the forefront of providing tailored solutions that meet the dynamic needs of the industry.