

Powdered Electrolyte Pneumatic Conveying Solutions
For industrial applications requiring the efficient and reliable transport of powdered electrolytes, the selection of an appropriate pneumatic conveying system is critical. This article introduces the advanced solutions offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, focusing on the technical aspects, benefits, and practical applications of pneumatic conveying for electrolyte powders.
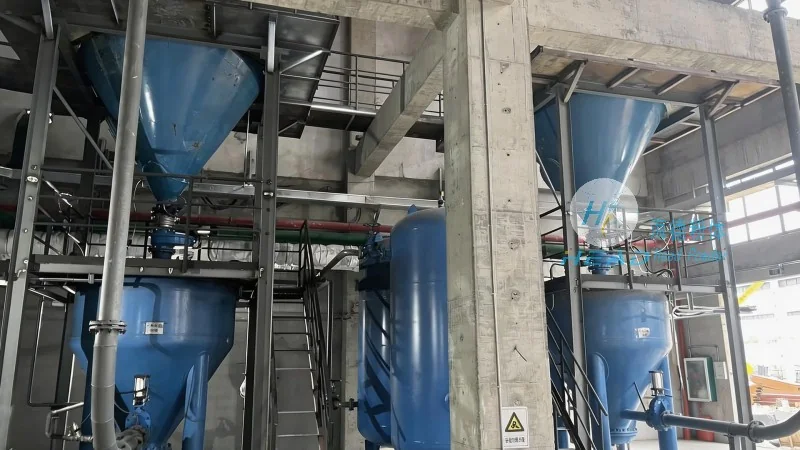
Understanding Pneumatic Conveying for Electrolyte Powders
Pneumatic conveying is a method that uses air or other gases to transport bulk materials, such as powdered electrolytes, through a pipeline system. This technology offers several advantages over traditional mechanical conveying methods, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are sensitive to moisture or contamination. The system typically consists of a hopper, a conveyor line, and a receiver, with the material being drawn into the pipeline by a vacuum or pressure source.
Key Features of HeadPowder's Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique requirements of electrolyte powder handling. Their solutions are engineered to ensure high efficiency, minimal product degradation, and compliance with industry standards. Key features include:
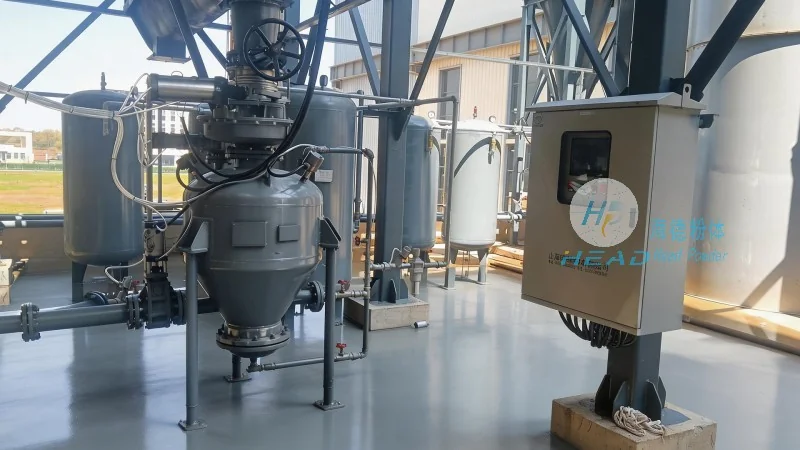
- Advanced material handling technology that minimizes product attrition and maintains particle integrity.
- Customizable system configurations to accommodate varying material properties, flow rates, and process requirements.
- Integration with existing production lines for seamless operation and minimal downtime.
- Robust construction using high-quality materials to withstand the demands of continuous operation in industrial environments.
Benefits of Implementing Pneumatic Conveying Systems
Adopting a pneumatic conveying system for electrolyte powders provides numerous benefits for manufacturers. These include improved process control, enhanced safety by reducing manual handling, and increased productivity through optimized material flow. The systems also contribute to lower operational costs by reducing energy consumption and maintenance requirements compared to traditional methods. Additionally, the ability to handle materials in a closed system helps maintain product quality and prevents environmental contamination.
Application Examples in Electrolyte Processing
The versatility of pneumatic conveying solutions makes them suitable for a wide range of electrolyte processing applications. For instance, in battery manufacturing, the efficient transport of lithium, sodium, or other electrolyte powders is essential for maintaining production efficiency. In chemical processing plants, the system can handle various types of electrolyte powders used in the production of industrial chemicals, ensuring consistent quality and reliable supply. The adaptability of these systems allows them to be integrated into existing production workflows, supporting continuous improvement and scalability.
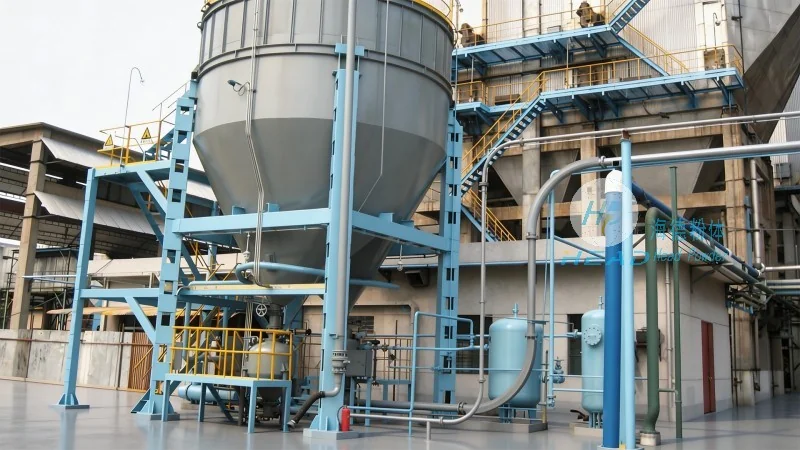
Customization and Technical Support from HeadPowder
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive technical support and customization services to meet the specific needs of each client. Their team of engineers works closely with customers to assess process requirements, material characteristics, and operational constraints, developing tailored solutions that maximize efficiency and performance. The company provides detailed system designs, including flow rate calculations, pressure drop assessments, and material compatibility studies, ensuring that the final solution is optimized for the intended application.
Conclusion: Enhancing Electrolyte Handling with Advanced Pneumatic Conveying
For industries relying on the consistent and efficient handling of powdered electrolytes, pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. represent a superior choice. By leveraging advanced technology and customized solutions, these systems address the challenges of material transport while delivering significant benefits in terms of efficiency, safety, and cost-effectiveness. As a trusted partner in the field, HeadPowder continues to provide innovative solutions that support the evolving needs of industrial electrolyte processing.