

Working Principle and Features of Organic Fertilizer Powder Pneumatic Conveying Equipment
Organic fertilizer powder pneumatic conveying equipment is a specialized system designed for the efficient and reliable transport of organic fertilizer powders. This equipment plays a crucial role in modern agricultural and fertilizer processing operations, ensuring that organic materials are moved safely and effectively from storage to processing or application points. The technology behind these systems combines principles of fluidization, air flow, and mechanical design to achieve seamless material handling.
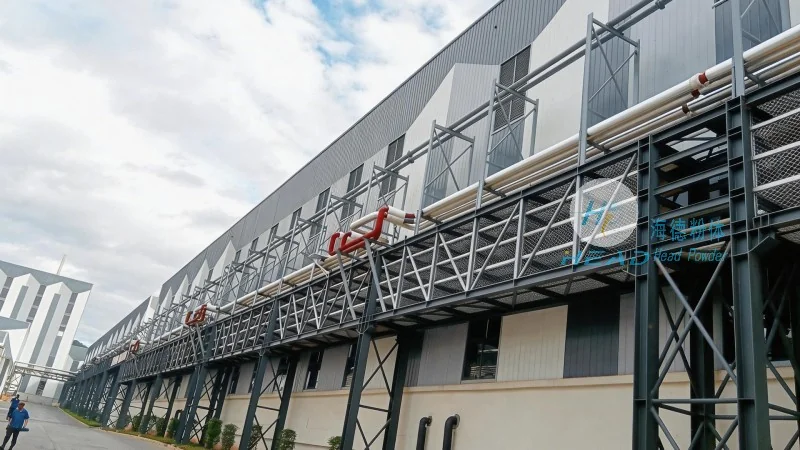
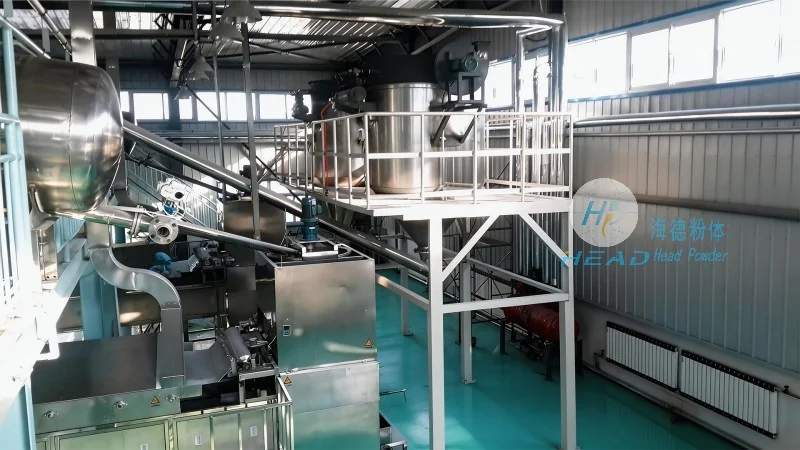
Understanding the Working Principle of Organic Fertilizer Powder Pneumatic Conveying Equipment
The core working principle of organic fertilizer powder pneumatic conveying equipment revolves around the use of air as the conveying medium. The system typically consists of a hopper, a blower or air compressor, a pipeline network, and a discharge point. When organic fertilizer powder is fed into the hopper, the blower generates a high-pressure airflow that lifts the powder particles and propels them through the pipeline. This process, known as pneumatic conveying, relies on the interaction between the air stream and the powder particles to maintain suspension and transport them over distances. The equipment may use different modes such as dilute phase or dense phase conveying, depending on the characteristics of the organic fertilizer and the required transport distance. In dilute phase conveying, the powder is carried in a low concentration within the air stream, while dense phase conveying uses higher air pressure to move the powder in a more concentrated manner, often with lower air velocity to reduce particle degradation. The working principle also involves the use of appropriate air velocities and pipeline diameters to prevent clogging and ensure consistent flow. The system may include components like cyclones, filters, and pressure vessels to manage the air and powder mixture, ensuring that the organic fertilizer is delivered without loss or contamination.
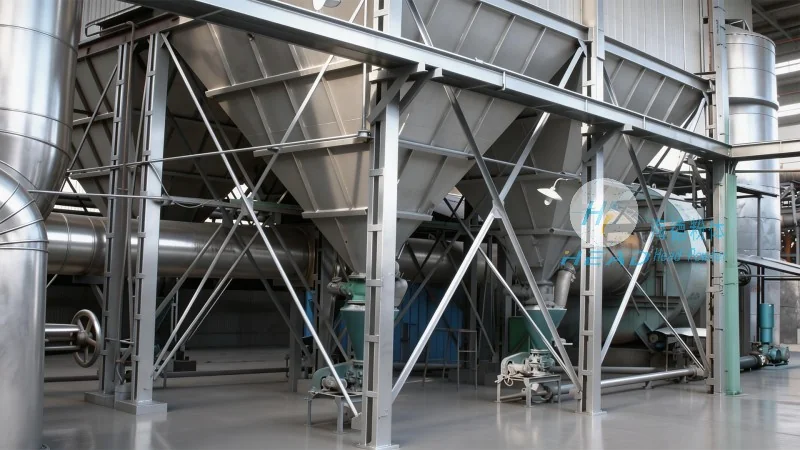
Key Features of Organic Fertilizer Powder Pneumatic Conveying Equipment
Organic fertilizer powder pneumatic conveying equipment offers several distinct features that make it an ideal choice for handling organic materials. First, it provides a dust-free and hygienic conveying process, which is critical for organic fertilizers that may contain pathogens or require contamination control. The enclosed system prevents the release of fine particles into the environment, enhancing safety and compliance with environmental regulations. Second, the equipment is highly efficient in terms of energy consumption and operational costs. By using air as the conveying medium, it eliminates the need for mechanical components like belts or buckets, reducing wear and maintenance requirements. This results in lower operational expenses and longer equipment lifespan. Third, the system offers flexibility in terms of layout and installation. It can be configured to handle various organic fertilizer types, including compost, manure, and other organic residues, with adjustable settings for different particle sizes and moisture contents. The modular design allows for easy integration into existing production lines or expansion as production needs grow. Fourth, the equipment ensures minimal product degradation during transport. The low impact and gentle handling of the pneumatic system prevent clumping or breakdown of the organic fertilizer particles, maintaining the quality and effectiveness of the final product. Additionally, the system can be equipped with monitoring and control systems to optimize performance, such as real-time pressure and flow monitoring, ensuring consistent and reliable operation. These features collectively make organic fertilizer powder pneumatic conveying equipment a superior solution for modern organic fertilizer processing and distribution.
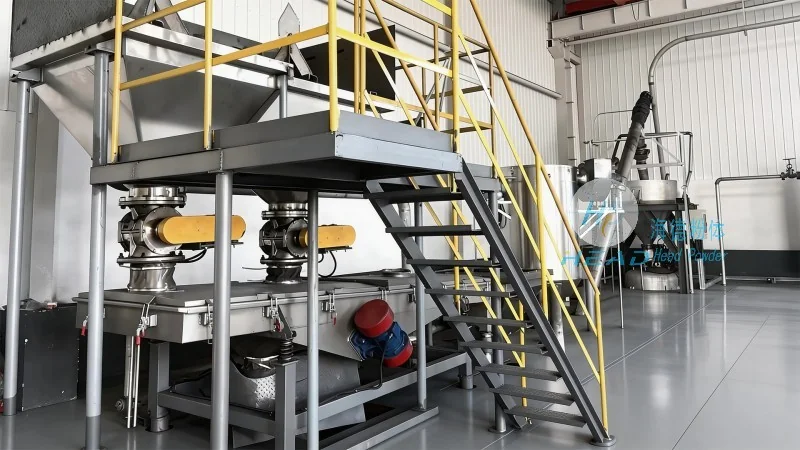
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer of specialized conveying and processing equipment for the fertilizer industry. With a strong focus on innovation and quality, the company has established itself as a trusted partner for clients seeking reliable solutions for organic fertilizer handling. HeadPowder's expertise lies in designing and manufacturing equipment that meets the unique challenges of organic fertilizer processing, ensuring that their products are durable, efficient, and compliant with industry standards. The company's facilities are located in Shandong, China, where they leverage advanced manufacturing techniques and rigorous quality control processes to deliver high-performance equipment. By combining technical expertise with customer-centric service, HeadPowder aims to support the growth and sustainability of the organic fertilizer industry, providing equipment that enhances operational efficiency and product quality. Their commitment to research and development ensures that their products remain at the forefront of technological advancements in material handling, catering to the evolving needs of agricultural and environmental sectors.