

Working Principle and Characteristics of Air-Driven Material Transport for Ammonium Bicarbonate
Ammonium bicarbonate, a widely used chemical in various industrial applications, often requires efficient and reliable material handling solutions. The air-driven transport system for ammonium bicarbonate offers a sophisticated approach to managing the material's flow, ensuring safety, efficiency, and minimal environmental impact. This article explores the working principle and key characteristics of such a system, providing insights into its operational mechanics and advantages.
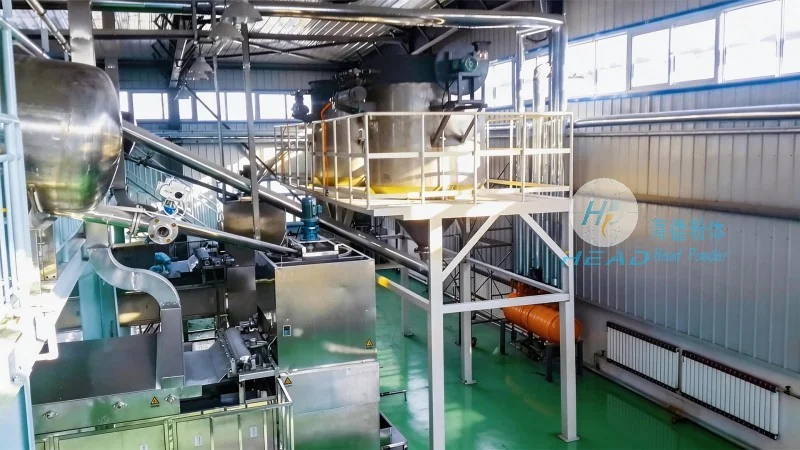
Working Principle of Air-Driven Material Transport for Ammonium Bicarbonate
The air-driven transport system for ammonium bicarbonate operates on the principle of pneumatic conveying, where the material is transported through a pipeline using a combination of air pressure and vacuum. The process typically involves several key components: a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the material's deposition. The system can be categorized into two main types: dilute-phase and dense-phase conveying, each tailored to different material properties and transport requirements.
In dilute-phase conveying, the material is suspended in a stream of air and transported at relatively high velocities. This method is suitable for materials with good flowability and low dust generation. The air velocity is maintained above the material's terminal velocity to keep the particles in suspension. Conversely, dense-phase conveying involves transporting the material in a more compact form, with lower air velocities and higher material concentration. This approach is ideal for materials that are prone to bridging or caking, as it reduces the risk of blockages and ensures a more controlled flow.
The working principle also includes the role of the air compressor or vacuum pump, which generates the necessary pressure or vacuum to move the material. The system may use positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out), depending on the application and the distance of the transport. For ammonium bicarbonate, which is a fine powder with potential for dust generation, the system is designed to minimize particle loss and ensure compliance with safety regulations. The use of appropriate filtration and dust collection systems is integral to maintaining air quality and preventing contamination.
Key Characteristics of Air-Driven Material Transport for Ammonium Bicarbonate
The air-driven transport system for ammonium bicarbonate exhibits several distinct characteristics that make it an attractive solution for industrial material handling. Firstly, it offers a high degree of flexibility in terms of transport distance and layout. Unlike traditional mechanical conveyors, pneumatic systems can be easily reconfigured to accommodate changes in production processes or facility expansions. This adaptability is particularly valuable in industries where production lines are frequently modified or scaled.
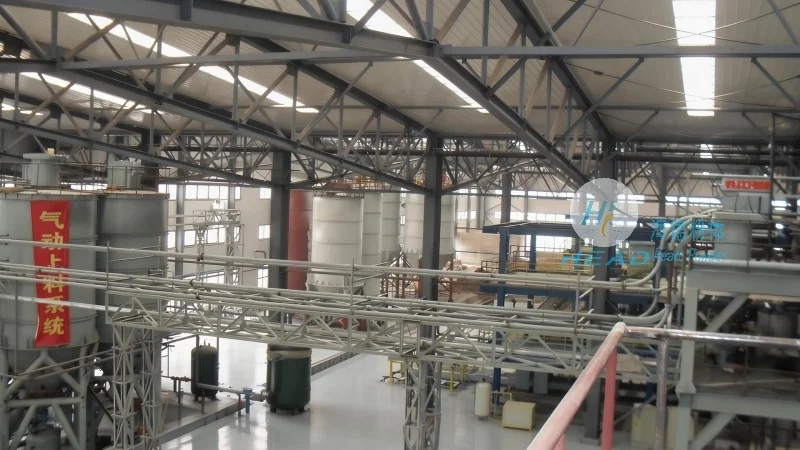
Secondly, the system provides excellent control over the material flow rate and pressure. By adjusting the air flow or vacuum levels, operators can precisely regulate the speed at which ammonium bicarbonate is transported. This level of control is crucial for maintaining consistent product quality and preventing overloading or underloading of downstream equipment. The ability to monitor and adjust parameters in real-time enhances process reliability and reduces the risk of operational disruptions.
Thirdly, the air-driven system offers significant advantages in terms of safety and hygiene. Since the material is transported in a closed pipeline, there is minimal exposure to the environment, reducing the risk of dust inhalation or contamination. This is particularly important for ammonium bicarbonate, which can be a respiratory irritant if not handled properly. The closed system also helps in maintaining product purity, as it prevents cross-contamination with other materials or external elements.
Additionally, the system is energy-efficient compared to traditional mechanical conveyors. By utilizing air as the primary transport medium, the energy consumption is lower, especially for longer distances. The use of efficient air compressors and vacuum pumps further optimizes energy usage, contributing to cost savings and environmental sustainability. This makes the air-driven system a cost-effective solution for large-scale ammonium bicarbonate handling operations.
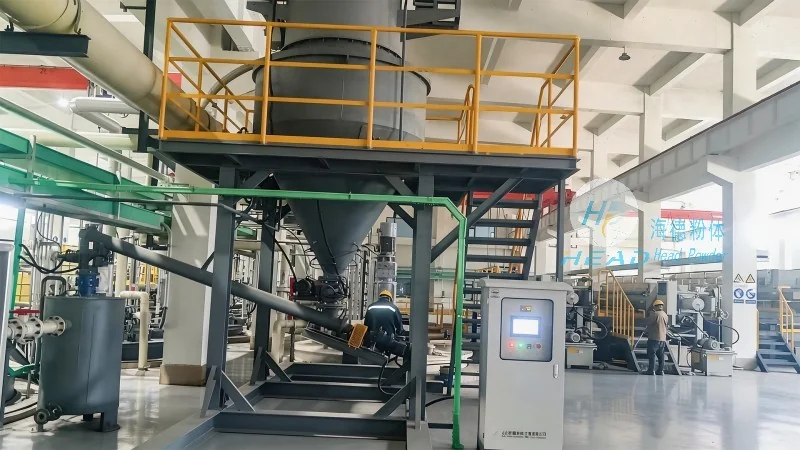
Another notable characteristic is the system's ability to handle varying material conditions. Whether the ammonium bicarbonate is in a dry, free-flowing state or has some moisture content, the air-driven system can be adapted to maintain optimal flow characteristics. The design of the feeder and hopper ensures that the material is consistently fed into the pipeline, preventing blockages and ensuring smooth operation. This adaptability is essential for maintaining production continuity and minimizing downtime.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized engineering solutions for material handling and processing. With a focus on innovation and customer-centric approaches, the company has established itself as a trusted partner in the chemical and industrial sectors. Headpowder specializes in designing and manufacturing air-driven transport systems tailored to the unique requirements of ammonium bicarbonate and other fine powders. The company's expertise lies in integrating advanced technology with practical applications, ensuring that each system is optimized for efficiency, safety, and reliability.
Headpowder's commitment to quality is evident in its adherence to international standards and rigorous testing protocols. The company's engineers and technicians work closely with clients to understand their specific needs, from initial design and installation to ongoing maintenance and support. This collaborative approach ensures that the air-driven transport systems are not only effective but also aligned with the client's operational goals and budget constraints. By leveraging years of experience and continuous research, Headpowder delivers solutions that enhance productivity, reduce operational costs, and improve overall process performance.
Headpowder's facilities are equipped with state-of-the-art equipment and a skilled workforce, enabling the company to handle complex projects with precision and efficiency. The company's location in Shandong, China, provides easy access to key markets and supply chains, facilitating timely delivery and after-sales support. Whether for new installations or system upgrades, Headpowder offers comprehensive services that cover every aspect of the air-driven material transport process, from concept development to long-term maintenance.