

[W]Working Principle and Characteristics of Air-Driven Stone Aggregate Conveying
HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced air-driven conveying systems for various bulk materials, including stone aggregates. This article explores the fundamental working principle and key characteristics of such systems, offering insights into their efficiency and practical applications.
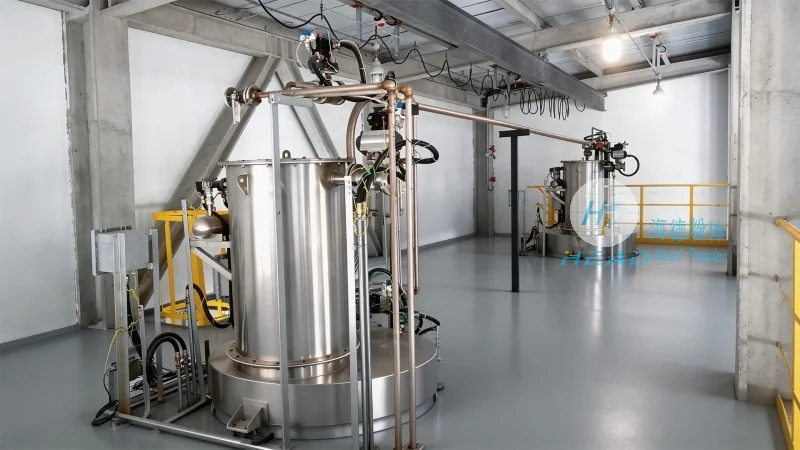
Understanding the Working Principle of Air-Driven Stone Aggregate Conveying
The core mechanism of air-driven stone aggregate conveying involves the use of compressed air to transport solid particles through a pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a conveying line. As compressed air is introduced into the pipeline, it creates a low-pressure zone that draws the stone aggregates forward through the system. This method, often referred to as pneumatic conveying, relies on the interaction between the air flow and the material particles to achieve transport. The system may utilize different configurations, such as dilute-phase or dense-phase conveying, depending on the material properties and required delivery conditions. In dilute-phase systems, the material is suspended in the air stream, while dense-phase systems use higher air pressure to push the material in a more compact form. This flexibility allows for the efficient handling of various stone aggregate sizes and types, from fine sand to coarse gravel.
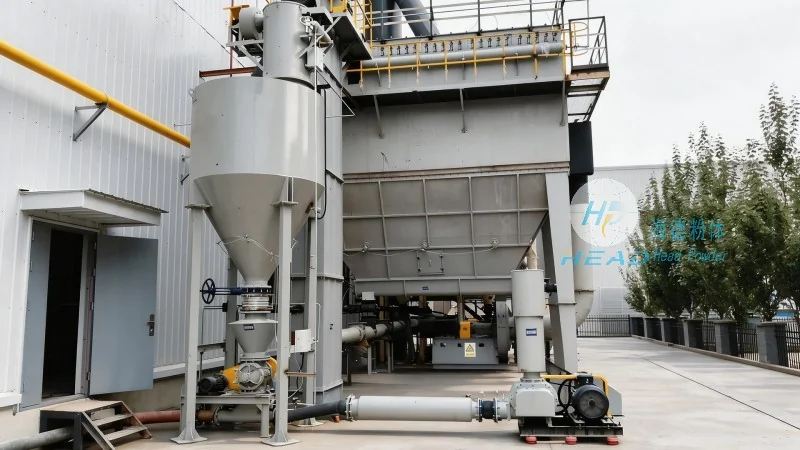
Key Characteristics of Air-Driven Stone Aggregate Conveying Systems
Several distinct characteristics define air-driven stone aggregate conveying systems, making them suitable for diverse industrial applications. Firstly, these systems offer high efficiency in material transport, with the ability to move large volumes of stone aggregates over considerable distances with minimal energy consumption compared to traditional methods like belt conveyors or trucks. The pneumatic approach eliminates the need for mechanical components at transfer points, reducing wear and maintenance requirements. Secondly, air-driven systems provide excellent control over material flow, allowing for precise regulation of delivery rates and pressure, which is crucial for maintaining consistent production processes. This control is particularly beneficial in applications where uniform material distribution is essential, such as in concrete mixing or asphalt production. Thirdly, the systems are highly adaptable to different operational environments. They can be installed in confined spaces or integrated into existing production lines without significant structural modifications. Additionally, air-driven conveying is effective in handling materials that are prone to dust or require dust control, as the enclosed pipeline system minimizes environmental contamination. The technology also supports the conveyance of materials with varying moisture content, ensuring that the stone aggregates remain in optimal condition throughout the transport process.
Applications and Benefits in Industrial Settings
HeadPowder's air-driven stone aggregate conveying systems are widely utilized across various industries, including construction, mining, and manufacturing. In the construction sector, these systems are essential for transporting aggregates from storage silos to concrete batching plants, ensuring a steady and controlled supply of materials. The ability to handle different aggregate sizes and maintain consistent flow rates enhances the efficiency of concrete production, reducing downtime and material waste. In mining operations, air-driven conveying is employed to transport crushed stone and ore from processing facilities to storage or processing sites, improving operational safety by eliminating the need for heavy machinery and manual handling. The systems also contribute to cost savings by reducing labor costs associated with material transport and minimizing the environmental impact of dust emissions. Furthermore, the adaptability of these systems allows them to be integrated into existing infrastructure, making them a practical solution for upgrading or expanding material handling capabilities without major disruptions to ongoing operations.
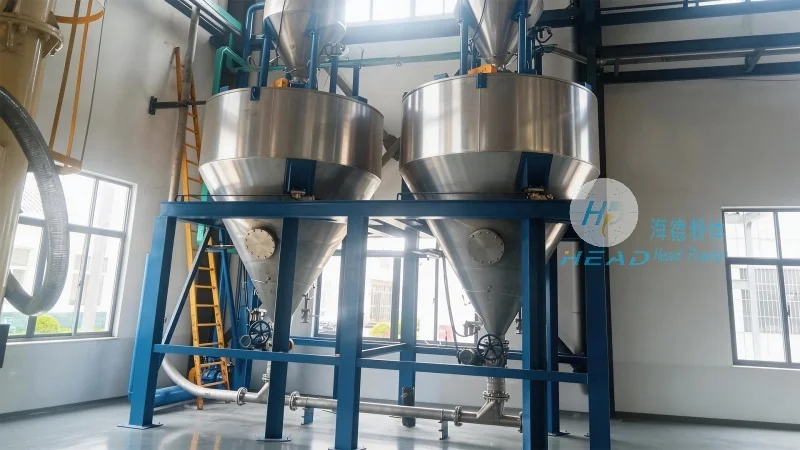
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted manufacturer of advanced air-driven material conveying solutions. With a focus on innovation and customer-centric design, the company provides tailored systems that meet the specific needs of its clients. By leveraging the principles of pneumatic conveying, HeadPowder's systems offer superior performance, reliability, and efficiency in handling stone aggregates. The company's commitment to quality and technological advancement ensures that its products remain at the forefront of industrial material handling solutions, supporting the growth and productivity of various industries worldwide.