

Anhydrous Sodium Sulfate Air-Solid Pneumatic Conveyor: Introduction and Structural Principles
The air-solid pneumatic conveyor is a specialized equipment designed for the efficient and reliable transportation of anhydrous sodium sulfate. This equipment is widely used in industrial applications where the safe and effective handling of bulk materials is critical. The system operates by utilizing compressed air to move the material through a pipeline, ensuring minimal product degradation and maintaining consistent flow rates. As a key component in material handling systems, this conveyor plays a vital role in optimizing production processes and enhancing operational efficiency.
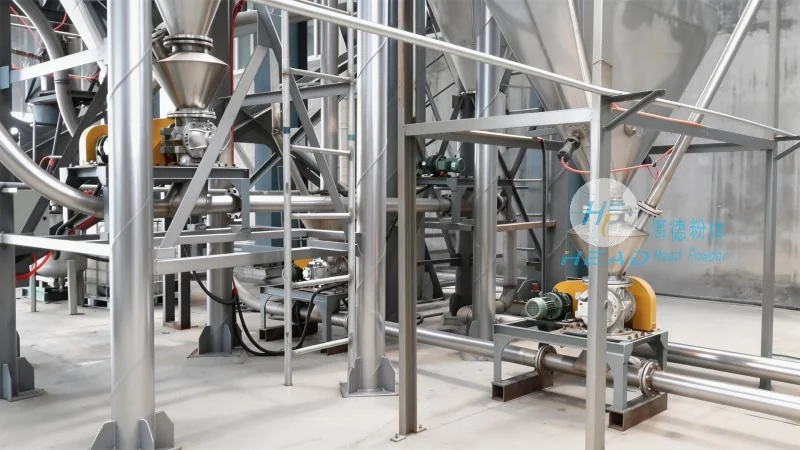
Structural Components and Working Principle
The anhydrous sodium sulfate air-solid pneumatic conveyor consists of several essential components that work in tandem to achieve effective material transport. The primary parts include the hopper, which serves as the material storage and feeding unit; the air compressor, responsible for generating the necessary air pressure; the pipeline system, which forms the conduit for material and air flow; and the control valves and sensors that regulate the operation and monitor system performance. The working principle involves the material being fed into the hopper, where it is then drawn into the pipeline by the high-pressure air from the compressor. The air and material mixture travels through the pipeline to the discharge point, where the material is separated from the air and collected. This process ensures a continuous and controlled flow of anhydrous sodium sulfate, minimizing downtime and maximizing throughput.
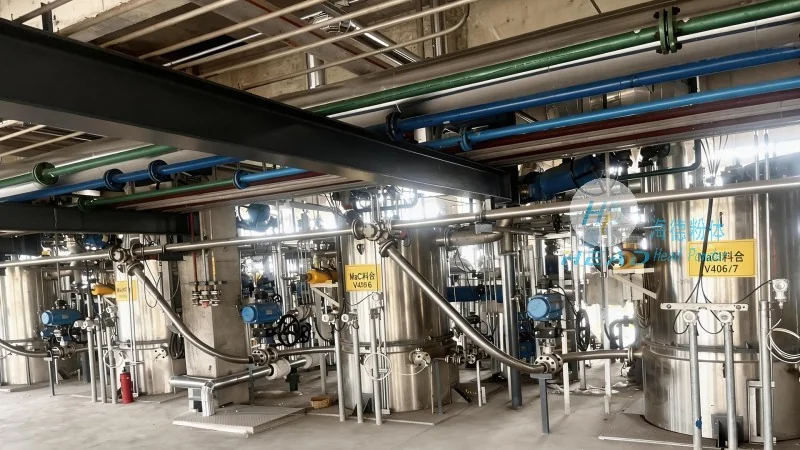
Key Features and Advantages
When considering the air-solid pneumatic conveyor for anhydrous sodium sulfate applications, several key features and advantages stand out. One of the primary benefits is the ability to handle bulk materials without the need for mechanical components like belts or chains, which reduces maintenance requirements and operational costs. The system also offers excellent flexibility in terms of layout and installation, as the pipeline can be configured to follow the existing production line layout. Additionally, the conveyor provides a hygienic and dust-free environment, which is crucial for maintaining product quality and meeting regulatory standards. The compact design of the equipment allows for easy integration into existing facilities, making it a cost-effective solution for material handling needs.
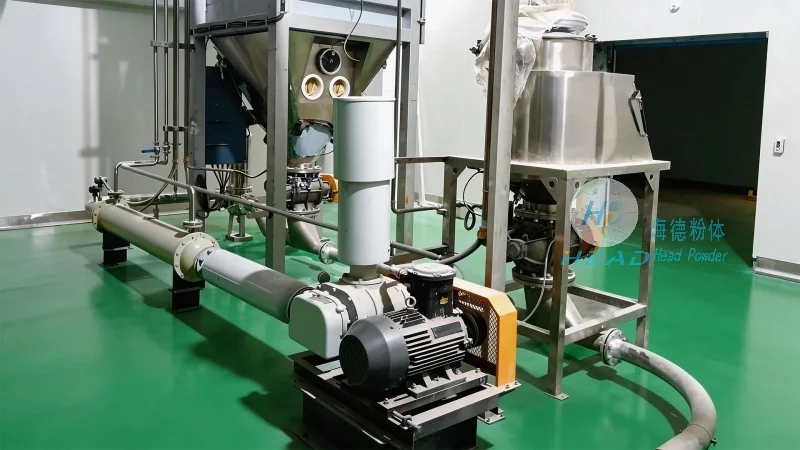
Application Scenarios and Industry Use Cases
The anhydrous sodium sulfate air-solid pneumatic conveyor is particularly suitable for various industrial applications where the transportation of bulk materials is required. In the chemical industry, it is commonly used for moving raw materials and finished products between processing units. In the food and pharmaceutical sectors, the system is employed to transport materials in a controlled and sanitary manner, ensuring product purity and safety. Furthermore, in the mining and mineral processing industries, the conveyor is utilized for the transport of anhydrous sodium sulfate from storage to processing equipment. The versatility of the system makes it adaptable to different production environments and material characteristics, providing a reliable solution for diverse industrial needs.
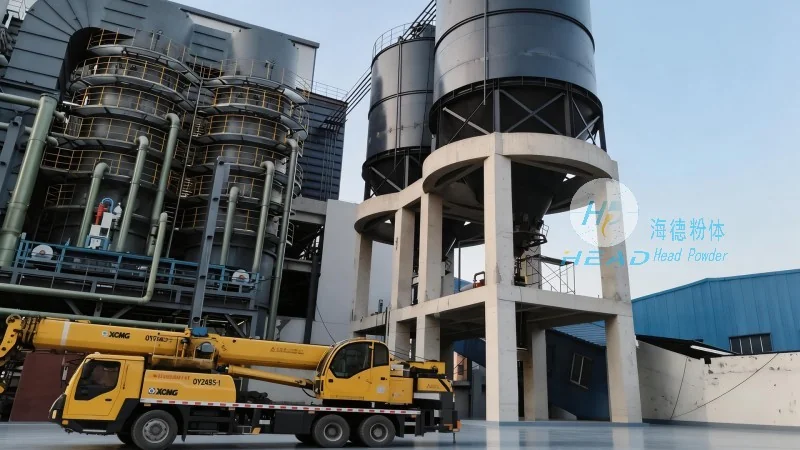
Company Information and Technical Support
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of material handling equipment, specializing in the design and production of air-solid pneumatic conveyors. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific requirements of clients. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. Headpowder offers comprehensive technical support, including installation guidance, maintenance services, and after-sales assistance, ensuring that clients receive the best possible service and support throughout the equipment's lifecycle. By choosing headpowder's anhydrous sodium sulfate air-solid pneumatic conveyor, businesses can benefit from reliable performance, enhanced efficiency, and long-term cost savings.