

[Pneumatic Conveying in Bulk Handling of Sodium Sulfate]
For industries dealing with bulk materials like sodium sulfate, efficient and reliable transportation methods are crucial. Pneumatic conveying systems have emerged as a preferred solution, offering advantages such as reduced contamination, lower maintenance costs, and enhanced safety compared to traditional methods. This article explores the application of pneumatic conveying in the bulk handling of sodium sulfate, highlighting the benefits and technical considerations for effective material transport.
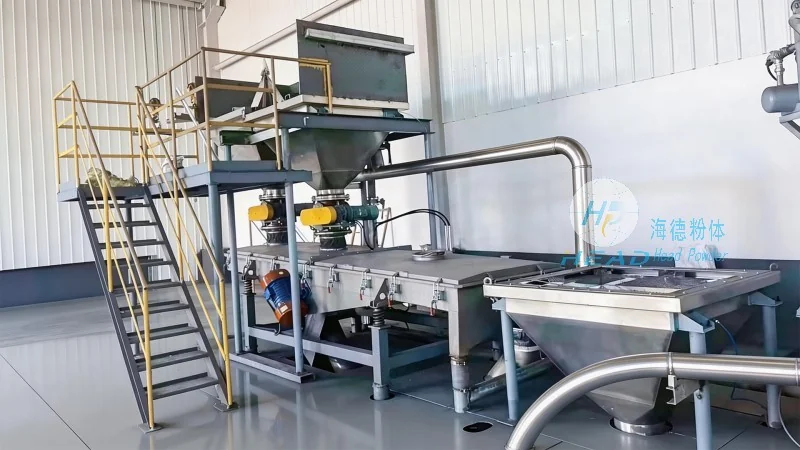
Understanding Sodium Sulfate and Its Handling Requirements
Sodium sulfate, also known as Glauber's salt or mirabilite, is a white crystalline solid commonly used in various industries, including glass manufacturing, paper production, and chemical processing. Its bulk handling requires specialized equipment to ensure consistent flow and minimize material degradation. Traditional methods like belt conveyors or screw conveyors may introduce friction and heat, potentially affecting the quality of the product. Pneumatic conveying addresses these challenges by using air to transport the material, maintaining its integrity throughout the process.
HeadPowder Engineering's Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of sodium sulfate processing. The company's expertise lies in understanding the unique properties of sodium sulfate, such as its hygroscopic nature and potential for dust generation, and developing systems that mitigate these issues. HeadPowder's solutions include positive pressure and negative pressure conveying systems, each optimized for different operational conditions and material flow rates.
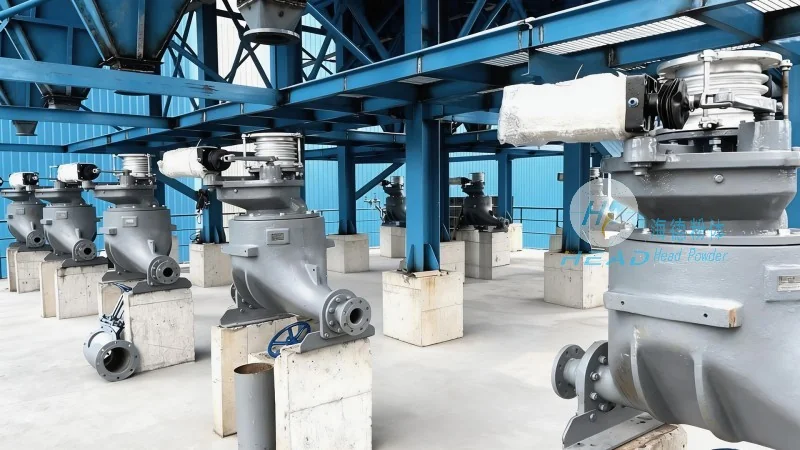
Key Benefits of Pneumatic Conveying for Sodium Sulfate
Implementing pneumatic conveying for sodium sulfate offers several advantages. Firstly, it eliminates the need for mechanical components that can cause contamination or damage to the material. The enclosed system ensures that the sodium sulfate remains clean and free from external pollutants, which is critical for applications where purity is paramount. Secondly, pneumatic conveying reduces labor costs by automating the material transport process, minimizing the need for manual handling and associated risks. Additionally, the system's flexibility allows for easy integration with existing production lines, enabling seamless material flow from storage to processing units.
Technical Considerations for Effective Pneumatic Conveying
Successful implementation of pneumatic conveying for sodium sulfate requires careful consideration of several technical factors. The choice between positive and negative pressure systems depends on the distance and elevation changes in the material transport path. Positive pressure systems are suitable for short to medium distances and vertical lifts, while negative pressure systems are better for longer horizontal runs. The air velocity and pressure must be optimized to prevent material degradation and ensure consistent flow. HeadPowder Engineering conducts thorough assessments of the operational environment, including material characteristics, system layout, and safety requirements, to design systems that meet the specific needs of each client.
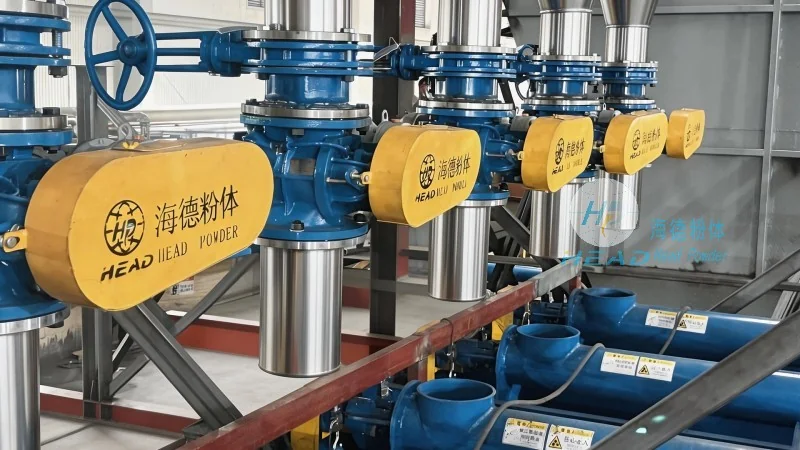
Case Studies and Real-World Applications
HeadPowder Engineering has successfully implemented pneumatic conveying systems for sodium sulfate in various industrial settings. For example, a glass manufacturing plant in China reduced material handling time by 40% and improved product purity by 15% after adopting a positive pressure pneumatic conveying system designed by the company. Another client, a chemical processing facility, reported lower maintenance costs and increased production efficiency by integrating a negative pressure system that minimized dust emissions and improved material flow consistency. These case studies demonstrate the effectiveness of pneumatic conveying in enhancing operational performance and meeting the stringent requirements of sodium sulfate processing.
Conclusion and Future Outlook
Pneumatic conveying represents a highly effective solution for the bulk handling of sodium sulfate, offering significant advantages over traditional methods. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can optimize their material transport processes, improve product quality, and reduce operational costs. As technology advances, further innovations in pneumatic conveying systems are expected to enhance efficiency and sustainability, making it an even more attractive option for sodium sulfate handling in the future.