

Working Principle and Features of High-Calcium Powder Conveying Systems
High-calcium powder conveying systems are essential in industrial applications where the efficient and safe transport of calcium-rich powders is critical. These systems are designed to handle materials with high calcium content, which often present unique challenges such as dust generation, caking, and abrasive wear. Understanding the working principle and key features of such systems is crucial for optimizing performance and ensuring operational reliability in various industries, including food processing, pharmaceuticals, and chemical manufacturing.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and supply of advanced powder handling solutions. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable high-calcium powder conveying systems. HeadPowder's products are engineered to meet the specific demands of diverse industrial applications, ensuring durability, efficiency, and compliance with industry standards.
The Working Principle of High-Calcium Powder Conveying Systems
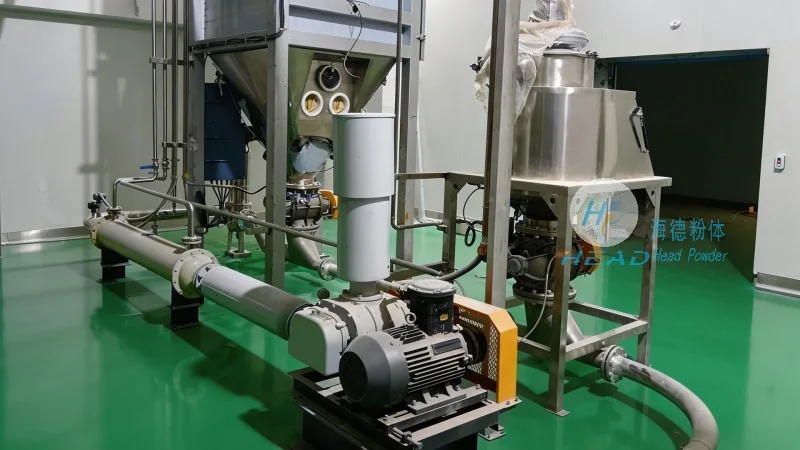
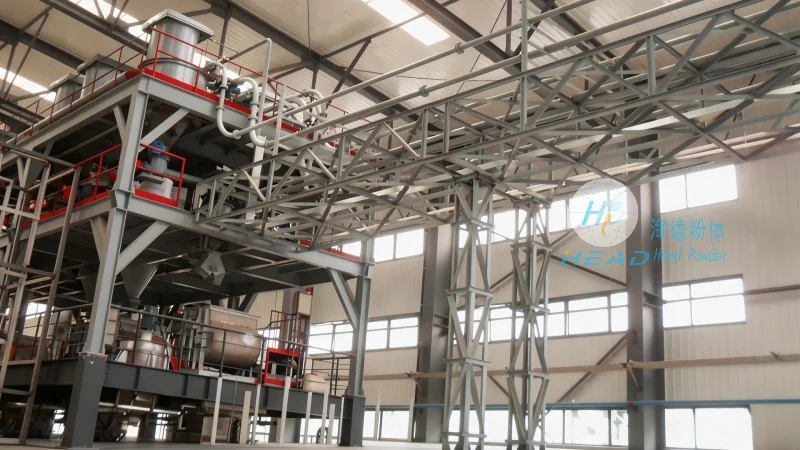
High-calcium powder conveying systems typically operate on the principle of pneumatic or mechanical transport, depending on the material characteristics and application requirements. Pneumatic conveying systems utilize air pressure to move powders through a network of pipes, while mechanical systems employ screws, belts, or other mechanisms to transport the material. In the case of high-calcium powders, the system design must account for the material's density, flowability, and potential for agglomeration. The conveying process begins with the material being fed into a hopper or feeder, where it is then transported through the system via air or mechanical action. The system is equipped with components such as cyclones, filters, and dust collectors to ensure the material is handled safely and efficiently, minimizing the risk of dust exposure and product contamination.
Key Features of High-Calcium Powder Conveying Systems
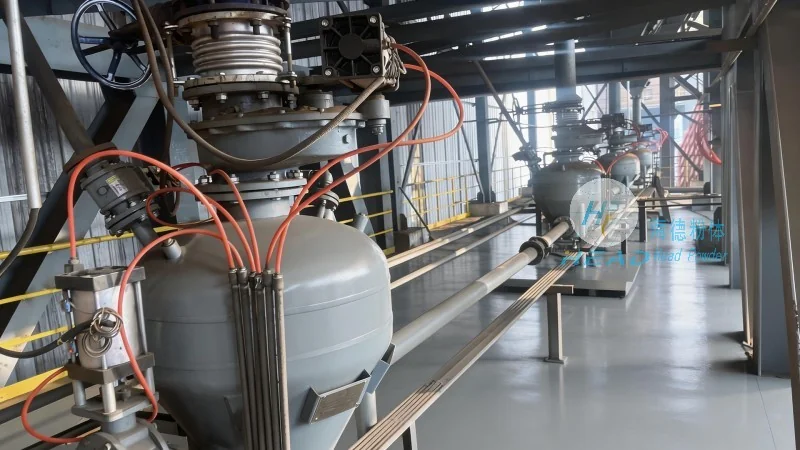
High-calcium powder conveying systems from HeadPowder are characterized by several key features that enhance their performance and reliability. One of the primary features is the use of robust materials of construction, such as stainless steel or specialized alloys, to withstand the abrasive nature of high-calcium powders and prevent corrosion. The systems are also equipped with advanced control systems that allow for precise regulation of flow rates, pressure, and temperature, ensuring optimal operation under varying conditions. Additionally, the design incorporates features to minimize dust generation and improve material handling efficiency, including sealed hoppers, airlocks, and efficient filtration systems. These features not only enhance safety but also contribute to the overall efficiency and longevity of the system.
Applications and Benefits
High-calcium powder conveying systems are widely used in various industries due to their ability to handle challenging materials. In the food industry, these systems are employed to transport calcium-rich ingredients such as calcium carbonate or calcium phosphate, ensuring consistent quality and safety in food products. In the pharmaceutical sector, the systems are used to convey active pharmaceutical ingredients (APIs) and excipients, where precision and contamination control are paramount. The benefits of using high-calcium powder conveying systems include improved process efficiency, reduced downtime, enhanced safety, and lower maintenance costs. By leveraging advanced technology and engineering expertise, HeadPowder's systems provide customers with reliable solutions that meet the stringent requirements of modern industrial operations.
Conclusion
High-calcium powder conveying systems represent a critical component in the efficient handling of calcium-rich materials across various industries. The working principle and key features of these systems, as exemplified by HeadPowder's offerings, are designed to address the unique challenges associated with high-calcium powders. By investing in advanced conveying solutions, businesses can enhance operational efficiency, ensure product quality, and maintain compliance with industry regulations. HeadPowder's commitment to innovation and quality makes it a leading choice for companies seeking reliable and effective high-calcium powder conveying systems.