

Working Principles and Features of Mobile Material Handling Systems
Mobile material handling systems are critical components in modern industrial operations, designed to efficiently transport and manage materials within various production environments. These systems offer flexibility and adaptability, allowing for dynamic reconfiguration of material flow based on operational needs. As a key solution for optimizing workflow and enhancing productivity, mobile material handling equipment plays a vital role in sectors ranging from manufacturing to logistics and warehousing.
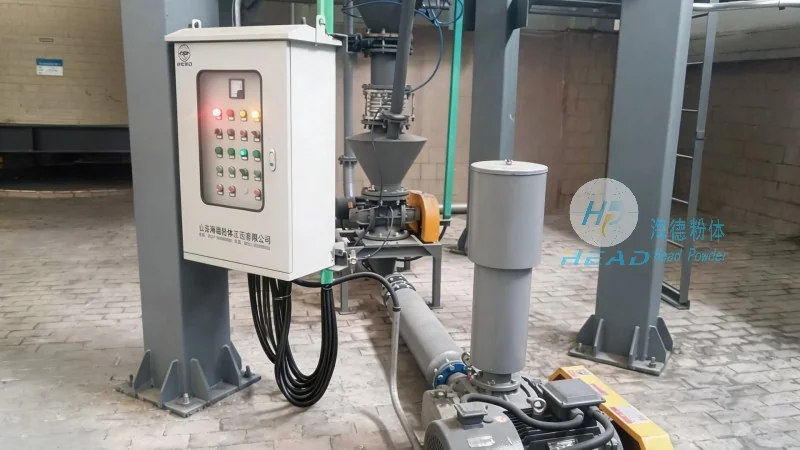
Working Principles of Mobile Material Handling Equipment
The core working principles of mobile material handling systems revolve around the integration of advanced engineering and intelligent control mechanisms. These systems typically utilize hydraulic or electric power sources to enable movement and positioning of material carriers. The operation involves several key steps: first, the system receives a command or signal to initiate movement, which triggers the activation of drive mechanisms such as wheels or tracks. Next, the material handling unit, equipped with appropriate lifting or conveying devices, moves to the designated location. Once positioned, the system can then engage in material transfer, such as loading or unloading, using features like forks, pallets, or conveyor belts. The control system, often integrated with sensors and feedback loops, ensures precise positioning and operational safety, preventing collisions and maintaining stability during transit.
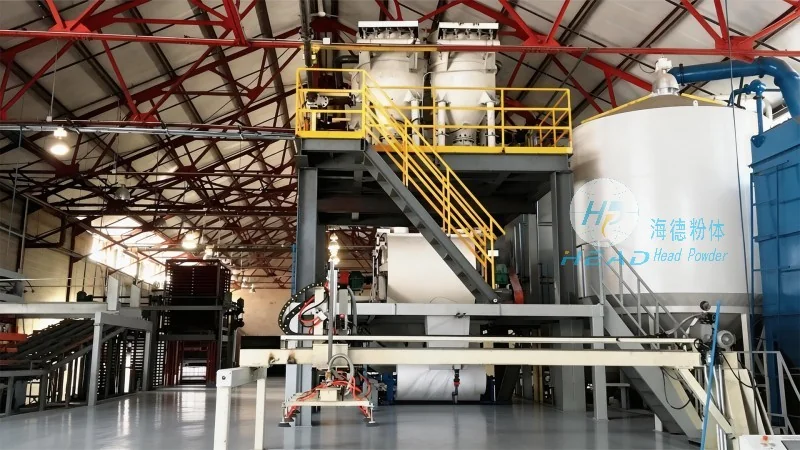
Key Features of Mobile Material Handling Systems
Mobile material handling systems are characterized by several distinct features that enhance their functionality and usability. One of the primary features is their mobility, which allows for the repositioning of material handling units as needed, eliminating the need for fixed infrastructure and enabling flexible workspace utilization. Another significant feature is the integration of advanced control technologies, including automated guidance systems and real-time monitoring capabilities. This enables operators to manage multiple units simultaneously and adjust operations based on real-time data. Additionally, these systems often incorporate safety features such as emergency stop buttons, collision avoidance sensors, and load capacity indicators to ensure safe and efficient operation. The design also emphasizes durability and reliability, with robust construction to withstand heavy-duty industrial environments and extended operational life.
Applications and Benefits in Industrial Settings
Mobile material handling systems find extensive applications across various industrial sectors, including manufacturing plants, distribution centers, and construction sites. In manufacturing, they are used to transport raw materials to production lines and move finished products to storage areas, streamlining the production process. In distribution centers, these systems enhance order picking and inventory management by allowing for the flexible movement of pallets and goods. The benefits of implementing mobile material handling systems are substantial, including increased operational efficiency, reduced labor costs, and improved safety. By automating material movement, companies can minimize manual handling tasks, lower the risk of workplace injuries, and optimize space utilization. Furthermore, the adaptability of these systems allows businesses to scale operations without significant capital investment in fixed infrastructure, providing a cost-effective solution for evolving production needs.
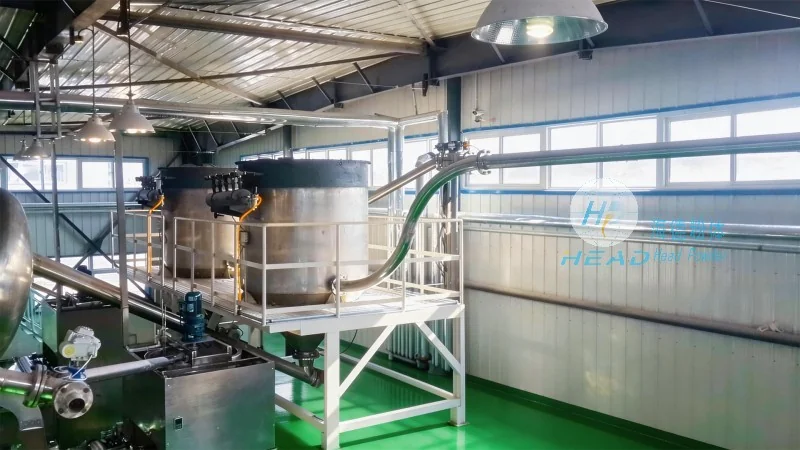
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of mobile material handling equipment, specializing in the design, development, and production of high-quality industrial solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the material handling industry. HeadPowder's products are engineered to meet the diverse needs of industrial clients, offering reliability, efficiency, and durability. The company's headquarters is located in Shandong, China, where it operates state-of-the-art manufacturing facilities and research centers. By leveraging advanced technology and a team of experienced engineers, HeadPowder continuously improves its product offerings to deliver cutting-edge solutions that enhance operational performance and safety in industrial environments.