

Working Principle and Characteristics of Potassium Hydroxide Material Handling
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the efficient and safe transportation of potassium hydroxide (KOH). Based in China, the company leverages advanced engineering solutions to address the unique challenges associated with handling this caustic chemical. This article explores the working principle and key characteristics of their material handling systems, offering insights into how they ensure optimal performance and operational safety.
The Working Principle of Potassium Hydroxide Material Handling Systems
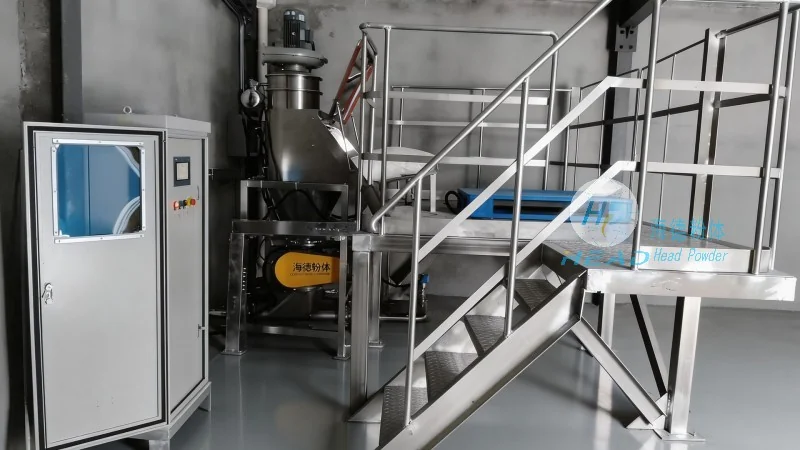
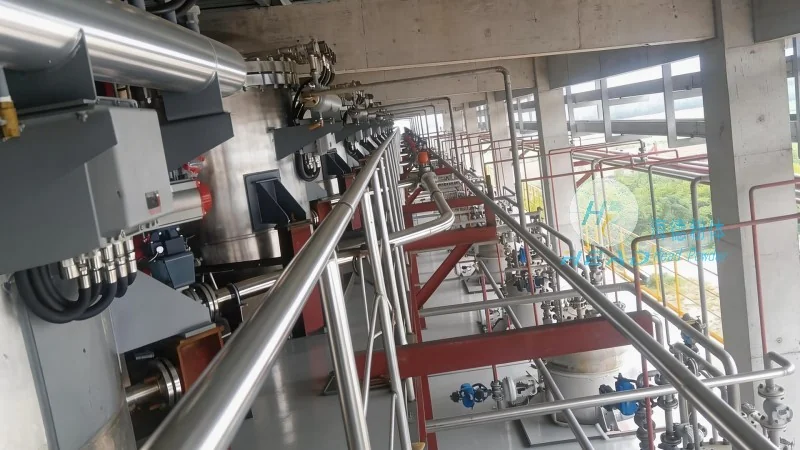
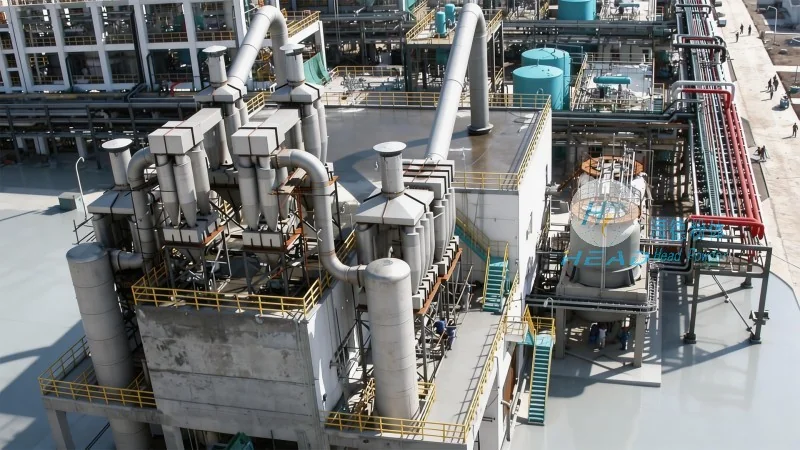
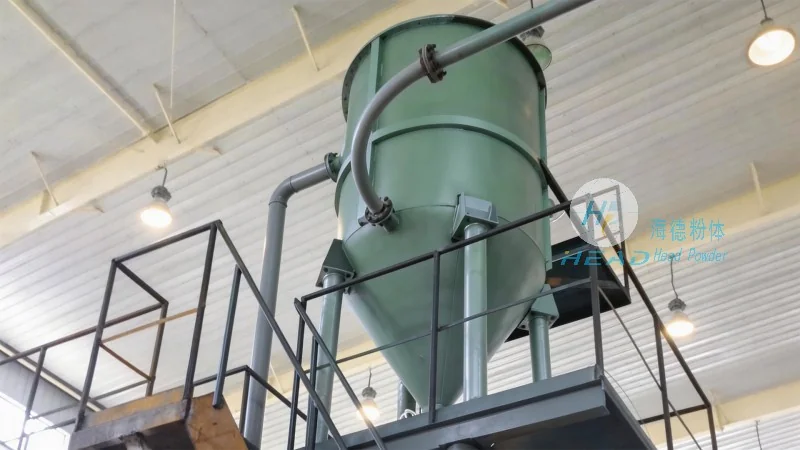
The material handling process for potassium hydroxide involves a series of integrated steps designed to maintain the chemical's integrity and ensure safe operation. At the core of the system is the use of specialized equipment such as conveyor belts, pumps, and storage tanks. The process typically begins with the loading of KOH from storage vessels into the handling equipment. Pneumatic or hydraulic systems may be employed to transfer the material, depending on the specific application and the volume of material being transported. The equipment is designed with corrosion-resistant materials, such as stainless steel, to withstand the aggressive nature of KOH and prevent contamination. Temperature control is also a critical aspect, as KOH can be sensitive to temperature fluctuations, which may affect its viscosity and handling properties. The system is equipped with sensors and monitoring devices to track the flow rate, pressure, and temperature in real-time, ensuring that the material is transported under optimal conditions. This closed-loop system minimizes the risk of spills and exposure, enhancing both safety and efficiency.
Key Characteristics of Potassium Hydroxide Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd. offers material handling solutions for potassium hydroxide that are characterized by several distinct features. First, the systems are engineered for high reliability and durability, with components designed to withstand continuous operation in harsh environments. The use of advanced materials and robust construction ensures long service life and minimal downtime. Second, the solutions prioritize safety, incorporating multiple layers of protection. This includes explosion-proof designs for equipment, emergency shut-off valves, and real-time monitoring systems that can detect and respond to abnormal conditions quickly. Third, the systems are highly customizable to meet the specific needs of different industries, such as chemical manufacturing, pharmaceuticals, or food processing. This adaptability allows for tailored solutions that optimize material flow and reduce operational costs. Fourth, the company emphasizes energy efficiency, with systems designed to minimize power consumption while maintaining performance. This not only reduces operational expenses but also aligns with sustainability goals. Finally, the material handling solutions are supported by comprehensive maintenance and support services, ensuring that clients receive ongoing assistance to keep their systems operating at peak performance.