

Working Principle and Features of High-Calcium Powder Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for high-calcium powder applications. With a focus on efficiency, reliability, and material integrity, the company’s solutions are engineered to meet the demanding requirements of industries that handle calcium-rich powders, such as cement, construction materials, and chemical processing.
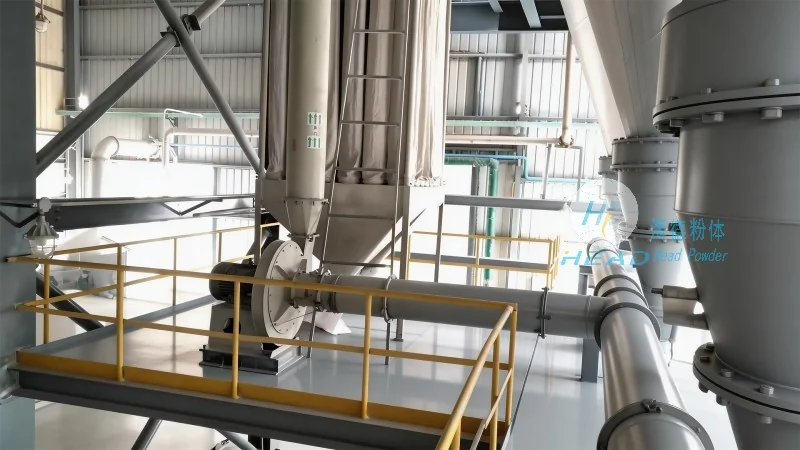
At the core of HeadPowder’s high-calcium powder pneumatic conveying systems is the pneumatic conveying technology, which utilizes air or gas to transport bulk materials through a pipeline network. This method offers a non-contact, continuous, and often dust-free alternative to traditional mechanical conveying methods, making it ideal for handling fine, abrasive, or sensitive powders like high-calcium materials.
Working Principle of High-Calcium Powder Pneumatic Conveying Systems
The working principle of these systems involves the generation of a pressure differential within a closed pipeline system. A blower or compressor creates a high-pressure air stream that draws the high-calcium powder from the source hopper into the pipeline. The powder is then suspended in the air stream and transported to the destination point, such as a storage silo, processing unit, or packaging line. The system typically includes components like a feed hopper, rotary valve, air lock, and a receiver, all working in tandem to ensure smooth and consistent material flow.
Key Features of High-Calcium Powder Pneumatic Conveying Systems
HeadPowder’s high-calcium powder pneumatic conveying systems are characterized by several key features that enhance performance and operational efficiency. Firstly, the systems are designed for high material throughput, capable of handling large volumes of high-calcium powder while maintaining consistent flow rates. This is achieved through optimized pipeline design, appropriate air velocity, and efficient feeding mechanisms. Secondly, the systems prioritize material integrity, minimizing particle degradation, agglomeration, or contamination during transport. This is crucial for high-calcium powders, which are often sensitive to handling conditions and require preservation of their physical and chemical properties.
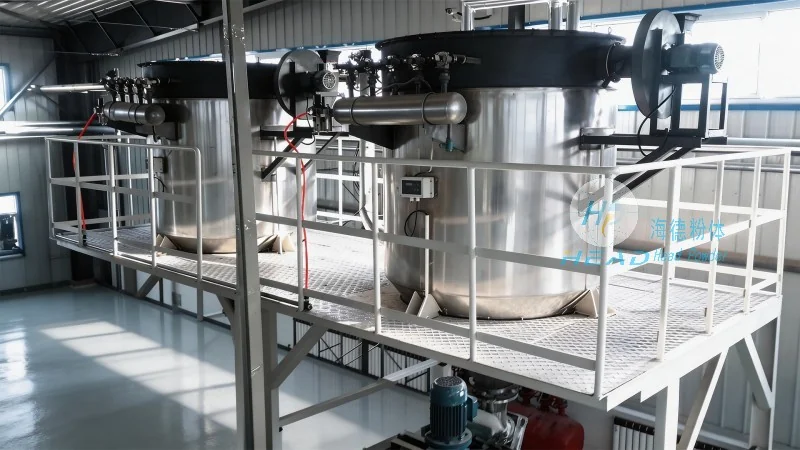
Thirdly, the systems offer flexibility in system configuration, allowing for both positive and negative pressure operation, as well as multi-point delivery or collection. This adaptability enables customization to fit specific plant layouts and material handling requirements. Additionally, the systems incorporate advanced control systems that monitor pressure, flow rate, and air consumption, providing real-time feedback and enabling automated adjustments to maintain optimal performance. Safety features, such as explosion-proof designs and dust suppression mechanisms, are also integrated to ensure compliance with industrial safety standards.
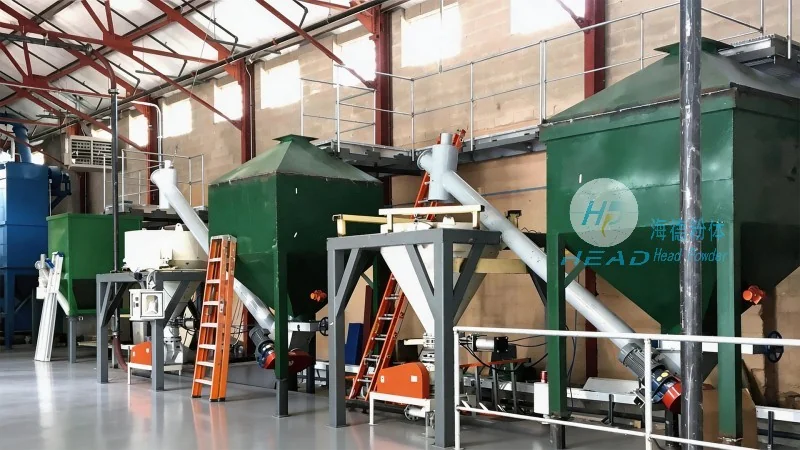
Benefits of Implementing High-Calcium Powder Pneumatic Conveying Systems
Adopting a high-calcium powder pneumatic conveying system from HeadPowder brings numerous benefits to industrial operations. The primary advantage is the reduction in labor costs and operational downtime, as the automated system minimizes the need for manual handling and reduces the risk of material spills or blockages. Furthermore, the systems enhance process efficiency by ensuring consistent material supply to downstream processes, which improves production output and reduces waste. The non-contact nature of the conveying method also reduces equipment wear and tear, leading to lower maintenance costs over the system’s lifespan.
Another significant benefit is the improvement in workplace safety and environmental compliance. By eliminating the need for manual handling of high-calcium powders, the systems reduce exposure to dust and airborne particles, thereby lowering the risk of respiratory issues and other health hazards. Additionally, the enclosed pipeline system prevents dust emissions, contributing to a cleaner and more environmentally friendly operation. This is particularly important for high-calcium powders, which can be hazardous if released into the environment.