

Principles and Application Scenarios of Dust-Free Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free pneumatic conveying systems. These systems are engineered to efficiently transport bulk materials while maintaining a completely dust-free environment, making them ideal for industries where contamination control is paramount.
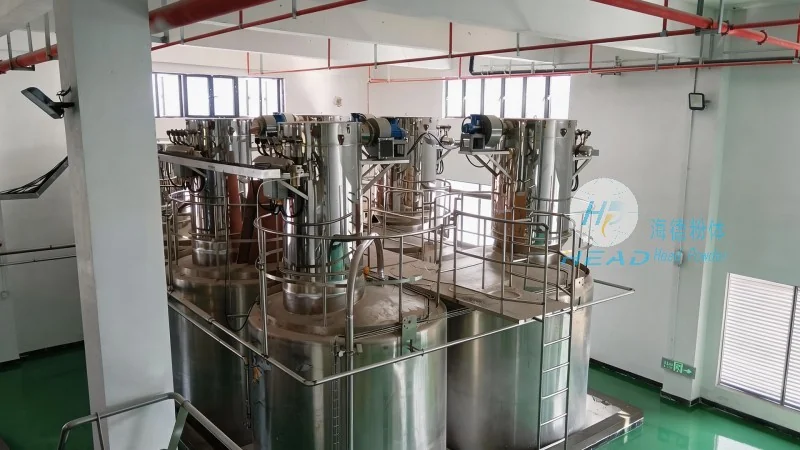
Principles of Dust-Free Pneumatic Conveying
The core principle of pneumatic conveying involves using compressed air or other gases to move bulk materials through a sealed pipeline system. In a dust-free design, the entire system is enclosed to prevent any material from escaping into the surrounding environment. This is achieved through a combination of sealed hoppers, flexible hoses, and positive pressure or negative pressure systems, depending on the specific application requirements. The system typically includes a material feed hopper, a conveyor line, and a discharge unit, all integrated to ensure a continuous and controlled flow of material.
One of the key advantages of this technology is its ability to handle a wide range of materials, from fine powders to granules, without the need for mechanical components that could cause wear or contamination. The sealed design also eliminates the risk of dust exposure, which is critical in industries such as pharmaceuticals, food processing, and electronics manufacturing where product purity and worker safety are non-negotiable.
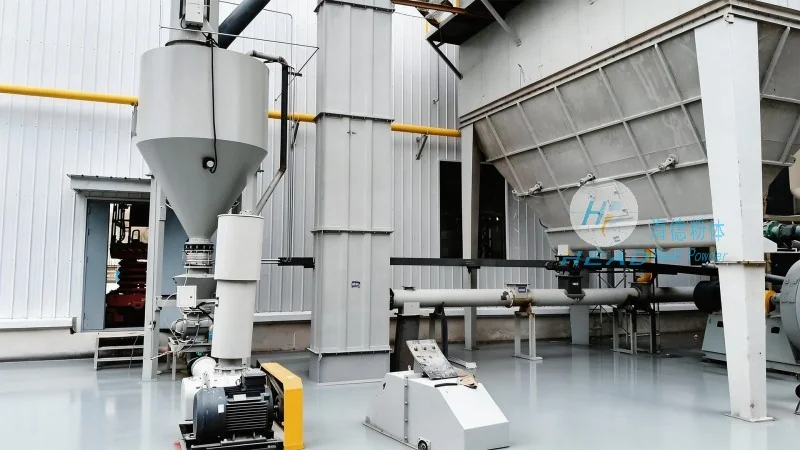
Working Scenarios and Industry Applications
Dust-free pneumatic conveying systems are widely used across various industries due to their versatility and efficiency. In the pharmaceutical industry, these systems are essential for transporting active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the final product remains free from contaminants. The sealed environment prevents cross-contamination and maintains the integrity of the product throughout the conveying process.
In the food processing sector, especially for products like flour, sugar, and spices, dust-free conveying is crucial to meet stringent hygiene standards and prevent product spoilage. The systems are designed to be easy to clean and maintain, with smooth surfaces and no dead zones where dust can accumulate. This makes them suitable for applications in bakeries, snack food manufacturers, and other food-related operations.
Chemical and petrochemical industries also benefit from dust-free pneumatic conveying, particularly when handling hazardous or reactive powders. The sealed system prevents the release of harmful substances into the workplace, reducing the risk of accidents and ensuring compliance with safety regulations. Additionally, the technology allows for precise control over material flow, which is vital for processes that require consistent dosing and mixing.
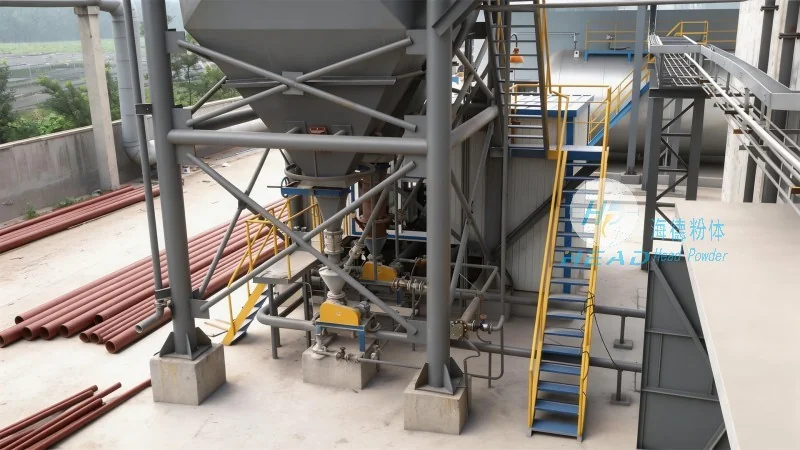
Other industries that find these systems advantageous include the plastics and rubber sectors, where materials like resin and rubber powder need to be transported without contamination. The ability to handle different particle sizes and densities makes the system adaptable to various production lines. In the agricultural industry, dust-free conveying is used for handling grain and other bulk agricultural products, improving efficiency and reducing the risk of dust-related health issues for workers.
Key Features and Advantages
HeadPowder's dust-free pneumatic conveying systems are equipped with several features that enhance their performance and reliability. These include variable speed drives for precise control over material flow, pressure sensors to monitor system performance, and automatic shut-off valves to prevent backflow and material spillage. The systems are also designed with energy efficiency in mind, using optimized air pressure settings to minimize energy consumption while maintaining the required conveying capacity.
Another significant advantage is the reduced maintenance requirements compared to traditional mechanical conveying systems. Since there are no moving parts in direct contact with the material, the wear and tear are minimal, leading to lower operational costs and longer system lifespans. The sealed design also simplifies cleaning procedures, as the entire system can be flushed with cleaning agents without exposing the environment to dust.
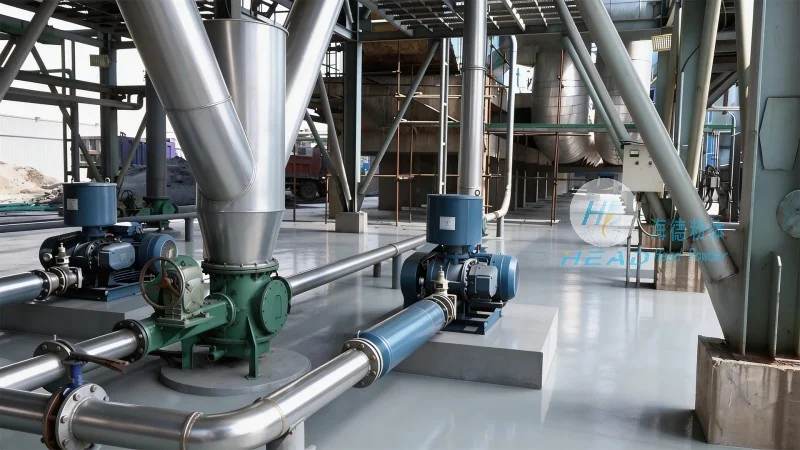
Furthermore, the systems are scalable and can be customized to meet the specific needs of different applications. Whether a small-scale operation or a large industrial plant, HeadPowder can provide a tailored solution that optimizes material handling while maintaining the highest standards of dust control and safety.
Conclusion
Dust-free pneumatic conveying systems represent a sophisticated solution for bulk material transport in industries where contamination control and worker safety are critical. By combining advanced engineering with a sealed design, these systems offer a reliable and efficient method for moving materials while maintaining a clean environment. HeadPowder, with its expertise and commitment to quality, continues to be a trusted partner for businesses seeking to implement effective and sustainable material handling solutions.