

Principle and Working Scene Characteristics of Bulk Bag Unloading Station Pneumatic Conveying System
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and supply of advanced pneumatic conveying systems tailored for bulk bag unloading stations. These systems are engineered to efficiently transfer bulk materials from large capacity bags into processing or storage facilities, ensuring seamless material handling operations.
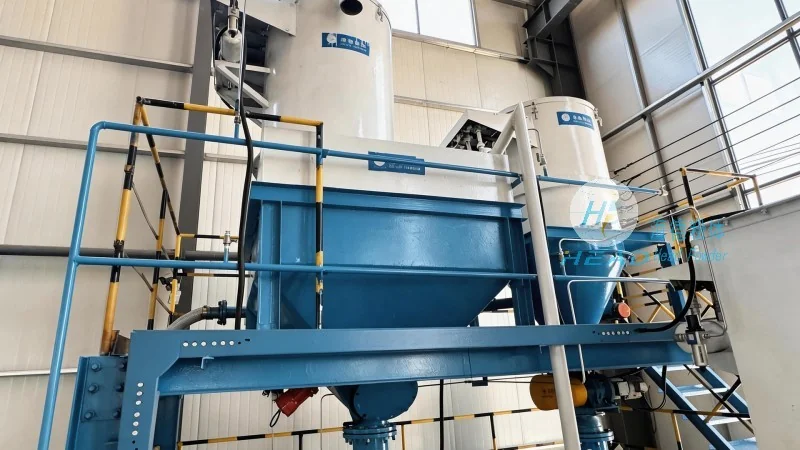
Principle of Pneumatic Conveying Systems
The core principle of pneumatic conveying systems for bulk bag unloading involves the use of air as the conveying medium to transport bulk materials. The system typically consists of a hopper, a vacuum or pressure pump, and a pipeline network. When a bulk bag is placed in the hopper, the pump creates a pressure differential that draws the material into the pipeline. The material is then transported to the desired destination, such as a silo or processing unit, where it is discharged. This method eliminates the need for manual handling, reducing labor costs and improving safety in industrial environments.
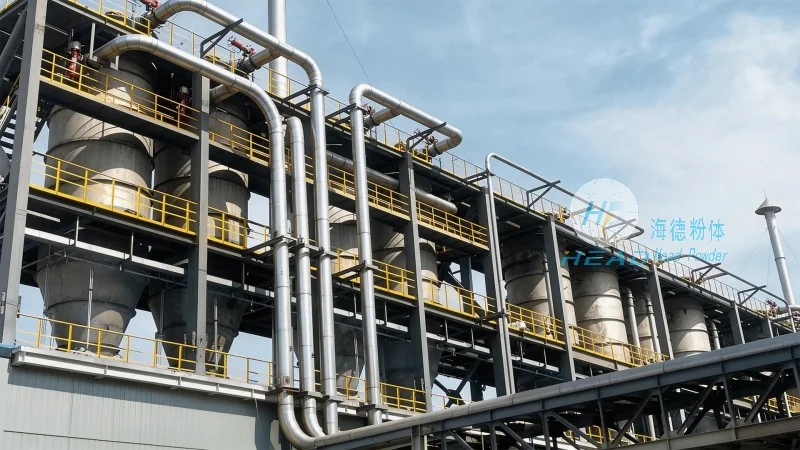
Working Scene Characteristics
Bulk bag unloading stations equipped with pneumatic conveying systems are commonly found in various industrial sectors, including chemical, food, pharmaceutical, and mining industries. The primary characteristics of these working scenes include high material throughput, minimal downtime, and the ability to handle a wide range of bulk materials, from powders to granules. The systems are designed to operate in both indoor and outdoor settings, with options for dust collection and filtration to maintain air quality and comply with environmental regulations. Additionally, the modular design of these systems allows for easy integration into existing production lines, providing flexibility and scalability for growing industrial needs.
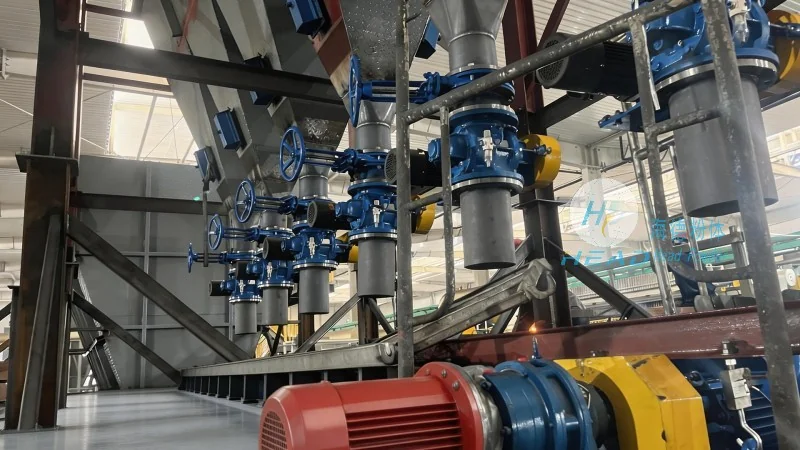
Company Overview
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable company dedicated to providing innovative material handling solutions. With a strong focus on research and development, the company has developed advanced pneumatic conveying systems that meet the highest standards of efficiency and reliability. HeadPowder's products are manufactured with precision engineering, ensuring durability and long-term performance in demanding industrial applications. The company's commitment to quality and customer satisfaction has established it as a trusted partner for businesses seeking efficient bulk material handling solutions.
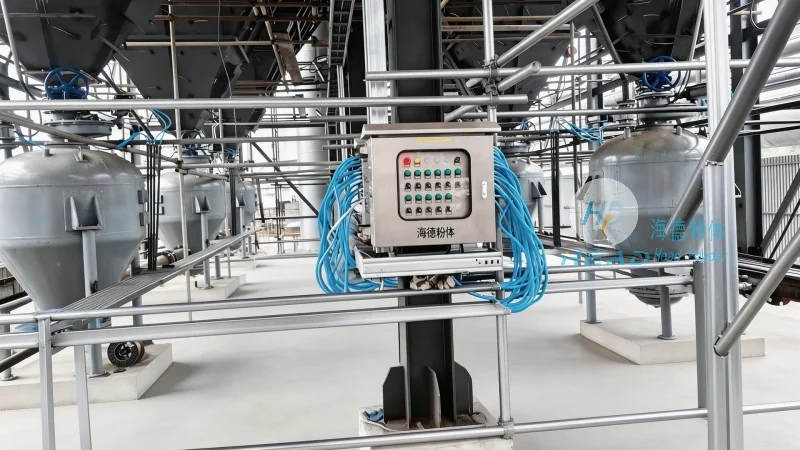
Application Examples
In practical applications, the pneumatic conveying systems for bulk bag unloading stations are used to handle materials such as cement, flour, plastic pellets, and chemical powders. For instance, in a chemical plant, these systems efficiently transfer raw materials from bulk bags into reactors, while in a food processing facility, they ensure hygienic and safe transfer of ingredients. The systems are also employed in mining operations to transport ore from storage bags to processing equipment, optimizing the material flow and reducing operational costs. These examples highlight the versatility and effectiveness of pneumatic conveying systems in diverse industrial scenarios.