

Principles and Application Scenarios of Coke Powder Conveying
Exploring the fundamental principles and operational characteristics of coke powder conveying systems is essential for optimizing material handling in industrial applications. This article delves into the core mechanisms that enable the efficient transport of coke powder and examines the diverse work environments where such systems are deployed, providing insights into their design, functionality, and practical implementation.
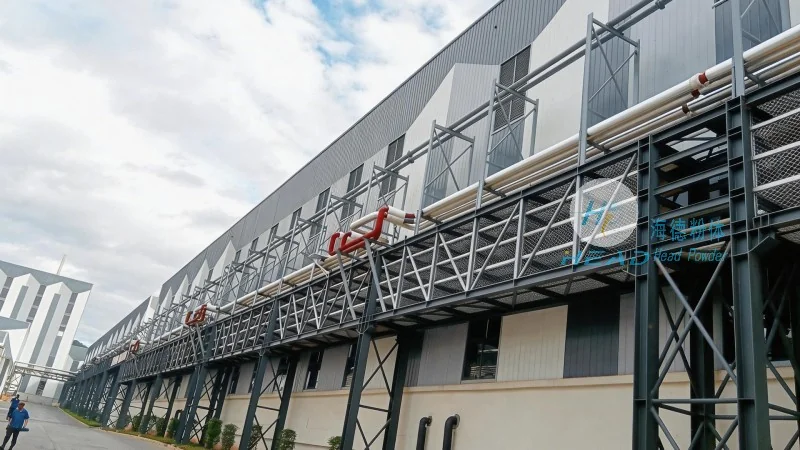
Overview of Coke Powder Conveying Systems
Coke powder conveying involves the movement of fine coke particles from processing units to storage or end-use locations within industrial facilities. The process relies on a combination of physical forces, including gravity, pressure differentials, and mechanical or pneumatic action. These systems are engineered to ensure consistent flow rates, minimize material loss, and maintain product integrity throughout the transportation process. Key components typically include feed hoppers, conveyors (such as screw, belt, or pneumatic pipelines), control valves, and monitoring equipment that regulate the flow and pressure of the material.
Core Principles of Coke Powder Conveying
The effectiveness of coke powder conveying is governed by several critical principles. First, particle size and density significantly influence the choice of conveying method. Fine, powdery coke particles often require pneumatic systems to prevent clogging and ensure smooth transport, as these systems can handle small particles with minimal resistance. In contrast, larger or bulkier coke particles may be better suited for mechanical conveyors like screw or belt systems, which rely on mechanical force to move material. Second, the principle of pressure differentials is central to pneumatic conveying, where compressed air creates a pressure gradient that propels the powder through pipelines. This method is particularly effective for long-distance or high-volume transport, as it can move large quantities of material efficiently over extended distances. Third, gravity-assisted conveyors, such as inclined screw or belt conveyors, leverage the natural weight of the material to facilitate movement, often used in shorter distances or when energy efficiency is a priority. Additionally, the control of moisture content and particle agglomeration is essential to prevent blockages and ensure consistent performance, as moisture can cause clumping and reduce flow rates.
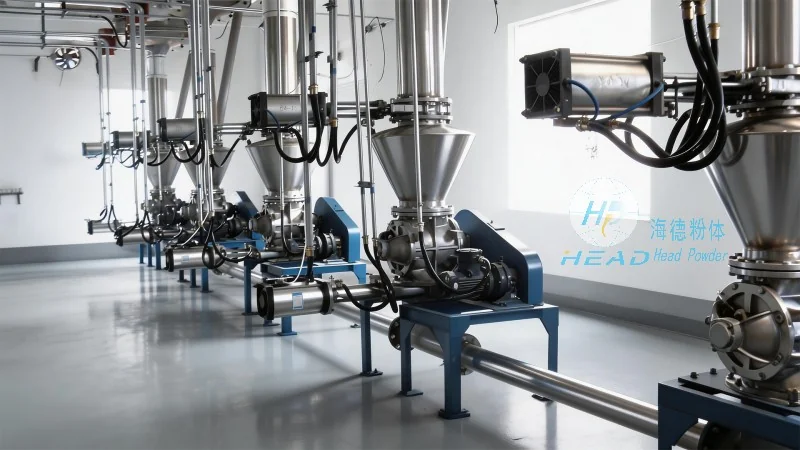
Diverse Application Scenarios and Operational Environments
The application scenarios for coke powder conveying vary widely across different industrial sectors, each presenting unique challenges and requirements. In steel manufacturing plants, for example, coke powder is a critical fuel used in blast furnaces, and efficient conveying systems are vital to maintain production continuity. The work environment in such settings is characterized by high temperatures, heavy machinery, and the need for reliable, high-capacity transport solutions that can handle abrasive and hot materials. Another key application is in the coke production sector, where coke powder is transported from processing units to storage silos or shipping facilities. Here, the system must handle varying particle sizes and maintain low dust emissions to comply with environmental regulations and ensure worker safety. In addition, the use of coke powder in chemical and metallurgical processes requires precise control over flow rates and particle distribution, often necessitating advanced control systems integrated with the conveying equipment to achieve consistent results.
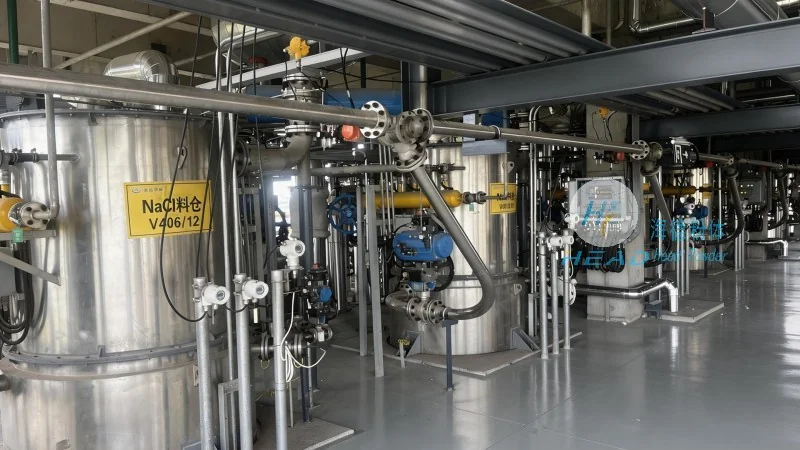
Work Environment and Safety Considerations
The operational environment of coke powder conveying systems is typically industrial and demanding, with considerations for safety and efficiency being paramount. Dust control is a critical aspect, as coke powder can generate significant airborne particles that pose health risks (such as respiratory issues) and environmental hazards (like air pollution). Advanced filtration systems and enclosed conveyor designs are commonly employed to minimize dust emissions and ensure compliance with occupational health and safety standards. Additionally, the mechanical integrity of the conveying equipment is essential, as coke powder can be abrasive and may cause wear on components like pipelines, screws, and bearings. Regular maintenance and the use of durable materials, such as stainless steel or specialized coatings, are necessary to extend the lifespan of the equipment and maintain optimal performance. The control systems in these applications often include sensors for monitoring flow rates, pressure, and temperature, providing real-time data to operators and enabling proactive adjustments to maintain system efficiency and prevent failures.
HeadPowder Engineering's Expertise in Coke Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing comprehensive coke powder conveying solutions tailored to the diverse needs of industrial clients. With a focus on innovation and reliability, HeadPowder designs and manufactures systems that integrate the principles discussed above, ensuring efficient and safe transport of coke powder. The company's expertise lies in understanding the unique challenges of each application scenario, from high-temperature steel plants to chemical processing facilities, and developing customized solutions that meet specific operational requirements. By leveraging advanced engineering and quality control processes, HeadPowder delivers systems that enhance productivity, reduce downtime, and improve overall material handling efficiency. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the coke powder conveying industry, serving clients across China and beyond. HeadPowder's solutions are designed to adapt to varying particle sizes, flow rates, and environmental conditions, ensuring that industrial facilities can achieve optimal performance and compliance with industry standards.