

Principle and Application Scenarios of Continuous Quantitative Powder Conveying Systems
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China, specializing in the design, development, and production of advanced powder conveying systems. The company focuses on providing efficient and reliable solutions for continuous quantitative powder handling in various industrial applications.
Principle of Continuous Quantitative Powder Conveying Systems
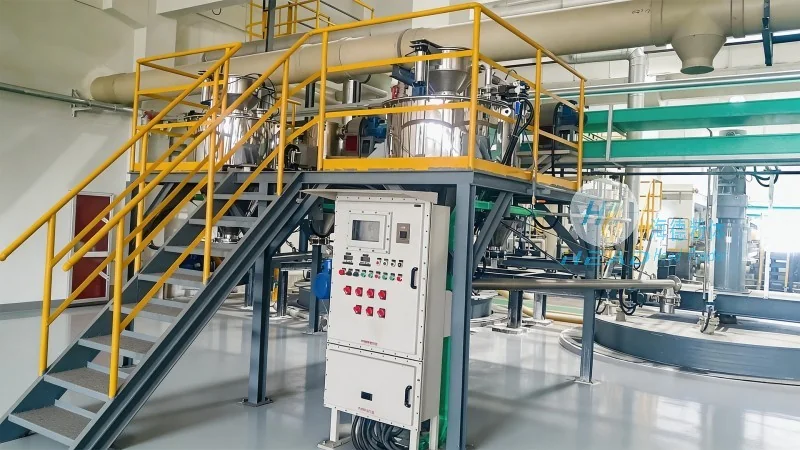
Continuous quantitative powder conveying systems operate on the principle of controlled, steady-state material flow. These systems are engineered to transport bulk powders, such as chemicals, food ingredients, pharmaceuticals, and industrial raw materials, with high precision and minimal loss. The core components typically include a feeding mechanism, a conveying device (like a screw conveyor, pneumatic system, or belt conveyor), and a control unit that regulates the flow rate. The feeding mechanism ensures a consistent supply of material, while the conveying device moves the powder through the system. The control unit, often equipped with sensors and digital controls, monitors and adjusts the flow rate to achieve the desired quantity. This closed-loop system minimizes variability in the output, ensuring that the delivered powder meets the required specifications for each application.
Key Features and Application Scenarios
Continuous quantitative powder conveying systems are characterized by several key features that make them suitable for diverse industrial environments. One of the primary advantages is their ability to handle large volumes of material with high accuracy, reducing the risk of over or under-dosing. The systems are designed for continuous operation, which enhances productivity and reduces downtime compared to batch processing methods. Additionally, these systems are often equipped with dust control measures, ensuring a clean and safe working environment. The flexibility of the conveying devices allows for adaptation to different powder types and particle sizes, making them versatile for various industries.
Common Application Scenarios
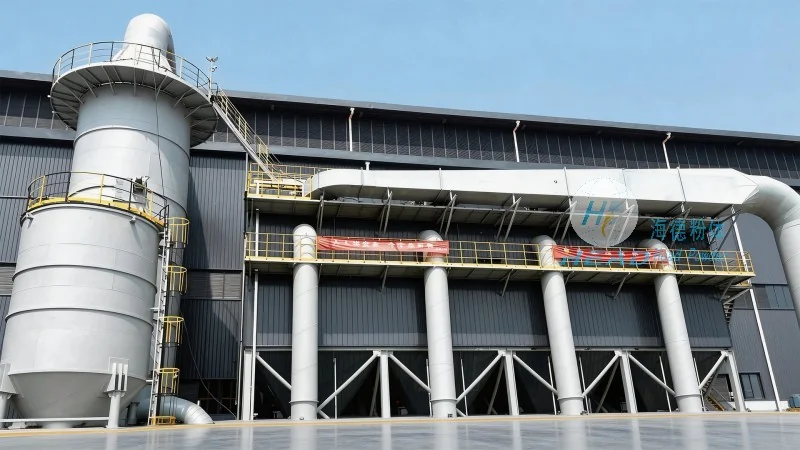
These systems are widely used in several industrial sectors, including pharmaceutical manufacturing, food processing, chemical production, and mining. In pharmaceuticals, continuous quantitative conveyors are essential for transporting active pharmaceutical ingredients (APIs) and excipients with strict purity and dosage requirements. The precision of the system ensures that each batch meets regulatory standards, minimizing the risk of contamination or dosage errors. In food processing, the systems handle ingredients like flour, sugar, and spices, maintaining consistent quality and preventing cross-contamination. Chemical manufacturers use these systems to transport raw materials and intermediates, ensuring safe and efficient processing. Mining and mineral processing industries benefit from the systems' ability to handle abrasive and heavy-duty powders, such as ores and minerals, with minimal wear and tear on equipment.
Advantages in Industrial Operations
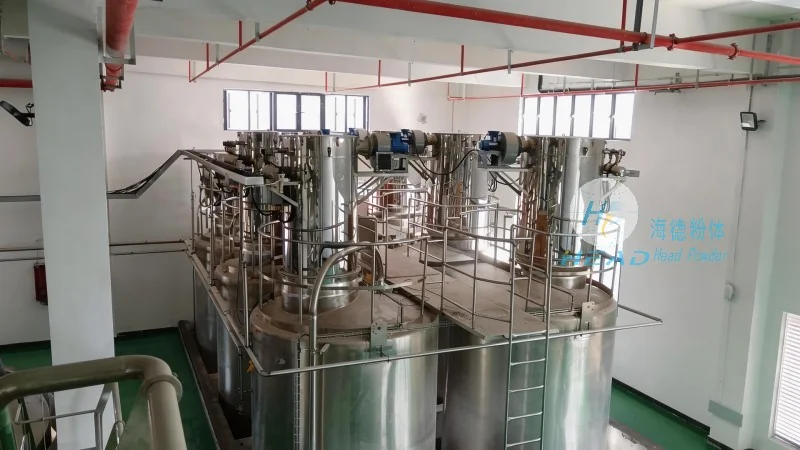
Implementing continuous quantitative powder conveying systems offers significant benefits to industrial operations. The primary advantage is improved process control, which leads to higher product quality and reduced waste. By maintaining a consistent flow rate, the systems help in achieving uniform product characteristics, which is crucial in industries where product consistency is paramount. Another advantage is increased efficiency, as continuous operation allows for uninterrupted production, reducing the time and labor required for manual handling. The systems also contribute to cost savings by minimizing material loss and reducing the need for reprocessing. Furthermore, the automation features of these systems enhance safety by reducing human intervention in potentially hazardous environments, such as those involving toxic or reactive powders.
HeadPowder's Commitment to Quality and Innovation
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality continuous quantitative powder conveying systems that meet the evolving needs of modern industries. The company leverages advanced engineering and manufacturing techniques to ensure that each system is tailored to the specific requirements of its clients. With a focus on precision, reliability, and efficiency, HeadPowder's products are designed to enhance operational performance and contribute to the success of industrial processes. By combining technical expertise with customer-centric solutions, the company aims to provide sustainable and effective powder handling solutions for a wide range of applications.