

Operation Process and Working Principle of Tonne Bag Powder Conveying System Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder conveying systems. The company's core product, the tonne bag powder conveying system, is engineered to efficiently handle bulk powder materials from large-scale storage to processing facilities. This equipment is crucial for industries such as chemicals, food, and pharmaceuticals, where precise and reliable material transfer is essential for operational efficiency and product quality.
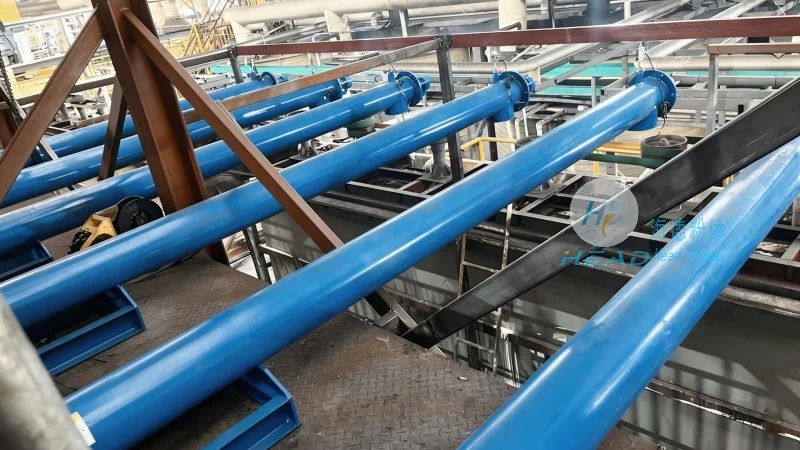
Overview of the Tonne Bag Powder Conveying System
The tonne bag powder conveying system is a comprehensive solution that integrates multiple components to streamline the handling of bulk powders. At its core, the system is designed to receive, weigh, and transfer powder from tonne bags into processing lines or storage silos. The equipment is built with durability and efficiency in mind, utilizing robust materials and advanced control technologies to ensure consistent performance under various operational conditions.
Key Components and Their Functions
The system typically consists of several key components, each playing a critical role in the overall operation. These include the receiving hopper, which captures the tonne bag and allows for easy discharge; a weighing scale to accurately measure the material load; a discharge valve to control the release of powder; and a conveyor system, such as a screw or pneumatic conveyor, to transport the material to its destination. Additionally, the system may incorporate a dust collection system to maintain a clean and safe working environment, as well as a control panel to monitor and adjust the operation in real-time.
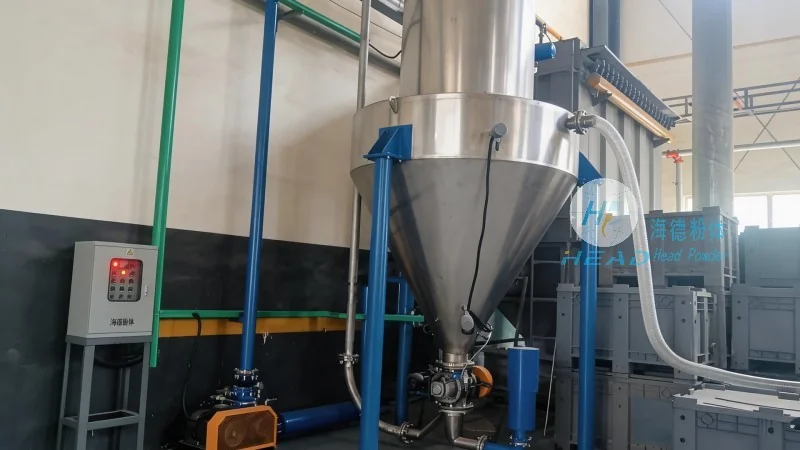
Operation Process: Step-by-Step
The operation of the tonne bag powder conveying system follows a systematic process to ensure smooth and efficient material handling. The process begins with the placement of a tonne bag into the receiving hopper. The hopper then seals the bag, preventing material spillage and dust contamination. Next, the weighing scale measures the exact weight of the powder, providing data for inventory management and process control. Once the weighing is complete, the discharge valve opens, allowing the powder to flow into the conveyor system. The conveyor then transports the material to the processing line or storage silo, where it is further processed or stored. Throughout this process, the control panel continuously monitors parameters such as flow rate, pressure, and temperature, ensuring optimal performance and safety.
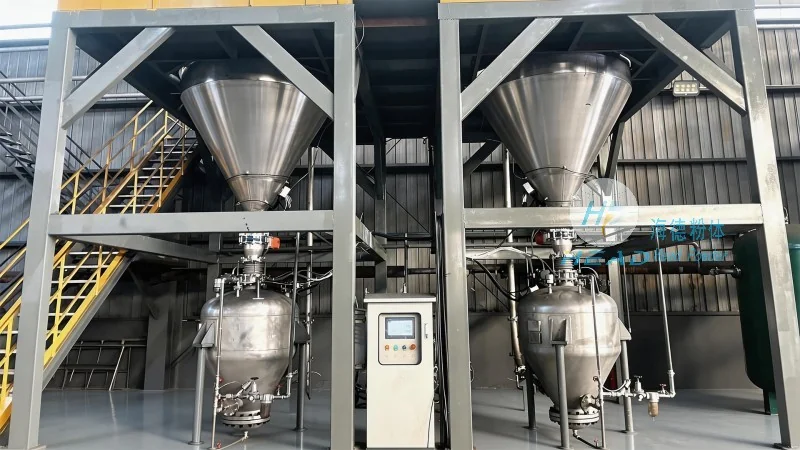
Working Principle: Mechanical and Control Systems
The working principle of the tonne bag powder conveying system combines mechanical engineering with advanced control technologies to achieve precise material handling. The mechanical components, including the hopper, weighing scale, and conveyor, work in tandem to move the powder from the bag to the processing line. The weighing scale uses load cells to measure the weight of the material, converting the force into an electrical signal that is processed by the control system. The control system then adjusts the operation of the conveyor and other components based on the measured data, ensuring that the material is transferred at the correct rate and under optimal conditions. Additionally, the system may incorporate sensors to detect blockages or other issues, triggering alarms or automatic shutdowns to prevent damage to the equipment or material loss.
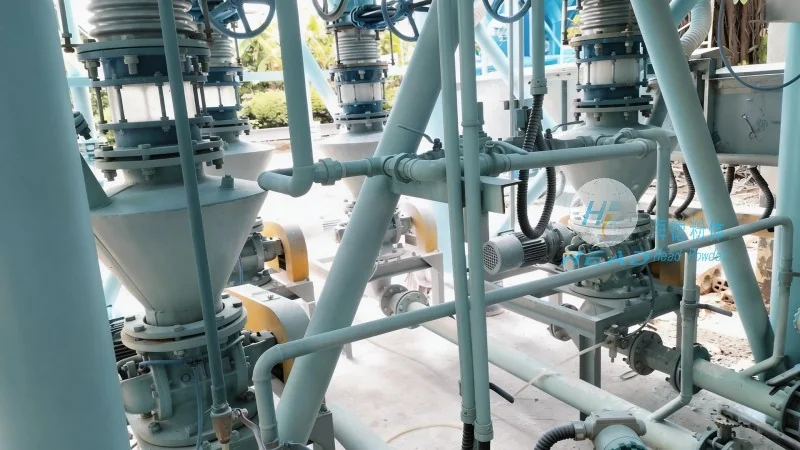
Benefits and Applications
The tonne bag powder conveying system offers numerous benefits for industries that handle bulk powders. The system enhances operational efficiency by reducing manual labor and minimizing material loss. It also improves product quality by ensuring consistent and accurate material transfer, which is critical for processes such as mixing, blending, and packaging. The system is particularly suitable for applications where large quantities of powder need to be handled, such as in chemical manufacturing, food processing, and pharmaceutical production. By integrating the system into their operations, companies can achieve higher productivity, lower costs, and improved safety.
Conclusion
HeadPowder's tonne bag powder conveying system is a reliable and efficient solution for handling bulk powders. The system's design and operation are based on proven engineering principles, ensuring that it meets the needs of various industries. With its robust construction, advanced control technologies, and comprehensive features, the system provides a cost-effective and reliable method for material transfer. As a leading manufacturer in Shandong, China, HeadPowder continues to innovate and improve its products to meet the evolving needs of the market. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking to enhance their material handling capabilities.