

Operation Process and Working Principle of Rare Earth Powder Material Handling Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and implementation of efficient rare earth powder material handling systems. These systems are engineered to ensure safe, reliable, and high-performance transportation of rare earth powders, which are critical components in various industrial applications.
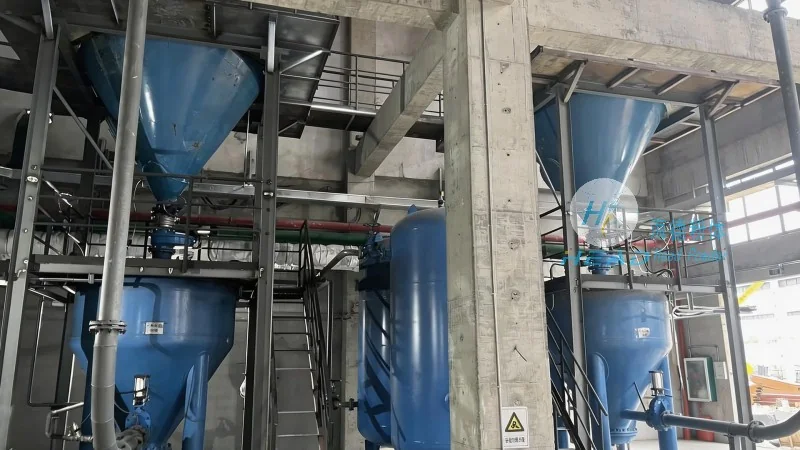
Overview of Rare Earth Powder Material Handling Systems
At the core of the system is a comprehensive solution tailored to the unique properties of rare earth powders, such as their fine particle size, chemical reactivity, and potential for dust generation. The design incorporates advanced technologies to address challenges like material segregation, caking, and environmental safety, ensuring optimal performance in demanding industrial environments.
Key Components and Their Roles
The rare earth powder material handling system typically consists of several interconnected components, each playing a vital role in the overall operation. These include feeders, conveyors, storage silos, and control systems. The feeders are responsible for accurately metering the powder, while the conveyors transport it to the next stage. Storage silos provide bulk storage, and the control systems monitor and regulate the entire process to maintain consistent flow and quality.
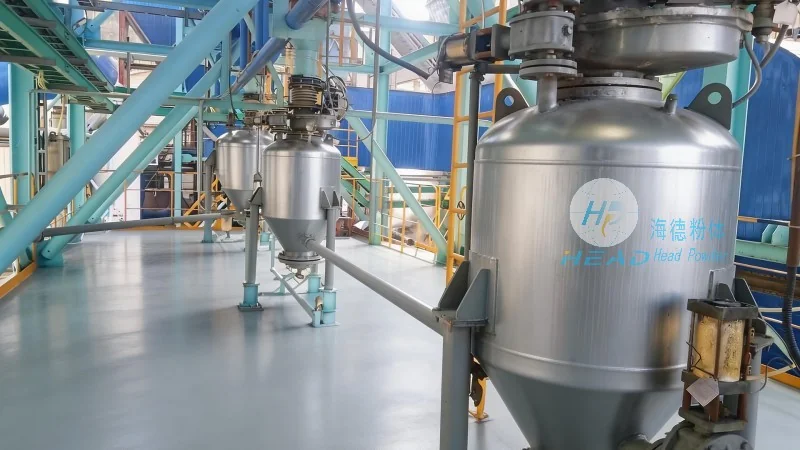
Operation Process: Step-by-Step Workflow
The operation of the rare earth powder material handling system follows a systematic workflow designed to maximize efficiency and minimize downtime. The process begins with the loading of raw rare earth powder into the storage silo. From there, the powder is discharged into a feeder, which regulates the flow rate based on the system's requirements. The feeder then transfers the powder to a conveyor system, which transports it to the processing or packaging area. Throughout this process, sensors and control devices continuously monitor parameters such as flow rate, pressure, and temperature to ensure the system operates within safe and optimal parameters.
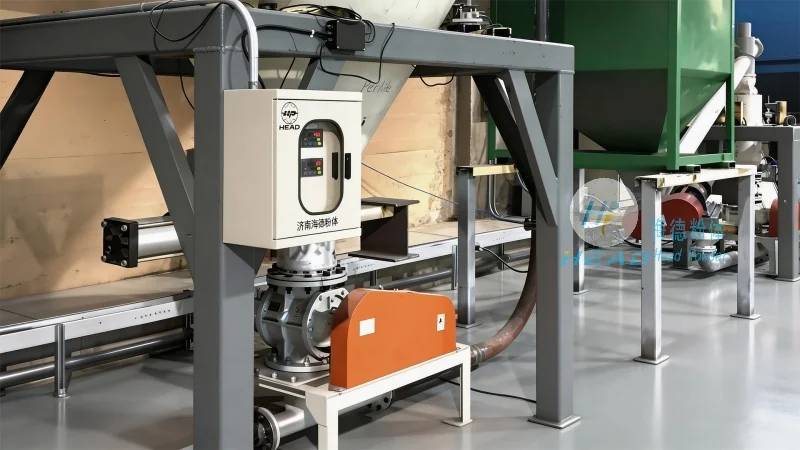
Working Principle: How the System Ensures Efficiency
The working principle of the rare earth powder material handling system is based on the principles of fluidization and pneumatic transport, depending on the specific design. For systems using pneumatic conveyors, the powder is carried by a stream of air, which reduces friction and prevents material degradation. The system may also incorporate mechanical conveyors, such as screw or belt conveyors, for horizontal or vertical transport. In either case, the design prioritizes minimizing material degradation, maintaining particle size distribution, and preventing contamination, which are critical for the quality of the final product.
Advantages and Applications
HeadPowder's rare earth powder material handling systems offer several advantages, including high capacity, low maintenance, and enhanced safety features. These systems are widely used in industries such as electronics, automotive, and renewable energy, where rare earth elements are essential for manufacturing components like magnets, catalysts, and batteries. The systems are designed to meet the specific needs of each application, ensuring that the material is handled with precision and care.