

Application of Pneumatic Conveying in the Handling of Sintered Ash Bulk Materials
When it comes to the efficient and reliable transport of bulk materials like sintered ash, pneumatic conveying systems offer a superior solution. This technology has become increasingly vital in industrial settings where the safe and effective movement of such materials is critical. The application of pneumatic conveying in sintered ash handling not only enhances operational efficiency but also ensures compliance with environmental and safety standards.
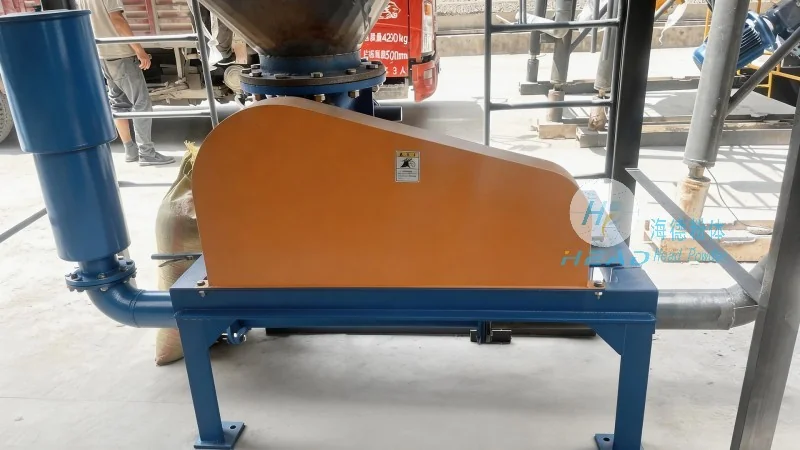
Understanding Sintered Ash and Its Handling Challenges
Sintered ash, a byproduct of industrial processes such as steel production, presents unique challenges when it comes to bulk material handling. Its granular nature, varying moisture content, and potential for dust generation require specialized equipment and systems to manage. Traditional methods like belt conveyors or bucket elevators may struggle with the abrasive properties and potential health hazards associated with sintered ash. This is where pneumatic conveying technology steps in, providing a more controlled and hygienic approach to material transport.
How Pneumatic Conveying Works in Sintered Ash Handling
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. In the context of sintered ash, these systems can be designed as either pressure or vacuum-based systems, depending on the specific application requirements. The process involves feeding the sintered ash into a hopper, where it is then drawn or pushed through the pipeline by the air flow. This method allows for the continuous and unobstructed movement of materials over long distances, minimizing the need for intermediate storage and handling points.
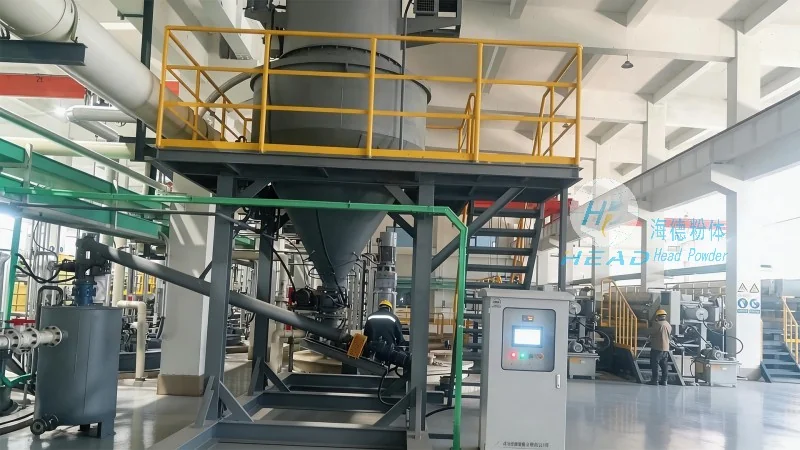
Key Benefits of Using Pneumatic Conveying for Sintered Ash
Implementing pneumatic conveying for sintered ash handling offers several key advantages. Firstly, it significantly reduces the risk of dust exposure and associated health hazards, as the material is contained within the pipeline system. Secondly, the technology provides a more hygienic and clean environment, which is particularly important in facilities where material contamination could impact downstream processes. Additionally, pneumatic conveying systems can handle materials with varying particle sizes and moisture levels, making them highly versatile. The energy efficiency of these systems also contributes to lower operational costs over time.
HeadPowder Engineering's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of sintered ash handling. With years of experience in the industry, HeadPowder has developed a comprehensive range of solutions that address the specific challenges associated with sintered ash transport. The company's expertise lies in customizing systems to ensure optimal performance, reliability, and safety, while adhering to industry standards and regulations.
Customized Pneumatic Conveying Systems for Sintered Ash Applications
HeadPowder understands that each sintered ash handling operation has distinct requirements. Therefore, the company offers customized pneumatic conveying systems that can be tailored to specific site conditions, material characteristics, and operational goals. These systems may include components such as high-capacity feeders, robust pipeline networks, and advanced control systems to ensure smooth and continuous material flow. The company's engineering team works closely with clients to assess their needs and develop solutions that maximize efficiency and minimize downtime.
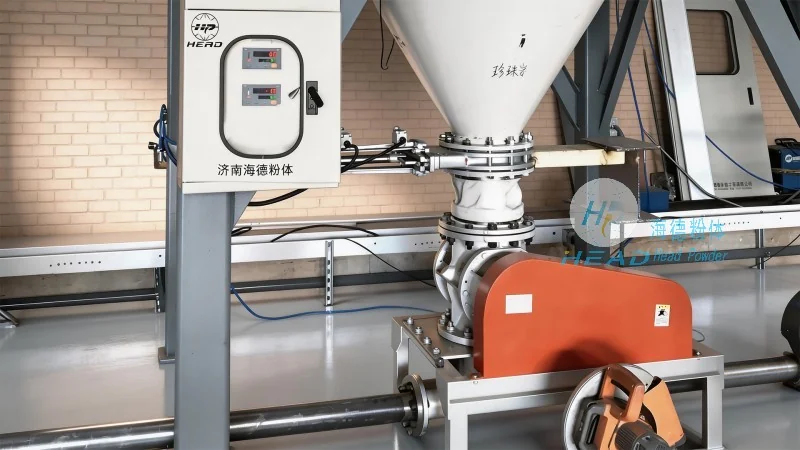
Ensuring Reliability and Durability in Sintered Ash Handling
For industrial operations, the reliability and durability of the conveying system are paramount. HeadPowder's pneumatic conveying systems are built with high-quality materials and components that can withstand the abrasive nature of sintered ash. The systems are designed with features such as wear-resistant liners, robust pumps, and efficient filtration to ensure long-term performance. Regular maintenance and support services are also provided by HeadPowder to ensure that the systems operate at peak efficiency and longevity.
Conclusion: The Future of Sintered Ash Handling with Pneumatic Conveying
As industrial processes continue to evolve, the demand for efficient and safe bulk material handling solutions remains high. Pneumatic conveying technology, particularly in the context of sintered ash handling, offers a forward-thinking approach that addresses the challenges of traditional methods. With its ability to enhance operational efficiency, improve safety, and reduce costs, pneumatic conveying is set to play a crucial role in the future of industrial material transport. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing innovative and reliable solutions that meet the evolving needs of the industry.