

Working Principle and Features of Capsule Material Conveying System
HeadPowder, a leading manufacturer in the field of pharmaceutical and food processing equipment, specializes in the design and production of efficient capsule material conveying systems. This article aims to provide a detailed explanation of the working principle and key features of such systems, highlighting how they contribute to the smooth operation of production lines in pharmaceutical manufacturing facilities.
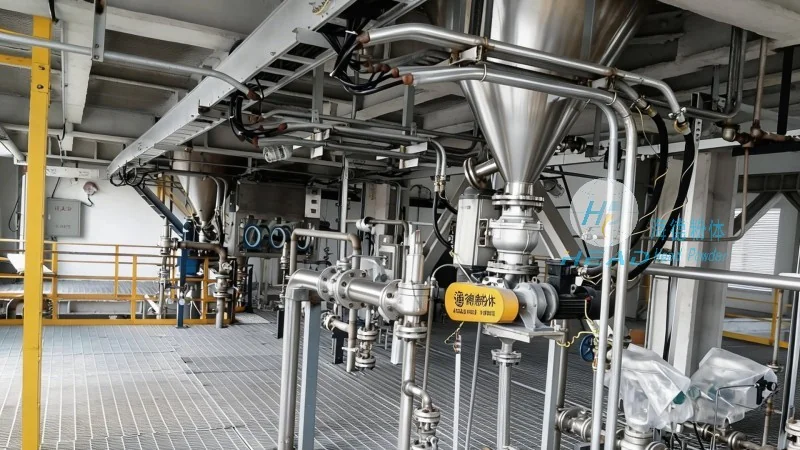
The capsule material conveying system is a critical component in the production process of capsules, ensuring that raw materials are transported from storage to processing units with precision and reliability. The core working principle revolves around the use of specialized machinery that can handle the delicate nature of capsule materials, such as gelatin or other polymers, while maintaining high throughput and minimal product damage. Typically, these systems employ mechanisms like screw conveyors, vibratory feeders, or pneumatic transport to move capsules through the production line. Each method is designed to address specific operational needs, such as handling different capsule sizes, maintaining consistent flow rates, and ensuring that the material remains in a controlled environment to prevent contamination or degradation.
One of the primary working principles is the utilization of mechanical motion to move capsules along a defined path. For instance, screw conveyors use rotating screws to push capsules forward, while vibratory conveyors utilize vibrations to create a cascading effect that propels the material. These mechanisms are often integrated with control systems that adjust speed and direction based on real-time production demands. The design of the conveying system also considers the physical properties of the capsule material, such as its density, shape, and moisture content, to optimize the conveying process and minimize energy consumption. By understanding these principles, manufacturers can select the most suitable conveying system for their specific production requirements, ensuring efficiency and cost-effectiveness.
Key Features of Capsule Material Conveying Systems
HeadPowder's capsule material conveying systems are engineered with several distinct features that enhance their performance and reliability. One of the most notable features is the high level of precision in material handling. The systems are designed to maintain consistent capsule flow rates, which is crucial for maintaining the quality and uniformity of the final product. This precision is achieved through advanced control technologies, including variable speed drives and feedback sensors, that monitor the conveying process and adjust parameters in real time. Additionally, the systems are constructed with materials that are resistant to corrosion and wear, ensuring long-term durability and minimal maintenance requirements.
Another key feature is the adaptability of the conveying system to different capsule types and sizes. Modern systems can handle a wide range of capsule dimensions, from small 2mm capsules to larger 00 size capsules, without the need for significant modifications. This flexibility is particularly valuable in pharmaceutical manufacturing, where product specifications may change frequently. The systems also incorporate features that prevent capsule breakage or deformation during transport, such as gentle handling mechanisms and cushioned surfaces. These features help maintain the integrity of the capsule material, which is essential for ensuring the quality of the final dosage form.
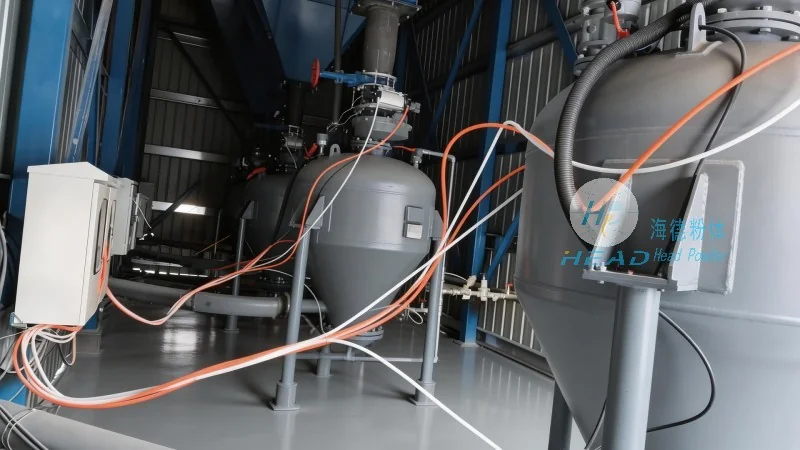
The systems also prioritize hygiene and compliance with industry standards. HeadPowder's equipment is constructed with stainless steel components and smooth surfaces that are easy to clean and sanitize, meeting the stringent requirements of GMP (Good Manufacturing Practice) regulations. The design minimizes dead zones and potential areas for material accumulation, reducing the risk of contamination. Furthermore, the systems are equipped with monitoring and alarm systems that alert operators to any deviations in the conveying process, ensuring immediate intervention and preventing production disruptions.
Conclusion and Company Information
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced capsule material conveying solutions. The company's expertise in mechanical engineering and pharmaceutical equipment design ensures that their systems are tailored to meet the unique needs of each client. By combining innovative technology with rigorous quality control, HeadPowder delivers conveying systems that enhance productivity, reduce operational costs, and maintain the highest standards of product quality. For pharmaceutical manufacturers seeking reliable and efficient capsule material handling solutions, HeadPowder's systems offer a proven solution that aligns with industry best practices and regulatory requirements.