

Working Principle and Features of Barley Material Handling Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the material handling industry, specializes in designing and manufacturing efficient systems for handling barley and other bulk materials. Based in Shandong, China, the company has built a reputation for delivering high-quality solutions tailored to the specific needs of the agricultural and food processing sectors. This article explores the working principle and key features of their barley material handling systems, providing a comprehensive overview for professionals in the field.
Understanding the Working Principle of Barley Material Handling Systems
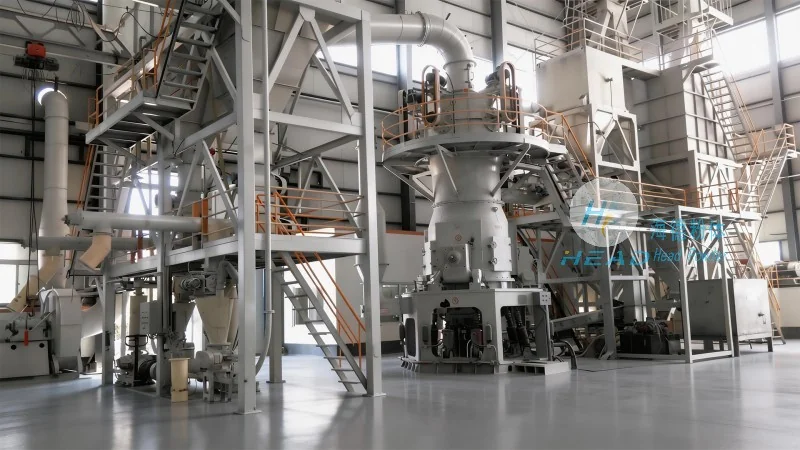
The barley material handling system developed by Shandong HeadPowder Engineering Co., Ltd. is engineered to streamline the entire process of receiving, storing, and transporting barley from the field to the processing plant. The system typically operates through a series of interconnected components, each designed to perform a specific function with precision and efficiency. At the core of the system is the intake mechanism, which may include a hopper or a receiving bin that collects raw barley from trucks or storage silos. This initial stage ensures a consistent flow of material into the processing line.
Once the barley is collected, it moves into the primary conveying section, often utilizing belt conveyors or screw conveyors to transport the grain horizontally or vertically. The choice of conveyor type depends on the distance and elevation changes required. For example, belt conveyors are ideal for long horizontal runs due to their high capacity and low maintenance, while vertical screw conveyors are effective for elevating barley to higher levels or transferring it between different floors of a facility. The system may also incorporate a series of transfer points and chutes to direct the flow of barley smoothly from one conveyor to another, minimizing the risk of spillage or blockages.
During the conveying process, the barley may undergo additional processing steps such as cleaning, screening, or sorting to remove impurities like dust, stones, or foreign materials. These operations are integrated into the system to ensure the final product meets quality standards. For instance, a vibrating screen or a magnetic separator might be employed to separate unwanted debris, while a dust extraction system helps maintain a clean and safe working environment. The system is designed to handle varying barley qualities and moisture levels, adapting to seasonal changes and different crop conditions.
Key Features of the Barley Material Handling System
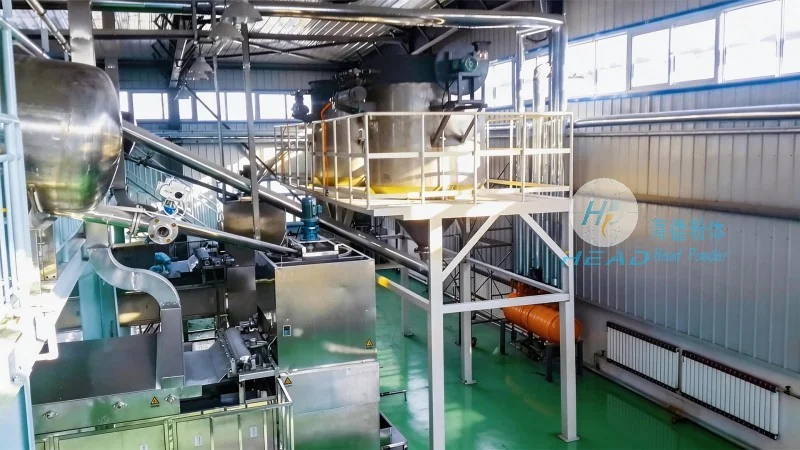
Shandong HeadPowder Engineering Co., Ltd.'s barley material handling system is distinguished by several key features that enhance its performance and reliability. One of the primary advantages is its modular design, which allows for easy customization and expansion. Users can add or remove components based on their specific requirements, such as increasing the capacity of the conveyor or adding additional cleaning stages. This flexibility makes the system suitable for both small-scale farms and large industrial processing facilities.
Another notable feature is the system's high efficiency and low energy consumption. Advanced engineering techniques, such as optimized belt tension and variable speed drives, reduce energy usage while maintaining high throughput. The use of durable materials, including stainless steel and high-strength plastics, ensures long-term durability and resistance to corrosion, even in humid or dusty environments common in agricultural settings. This durability minimizes maintenance costs and downtime, contributing to overall operational efficiency.
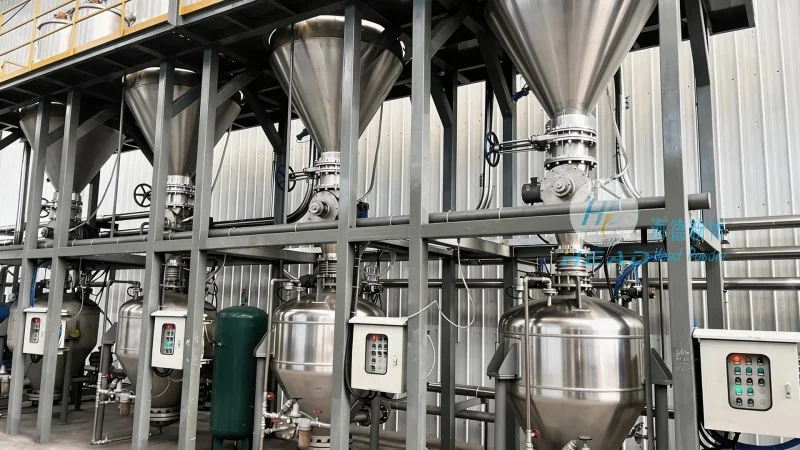
The system also prioritizes safety and operational reliability. It incorporates safety sensors and emergency stop buttons to prevent accidents during operation. Additionally, the design includes features like overload protection and automatic shut-off mechanisms to protect the equipment from damage caused by excessive material flow or blockages. These safety measures align with industry standards and ensure a secure working environment for operators.
Furthermore, the system is equipped with user-friendly control panels and monitoring systems. Operators can easily adjust conveyor speeds, monitor material levels, and receive alerts for any issues through a digital interface. This integration of technology allows for real-time management of the handling process, enabling quick responses to changes in production demands or material quality. The system's adaptability to different barley varieties and processing requirements makes it a versatile solution for various applications, from storage and transport to pre-processing for milling or brewing.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s barley material handling system exemplifies the company's commitment to innovation and quality in the material handling industry. By combining advanced engineering with practical design, the system offers an efficient, reliable, and adaptable solution for handling barley and other bulk materials. Its modular structure, energy-efficient operation, and emphasis on safety make it an ideal choice for businesses seeking to optimize their processing operations. With a strong presence in Shandong, China, the company continues to provide tailored solutions that meet the evolving needs of the agricultural and food processing sectors.