

Working Principle and Features of Sodium Carbonate Powder Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for the efficient handling of sodium carbonate powder through pneumatic conveying systems. This article explores the fundamental working principles and key features of such equipment, highlighting how it enhances material transport in industrial applications.
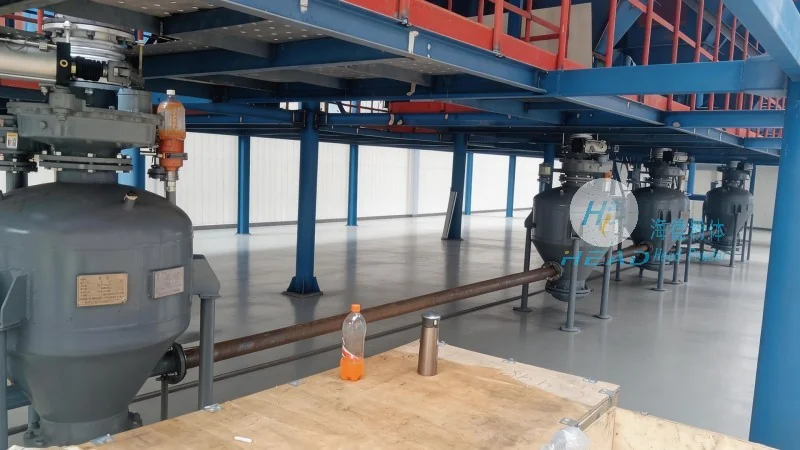
Working Principle of Pneumatic Conveying Systems for Sodium Carbonate
The core mechanism of pneumatic conveying equipment involves the use of air or gas to transport dry powder materials like sodium carbonate. The process typically operates under pressure or vacuum, depending on the system design. In a typical positive pressure system, compressed air is introduced into a hopper or storage silo, creating a pressure differential that propels the powder into a pipeline. The equipment comprises several critical components, including a feeding mechanism, a conveying line, a separation unit, and a discharge system. The feeding device ensures a consistent flow of sodium carbonate powder into the pipeline, while the conveying line transports the material to the destination. The separation unit, often a cyclone or filter, separates the powder from the air stream, allowing the powder to be collected and the air to be recycled or discharged. This closed-loop system minimizes material loss and ensures efficient operation.
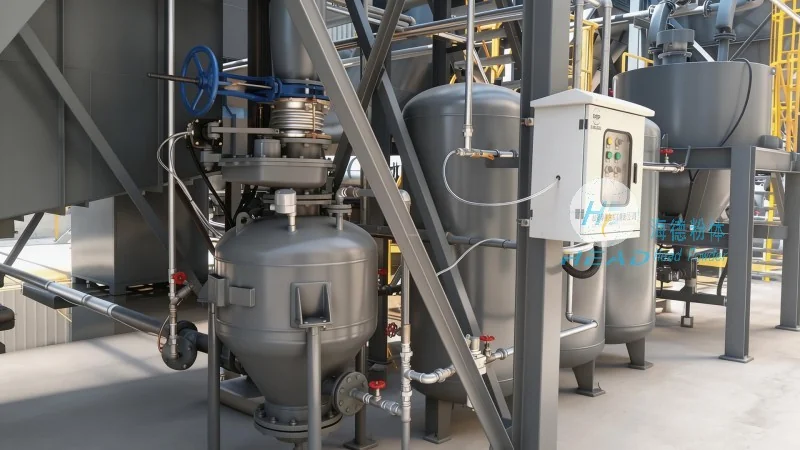
Key Features of Sodium Carbonate Powder Pneumatic Conveying Equipment
HeadPowder's pneumatic conveying systems for sodium carbonate powder are designed with several distinctive features that enhance performance and reliability. One of the primary advantages is the ability to handle fine or cohesive powders without the need for mechanical components that could cause blockages or wear. The equipment is constructed from corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of sodium carbonate and prevent degradation over time. Additionally, the system offers flexibility in terms of conveying distance and capacity, making it suitable for various industrial settings. The automated control systems provide real-time monitoring of pressure, flow rate, and material levels, ensuring optimal operation and reducing downtime. Another notable feature is the energy efficiency of the system, as it minimizes the use of external power compared to traditional mechanical conveying methods. The equipment also complies with international safety and environmental standards, ensuring safe operation in industrial environments.
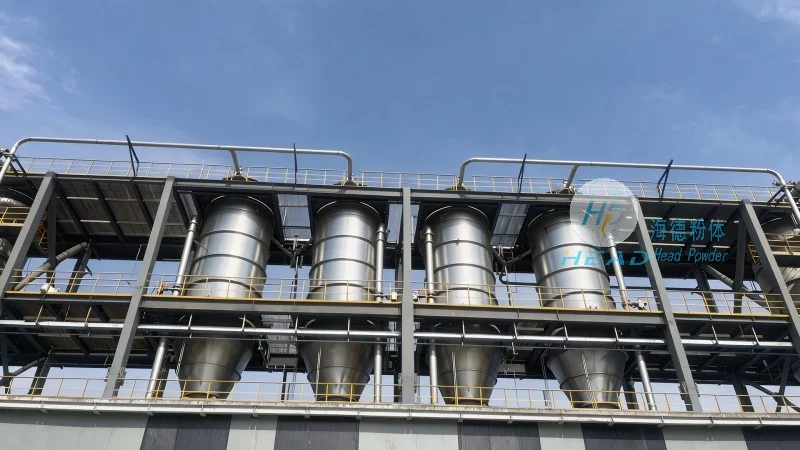
Application Benefits and Industrial Impact
The implementation of pneumatic conveying equipment for sodium carbonate powder offers significant benefits to industrial processes. By eliminating the need for manual handling or mechanical conveyors, the system reduces labor costs and improves workplace safety. The consistent and controlled flow of powder minimizes material degradation and loss, leading to higher product quality and reduced waste. The compact design of the equipment allows for easy integration into existing production lines, without requiring extensive modifications to the facility. Furthermore, the system's ability to handle large volumes of material efficiently supports increased production throughput, contributing to overall operational efficiency. In industries such as chemical manufacturing, food processing, and pharmaceuticals, where sodium carbonate is commonly used as a raw material, the pneumatic conveying system enhances the reliability and scalability of material handling operations.
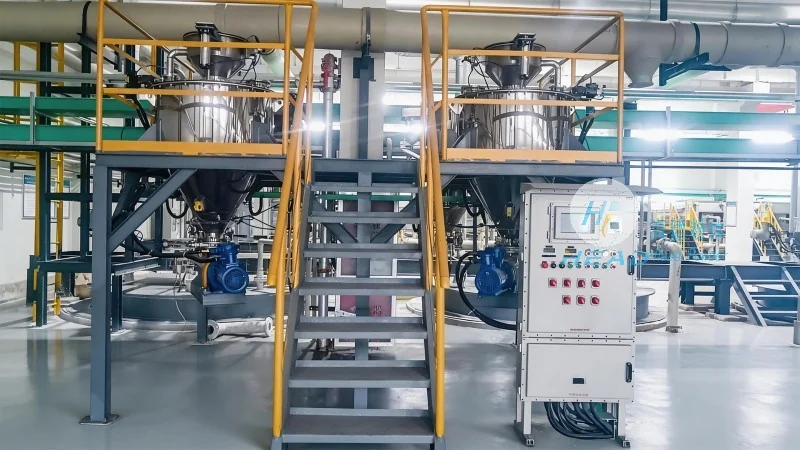
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a trusted provider of advanced pneumatic conveying solutions for sodium carbonate powder. With a focus on innovation and quality, the company has developed equipment that combines efficiency, reliability, and safety. The working principles and features discussed above demonstrate the effectiveness of pneumatic conveying systems in optimizing material transport for sodium carbonate applications. By leveraging the expertise of HeadPowder, industrial facilities can enhance their operational performance, reduce costs, and improve overall productivity. The company's commitment to customer satisfaction and technological advancement ensures that clients receive tailored solutions that meet their specific needs in the handling of sodium carbonate powder.