

Principle and Working Scene Characteristics of Purified Ash Pneumatic Conveying Systems
For industrial applications that require efficient and reliable material handling, the purified ash pneumatic conveying system stands out as a critical solution. This system is designed to handle ash and similar particulate materials with precision, ensuring minimal contamination and optimal performance across various operational environments.
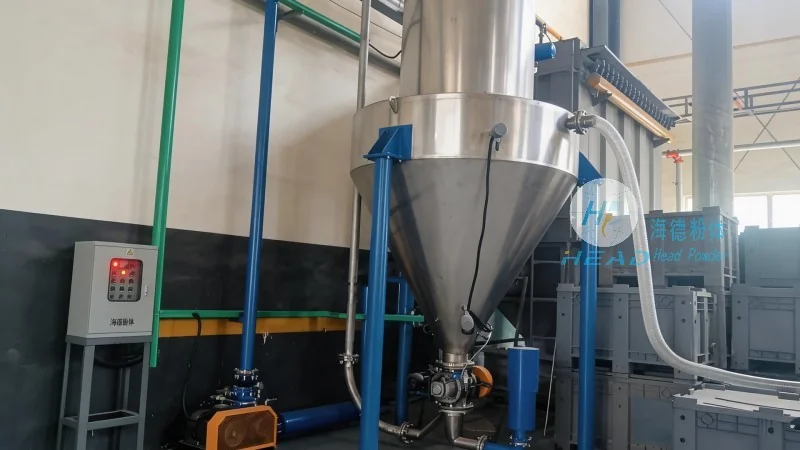
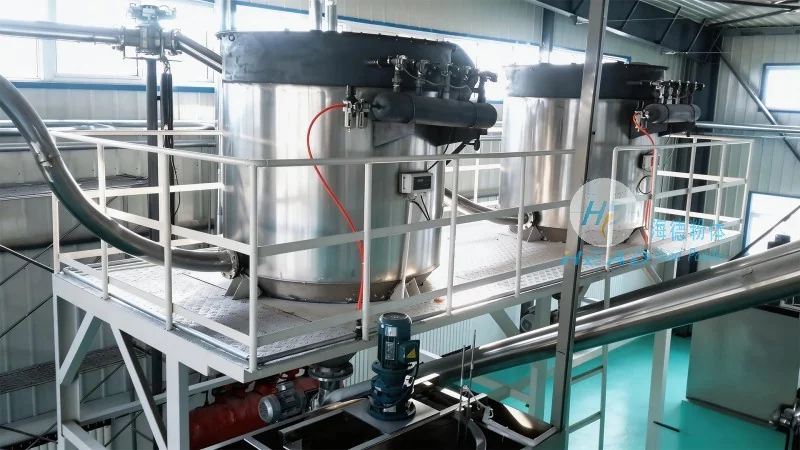
Principle of the Purified Ash Pneumatic Conveying System
The core of the purified ash pneumatic conveying system lies in its air-based transport mechanism. By utilizing compressed air or other gas streams, the system draws ash particles from a source and transports them to a designated destination. The process involves several key components, including a hopper for material storage, a rotary valve for controlled discharge, and a conveying line equipped with filters and pressure regulators. These components work in tandem to maintain consistent airflow and particle flow, preventing blockages and ensuring smooth operation. The system’s design emphasizes filtration to remove dust and impurities from the air stream, which is crucial for maintaining air quality and protecting downstream equipment.
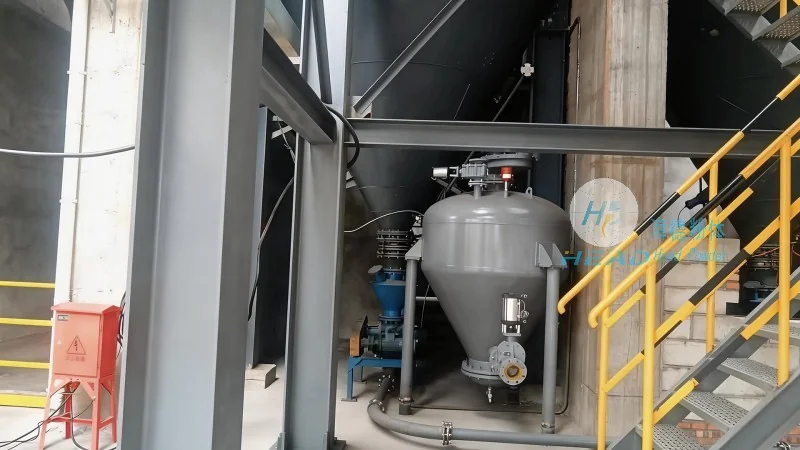
Working Scene Characteristics and Application Scenarios
The purified ash pneumatic conveying system is particularly suited for industrial settings where ash or similar fine particulates need to be moved over short to medium distances. Common applications include power plants, waste incineration facilities, and industrial processing plants. In these environments, the system’s ability to handle high volumes of material with low maintenance requirements makes it an ideal choice. The system operates efficiently in both indoor and outdoor settings, adapting to various environmental conditions. Its compact design allows for installation in confined spaces, while its robust construction ensures durability under heavy operational loads. The system’s flexibility in conveying different ash types, such as fly ash or bottom ash, further enhances its applicability across diverse industrial sectors.
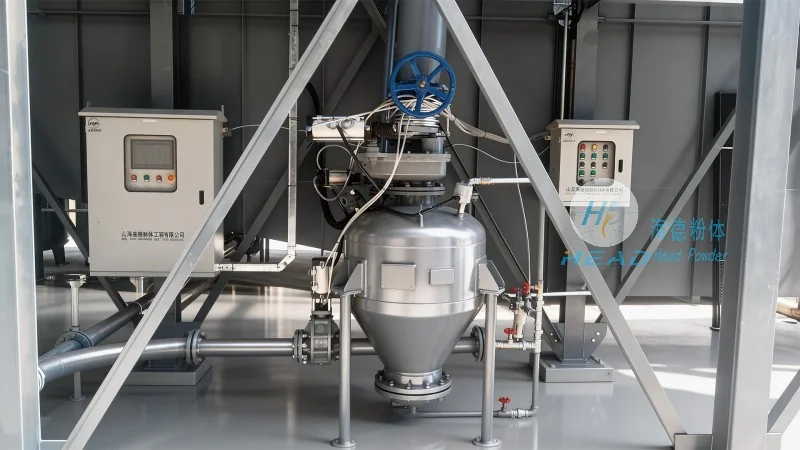
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of industrial clients. Headpowder’s expertise in ash handling technology has enabled the development of the purified ash pneumatic conveying system, which combines efficiency, reliability, and environmental compliance. The company’s commitment to customer satisfaction and technical excellence is reflected in its comprehensive support services, including installation, maintenance, and technical assistance. Headpowder’s operations are based in Shandong, China, where the company leverages local resources and expertise to deliver high-quality products and solutions to global markets.