

Principle and Working Scene Characteristics of Coffee Powder Pneumatic Conveying Equipment
For coffee processing facilities, the efficient and hygienic handling of coffee powder is crucial to maintaining product quality and operational efficiency. Pneumatic conveying systems offer a reliable solution for transporting coffee powder from storage silos to processing lines, packaging areas, or other destinations within a facility. These systems utilize air to move the powder through a network of pipes, eliminating the need for mechanical components that can introduce contamination or wear over time.
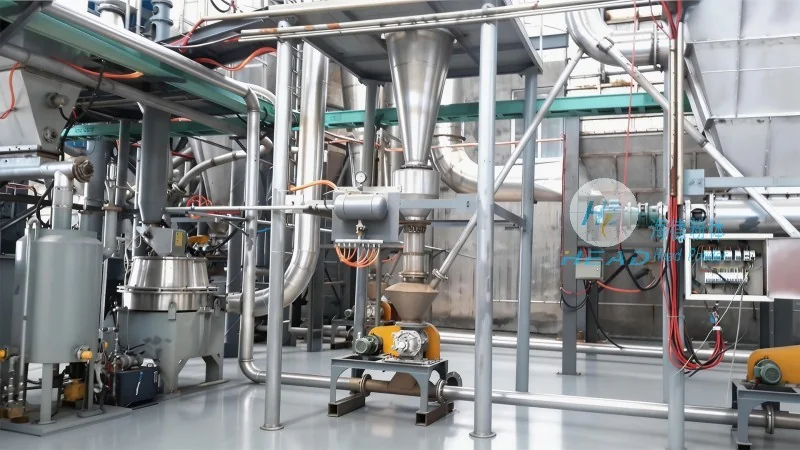
Company Overview: HeadPowder
HeadPowder, a leading manufacturer of pneumatic conveying equipment, specializes in designing and supplying customized solutions for the coffee industry. With a strong presence in Shandong, China, HeadPowder combines advanced engineering with industry expertise to deliver high-performance coffee powder handling systems. The company’s commitment to quality and customer satisfaction has established it as a trusted partner for coffee processing businesses worldwide.
Principle of Pneumatic Conveying for Coffee Powder
The core principle of coffee powder pneumatic conveying involves the use of air as a medium to transport solid particles. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems generate air pressure inside the conveying line, pushing the coffee powder forward through the pipes. Negative pressure systems, on the other hand, create a vacuum in the line, drawing the powder from the source. Both methods are effective for coffee powder, but the choice depends on factors such as the distance to be covered, the volume of material, and the desired level of control over the conveying process.
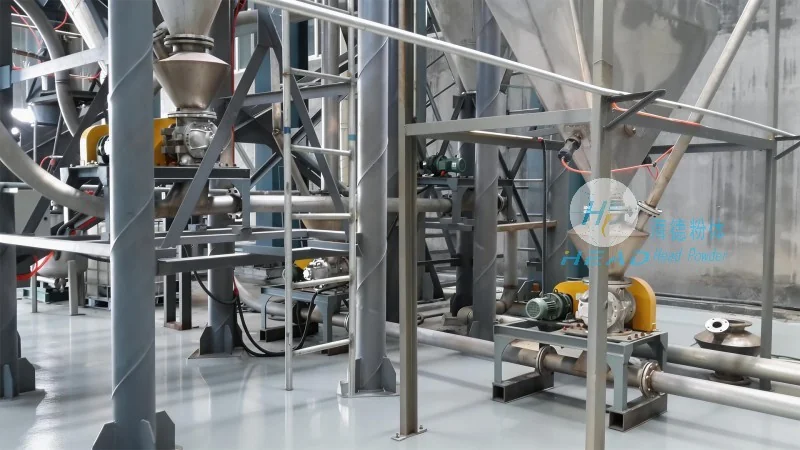
Key Components of Coffee Powder Pneumatic Conveying Systems
A typical coffee powder pneumatic conveying system consists of several key components, each playing a critical role in the overall operation. These include a hopper or silo for storing the coffee powder, a feeder to control the flow rate, a blower or vacuum pump to generate the air pressure, a conveying line network, and a receiver or collection tank at the destination. The hopper is designed to maintain the powder’s flowability and prevent bridging, while the feeder ensures a consistent and controlled discharge of the material. The blower or pump provides the necessary air volume and pressure to move the coffee powder through the pipes. The conveying line is typically made of stainless steel or other food-grade materials to ensure hygiene and durability. The receiver collects the coffee powder at the end of the line, often equipped with a dust collection system to prevent airborne particles from escaping.
Working Scene Characteristics of Coffee Powder Pneumatic Conveying Equipment
The application of coffee powder pneumatic conveying equipment varies across different working scenes, each with unique requirements and challenges. In coffee processing plants, these systems are commonly used to transport freshly ground coffee from the roasting and grinding stages to the packaging line. The equipment must handle the fine particles of coffee powder without causing blockages or excessive pressure drops in the pipes. In coffee roasting facilities, the system may need to handle hot coffee beans or ground coffee, requiring temperature-resistant components to prevent damage or degradation of the product. For coffee roasters and manufacturers, the ability to maintain product integrity and prevent contamination is paramount, making pneumatic conveying an ideal choice.
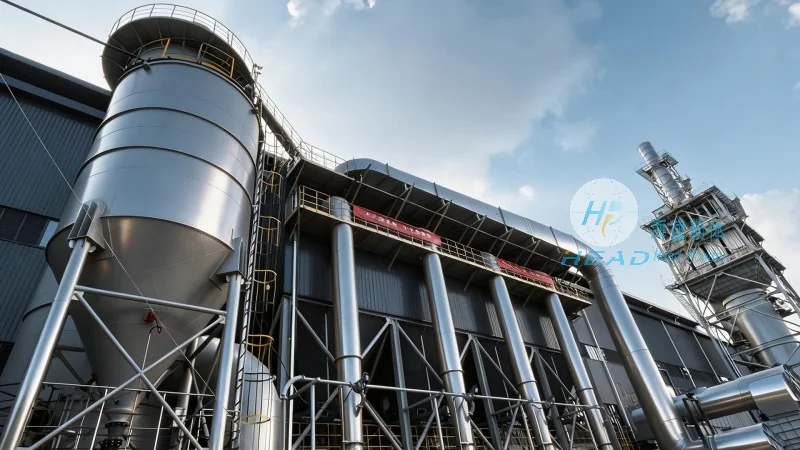
Advantages of Coffee Powder Pneumatic Conveying Systems
Compared to traditional mechanical conveying methods, coffee powder pneumatic conveying offers several advantages that make it a preferred choice for many coffee processing businesses. One of the key benefits is the elimination of direct contact between the coffee powder and mechanical components, reducing the risk of contamination from metal particles or other foreign materials. This is particularly important for coffee products that require strict hygiene standards, such as specialty or organic coffees. Another advantage is the ability to handle fine and abrasive materials without causing excessive wear on the equipment. Coffee powder is a fine, abrasive substance that can quickly damage mechanical conveyors, but pneumatic systems are designed to withstand this type of material, resulting in lower maintenance costs and longer equipment life. Additionally, pneumatic conveying systems can be easily integrated into existing production lines, allowing for flexible and scalable operations. They can be adjusted to handle varying volumes of coffee powder, making them suitable for both small-scale roasting operations and large-scale coffee processing facilities.
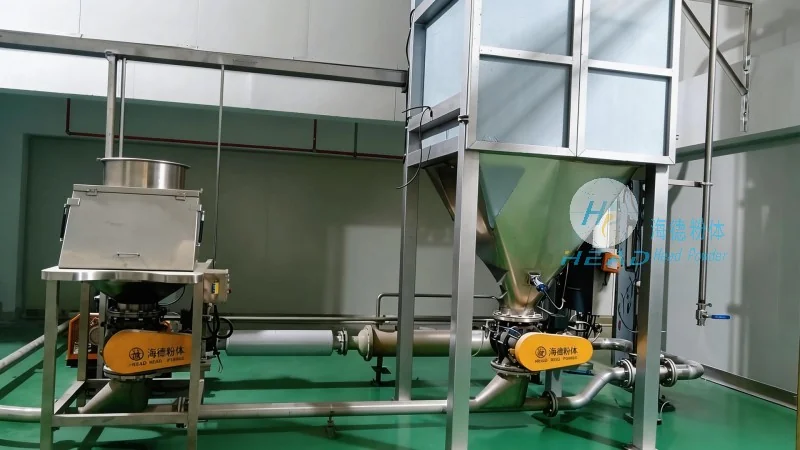
Customization and Application Flexibility
HeadPowder understands that each coffee processing facility has unique operational needs and space constraints. Therefore, the company offers customized pneumatic conveying solutions tailored to specific requirements. Whether the application involves short-distance transport within a small roasting shop or long-distance transfer between multiple processing sites, HeadPowder can design a system that meets the exact specifications. The company’s engineers work closely with clients to assess their current processes, identify potential bottlenecks, and recommend the most efficient and cost-effective conveying solution. Customization options include different pipe diameters, material types, and control systems to ensure optimal performance and integration with existing equipment. This flexibility allows coffee processing businesses to optimize their operations and improve overall productivity.
Conclusion: The Role of Pneumatic Conveying in Coffee Processing
As the coffee industry continues to grow and evolve, the demand for efficient and hygienic handling of coffee powder remains high. Pneumatic conveying equipment, particularly from manufacturers like HeadPowder, plays a critical role in meeting these demands. By leveraging the principles of air-based transport, these systems provide reliable, clean, and efficient solutions for coffee powder handling. The working scene characteristics of these systems, combined with their advantages in hygiene, durability, and flexibility, make them an essential component of modern coffee processing facilities. For coffee roasters, manufacturers, and distributors, investing in a high-quality pneumatic conveying system from HeadPowder is a strategic decision that can enhance operational efficiency, maintain product quality, and support long-term business growth.