

Principle and Working Scene Characteristics of Beer Brewery Pellet Conveying Systems
For breweries, the efficient handling of spent grain (brewery pellet) is a critical operational challenge. The beer brewery pellet conveying system, developed by Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder), addresses this challenge through advanced technology and tailored solutions. This article explores the core principles of the system and its application scenarios, highlighting how it enhances productivity and operational efficiency in modern brewing facilities.
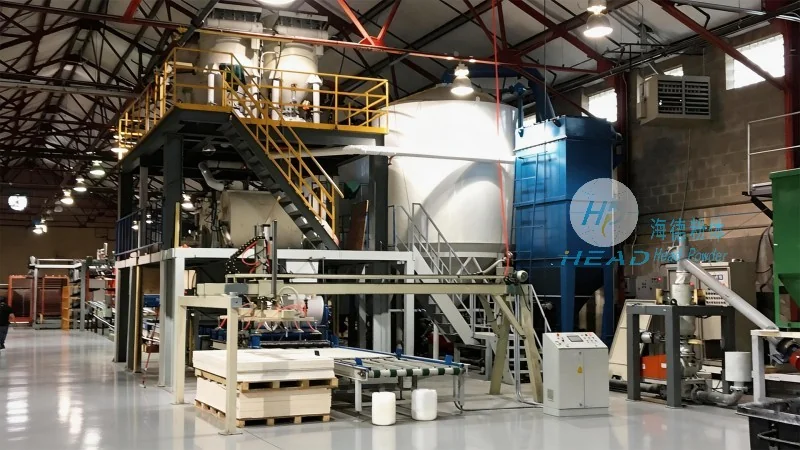
Core Principles of the Beer Brewery Pellet Conveying System
The system operates on the principle of pneumatic conveying, a method that uses air pressure to transport bulk materials like spent grain. HeadPowder's design incorporates several key components to ensure reliable and efficient operation. The system typically includes a hopper for material storage, a rotary valve for controlled discharge, a conveying line with appropriate air flow management, and a receiver for material deposition. The pneumatic conveying process minimizes material degradation and reduces the risk of contamination, which is essential for maintaining product quality in the brewing process.
One of the fundamental advantages of this system is its ability to handle abrasive and high-volume materials. The design of the conveying line, including the selection of appropriate ductwork and air velocity, ensures that the material is transported without excessive wear or blockages. Additionally, the system incorporates features such as pressure relief valves and air filtration to maintain system integrity and environmental compliance. The control system, often integrated with the brewery's existing automation infrastructure, allows for real-time monitoring and adjustment of conveying parameters, optimizing performance based on production needs.
Working Scene Characteristics and Application Scenarios
The beer brewery pellet conveying system is designed to meet the diverse needs of modern breweries, from small-scale craft breweries to large industrial facilities. Its adaptability is evident in various operational scenarios, including:
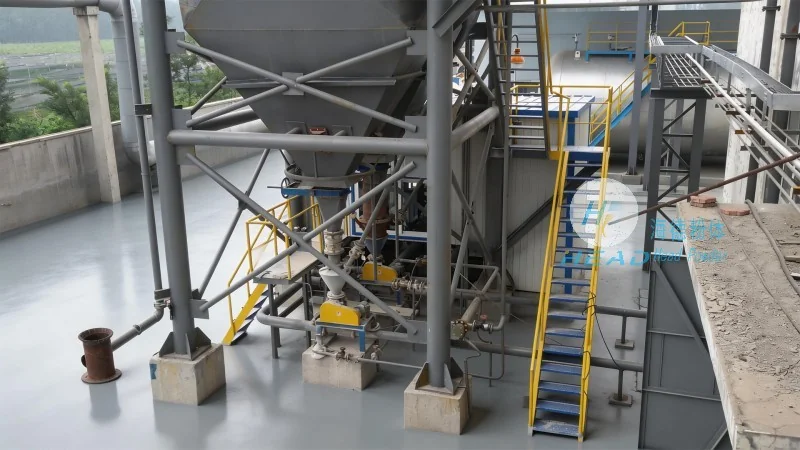
1. On-site Storage and Transfer In many breweries, spent grain is collected and stored on-site before being transported to processing facilities. The conveying system facilitates the transfer of this material from storage silos or bins to the processing line, reducing manual handling and associated labor costs. The system's ability to handle high volumes and maintain material integrity ensures that the spent grain is ready for further processing, such as animal feed production or biofuel generation.
2. Integrated Processing Lines For breweries that incorporate spent grain into their own production processes, the conveying system is integrated into the processing line. This includes applications like using spent grain as a raw material for brewing supplements or as a component in the production of other food products. The system's precision and reliability ensure that the material is delivered to the processing equipment at the correct temperature and moisture level, optimizing the subsequent steps in the production cycle.
3. Waste Management and Environmental Compliance In today's environmentally conscious industry, the efficient management of brewery waste is paramount. The conveying system plays a crucial role in waste management by ensuring that spent grain is transported to designated disposal or recycling facilities in a controlled manner. The system's design minimizes dust emissions and noise pollution, contributing to a safer and more sustainable operational environment. This is particularly important for breweries operating in urban or residential areas, where compliance with environmental regulations is a top priority.
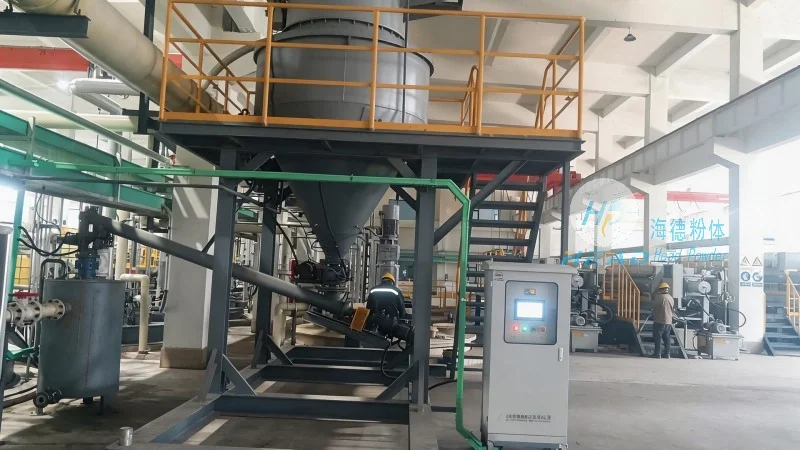
4. Scalability and Customization HeadPowder understands that each brewery has unique operational requirements. The conveying system is designed to be scalable, allowing for adjustments in capacity and configuration to match the specific needs of the facility. Whether a brewery is expanding its production capacity or upgrading its existing equipment, the system can be customized to meet these changes. This flexibility ensures that the system remains a valuable asset as the brewery grows and evolves over time.
Benefits and Advantages for Brewery Operations
Implementing the beer brewery pellet conveying system from HeadPowder offers numerous benefits that directly impact the bottom line and operational efficiency of a brewery. These include:
Increased Productivity By automating the material handling process, the system reduces downtime and labor costs associated with manual transfer. The efficient conveying of spent grain allows for faster processing and higher throughput, enabling breweries to meet increasing demand without additional labor.
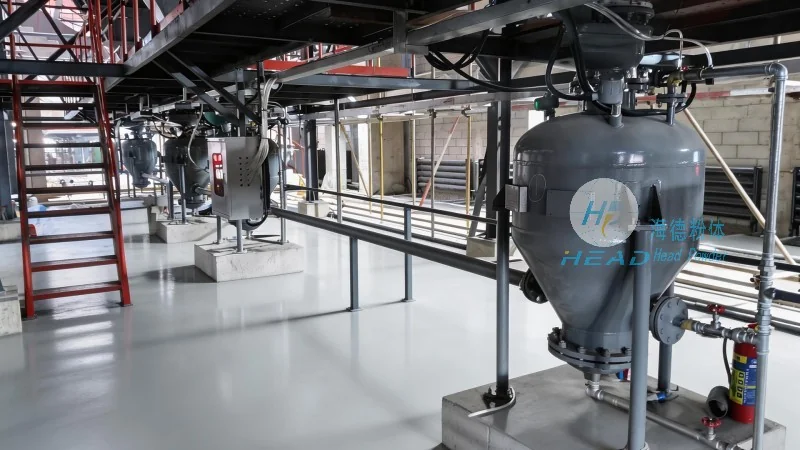
Improved Material Quality The pneumatic conveying method minimizes material degradation, ensuring that the spent grain remains in optimal condition for its intended use. This is particularly important for breweries that use spent grain in their own products or for external markets, as it maintains the quality and value of the material.
Enhanced Safety and Hygiene The system's enclosed design reduces the risk of dust exposure and cross-contamination, creating a safer working environment for employees. Additionally, the system's integration with the brewery's cleaning and sanitation protocols ensures that the material handling process adheres to strict hygiene standards, which is critical for maintaining product safety and regulatory compliance.
Cost Savings and Sustainability By optimizing material handling and reducing waste, the system contributes to long-term cost savings. The efficient use of energy and resources also aligns with the growing trend of sustainable brewing practices. HeadPowder's commitment to energy-efficient design further enhances the system's environmental impact, making it a responsible choice for modern breweries.